How Paper Grade Affects Cutting Performance | Practical Guide

Not all paper behaves the same in a sheeter.
Running different grades with one fixed setup is one of the most common reasons for defects, unstable operation, and unnecessary downtime.

In real production, cutting performance is closely tied to the physical properties of the paper—weight, stiffness, surface structure, and moisture behavior all play a role. Ignoring these differences leads to inconsistent results.

Why Paper Grade Matters

Each paper grade responds differently to tension, cutting force, and transport conditions.

A setup that works well for one material may cause problems for another.
This is why parameter adjustment is not optional—it is necessary for stable production.

Typical Behavior by Paper Type
1. Lightweight Paper (28–80 gsm)
Thin paper is flexible and highly sensitive to tension changes.

Common issues include:

  • wrinkling during transport
  • web instability at higher speeds
  • risk of web breaks under excessive tension

To run lightweight grades properly, the system must operate under low, stable tension, with smooth conveying and minimal disturbance.
2. Heavy Board and High GSM Paper
Thicker materials behave very differently.

They require:

  • higher and more stable cutting force
  • rigid mechanical support during cutting
  • precise synchronization to avoid deformation

If the cutting force is insufficient or unstable, problems such as rough edges or incomplete cuts can occur.
3. Coated Paper
Coated surfaces introduce another layer of complexity.

While structurally stable, they are more sensitive to surface damage.

Typical risks include:

  • scratching during transport
  • coating cracks at the cut edge
  • visi

Why High-Speed Lines Still Generate Waste | Practical Insight

Many plant owners assume that increasing machine speed will directly increase output.
In practice, this is often not the case.

A line running faster does not automatically produce more saleable product.
If the system is not properly balanced, higher speed usually leads to more instability—and more waste.

The Real Problem: Lack of Synchronization

In most cases, waste at high speed is not caused by the cutting unit itself.
It comes from poor coordination between different sections of the line.

A typical converting line includes:

  • cutting
  • conveying
  • stacking
  • packing

If these parts are not synchronized, problems appear quickly.

For example:

  • sheets leave the cutter faster than the conveyor can handle
  • conveying speed does not match stacking rhythm
  • stacking cannot stabilize sheets before the next batch arrives

The result is predictable: misalignment, wrinkling, sheet overlap, or jams.

All of these become waste.

Why Speed Amplifies Small Problems

At lower speeds, minor issues are often manageable.
Operators can make adjustments, and the system has more tolerance.

At higher speeds, the situation changes.

Small deviations—such as slight timing differences or uneven sheet flow—are magnified.
What was once a minor fluctuation becomes a visible defect or a stop.

This is why some lines perform well at medium speed but struggle when pushed closer to their rated capacity.

Where Waste Typically Comes From

In high-speed production, waste is usually generated in three areas:

1. Transfer Between Sections
If sheet flow is not smooth between cutting and conveying, alignment is lost.

2. Stacking Stability
If sheets are not properly controlled during stacking, they shift, overlap, or become uneven.

3. Process Timing Mismatch
If one unit runs faster or slower than the others, the entire flow becomes unstable.

None of these are caused by speed alone.
They are caused by lack of coordination.

What a Balanced Line Looks Like

A stable high-speed line is not defined by how fast one machine runs, but by how well all sections work together.

In a properly configured system:

  • cutting speed matches conveying capacity
  • conveying speed matches stacking rhythm
  • stacking output matches packing capability

Each part supports the next, without forcing it.

This is what allows the line to run fast without increasing waste.

Conclusion

Higher speed does not guarantee higher efficiency.
Without synchronization, it often does the opposite.

Real efficiency comes from balance—where every part of the line operates in coordination.
Only then can higher speed translate into higher output, rather than higher loss.

SHM A4-5 & A4B Line Installed in Tanzania

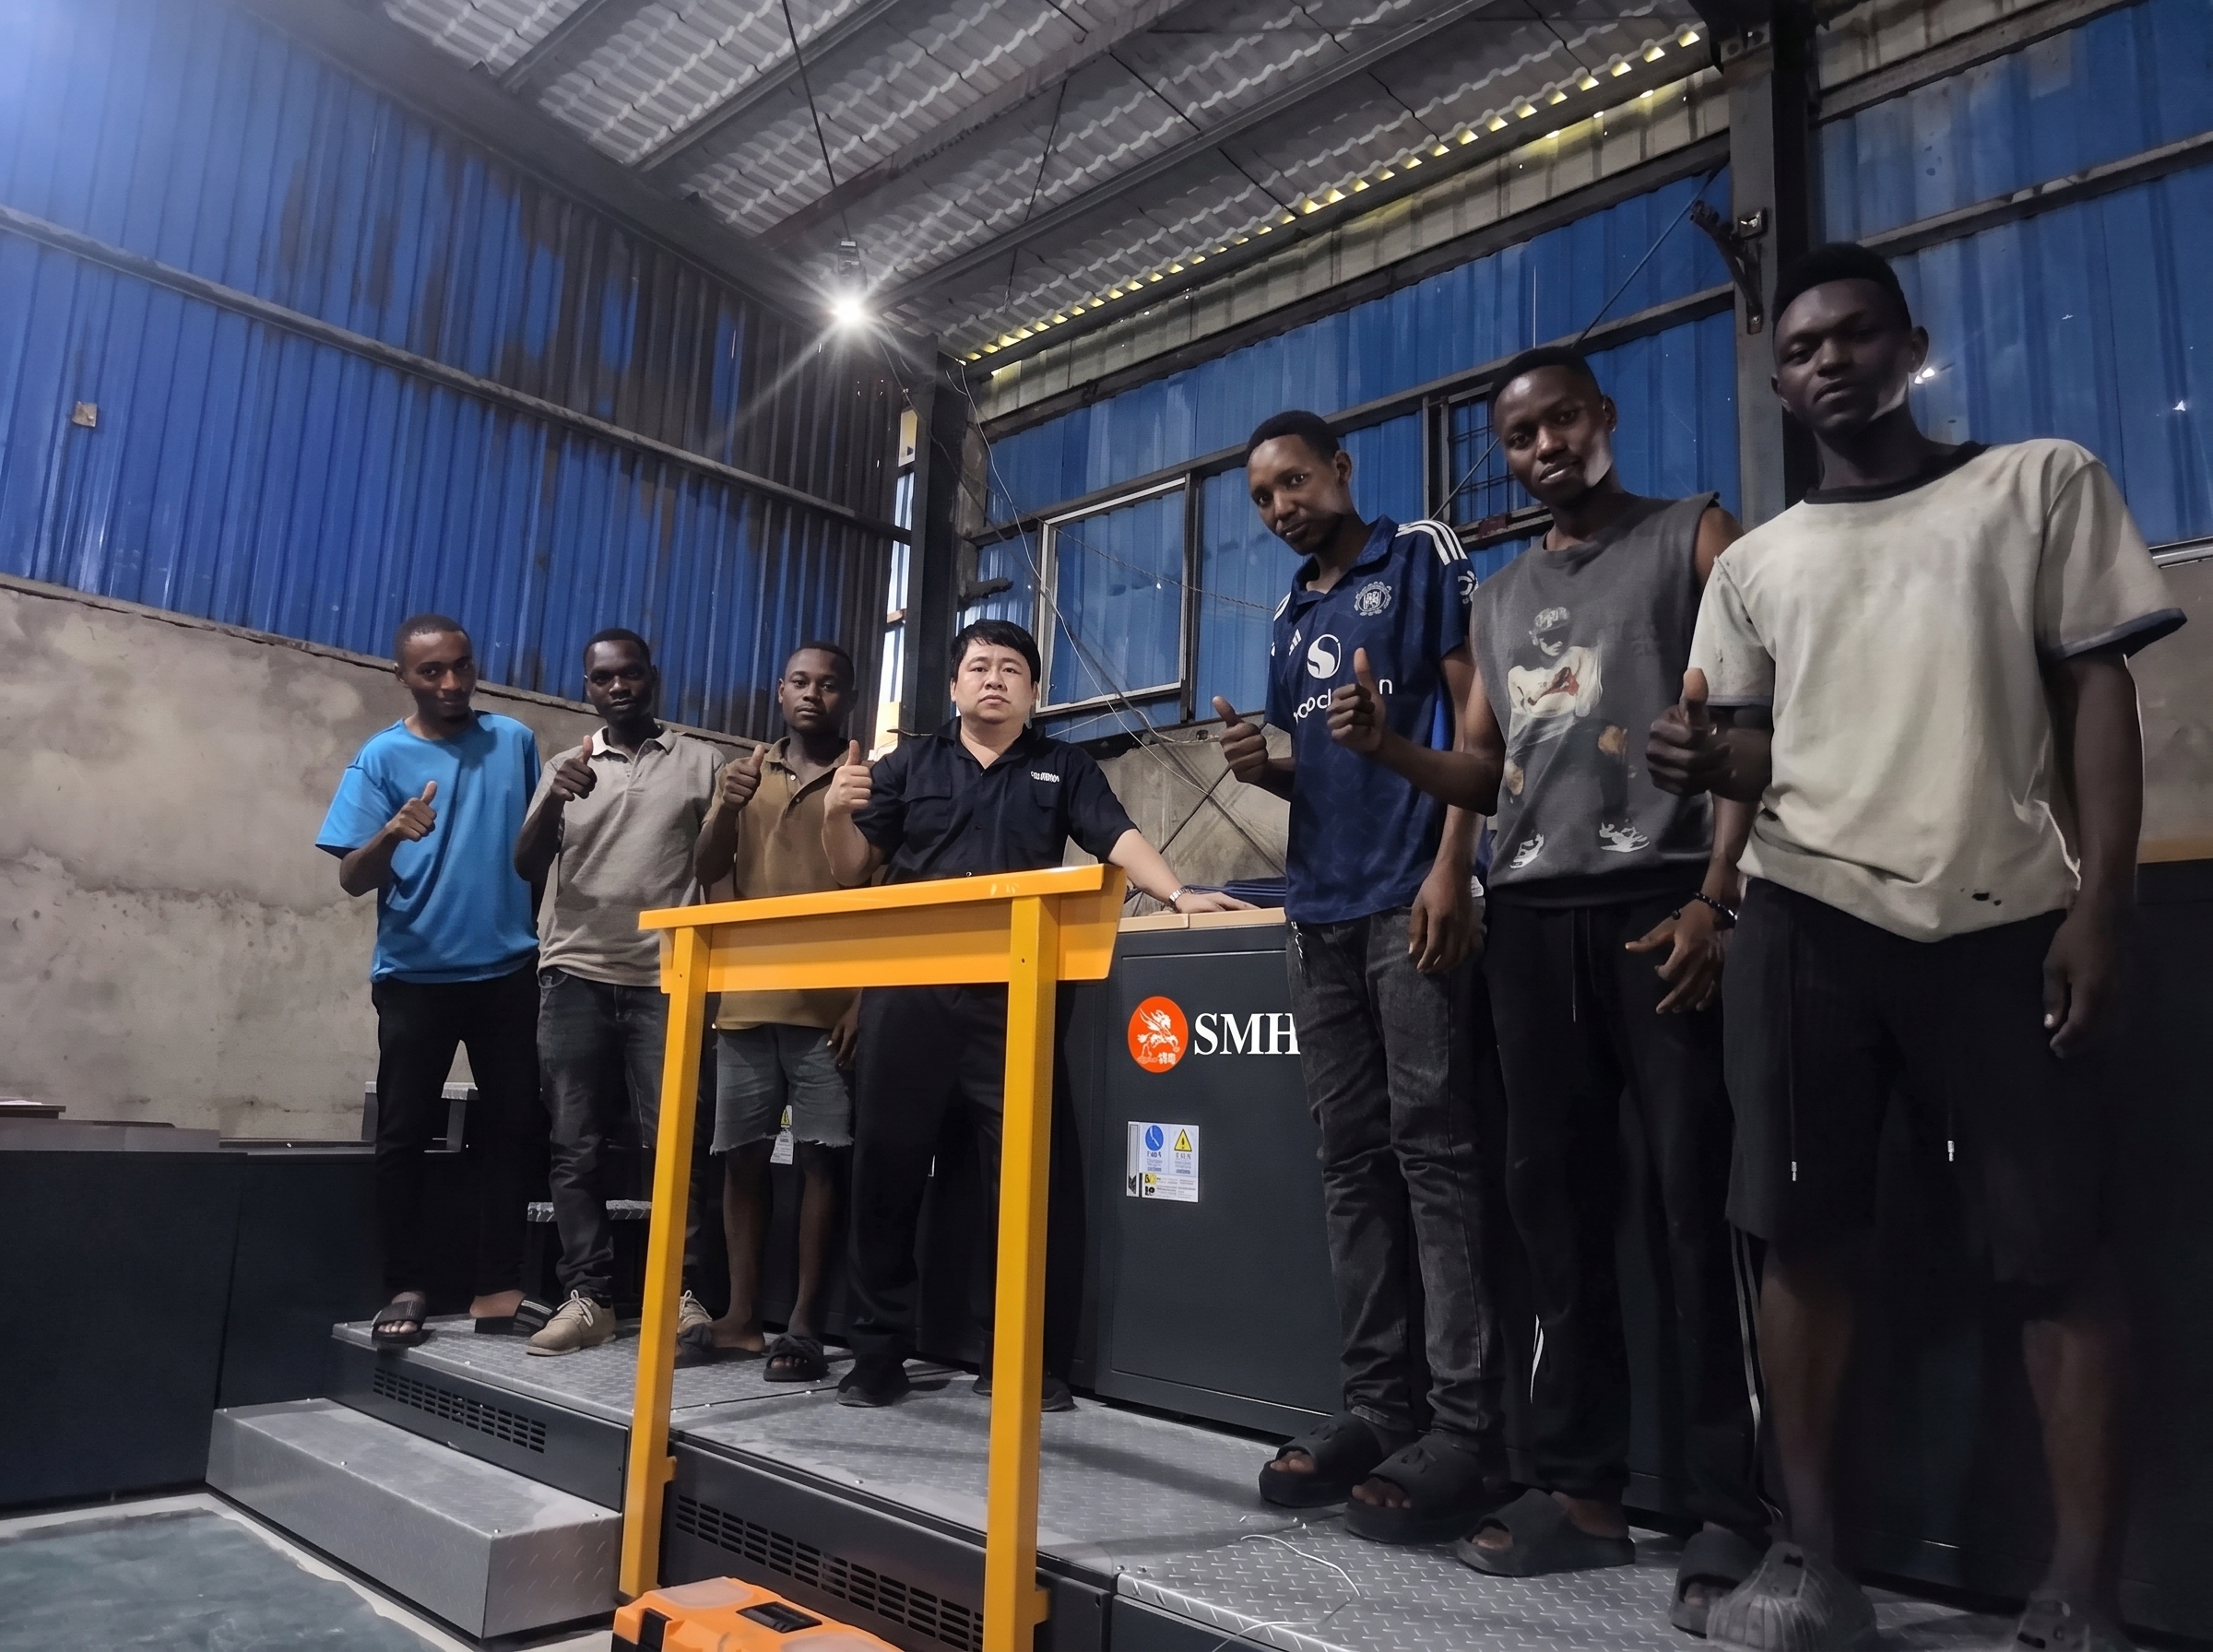
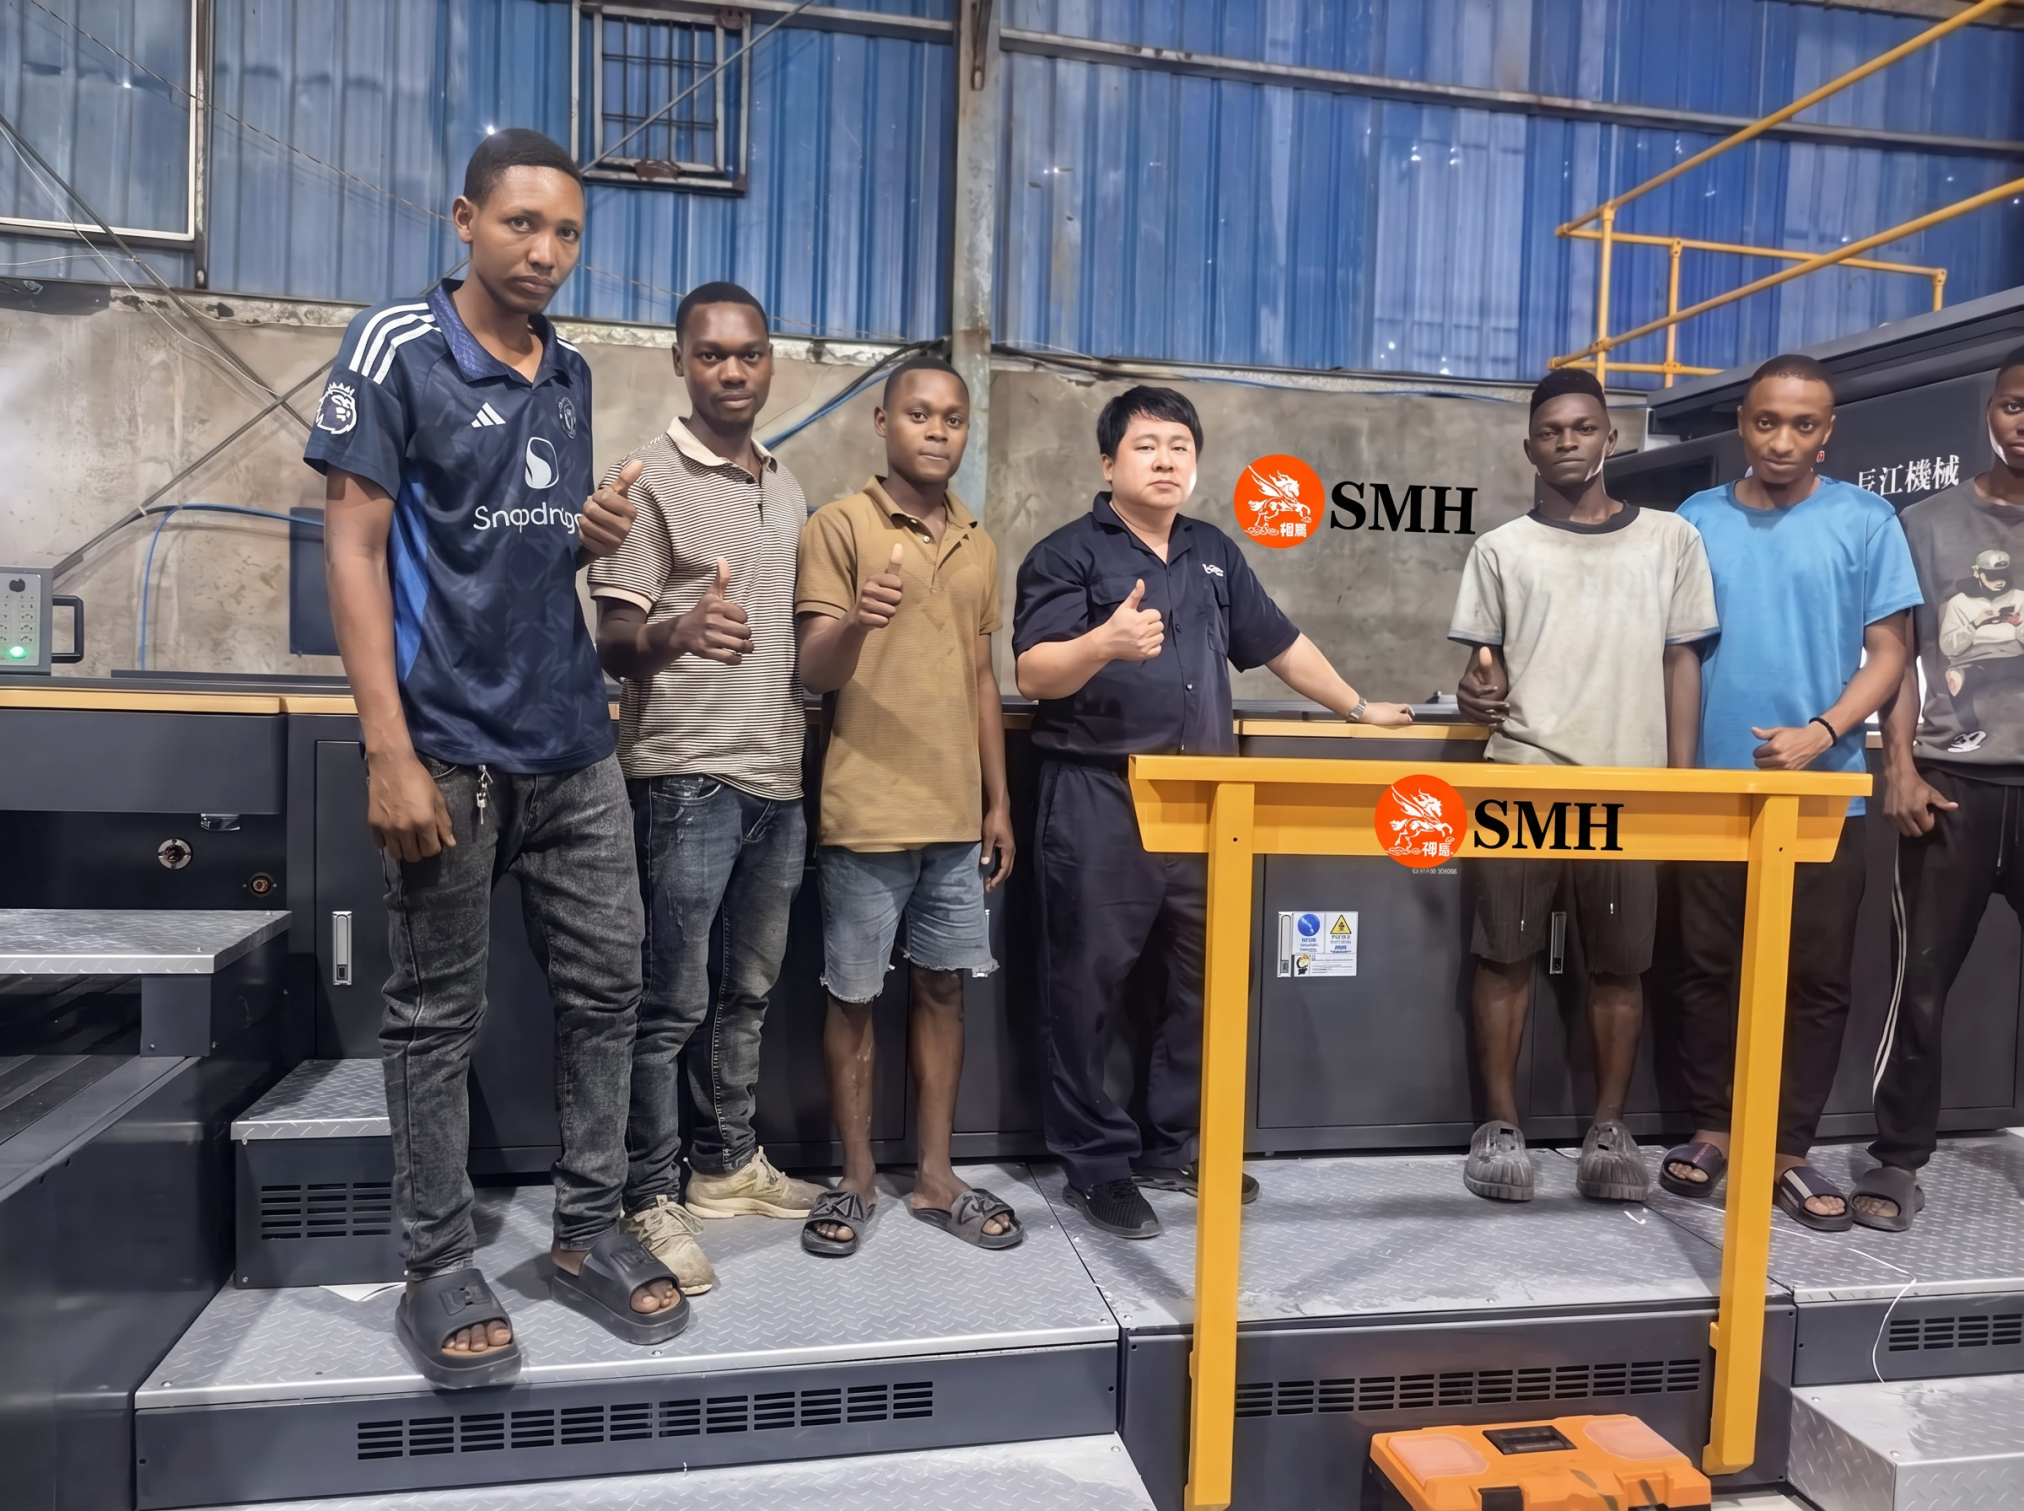
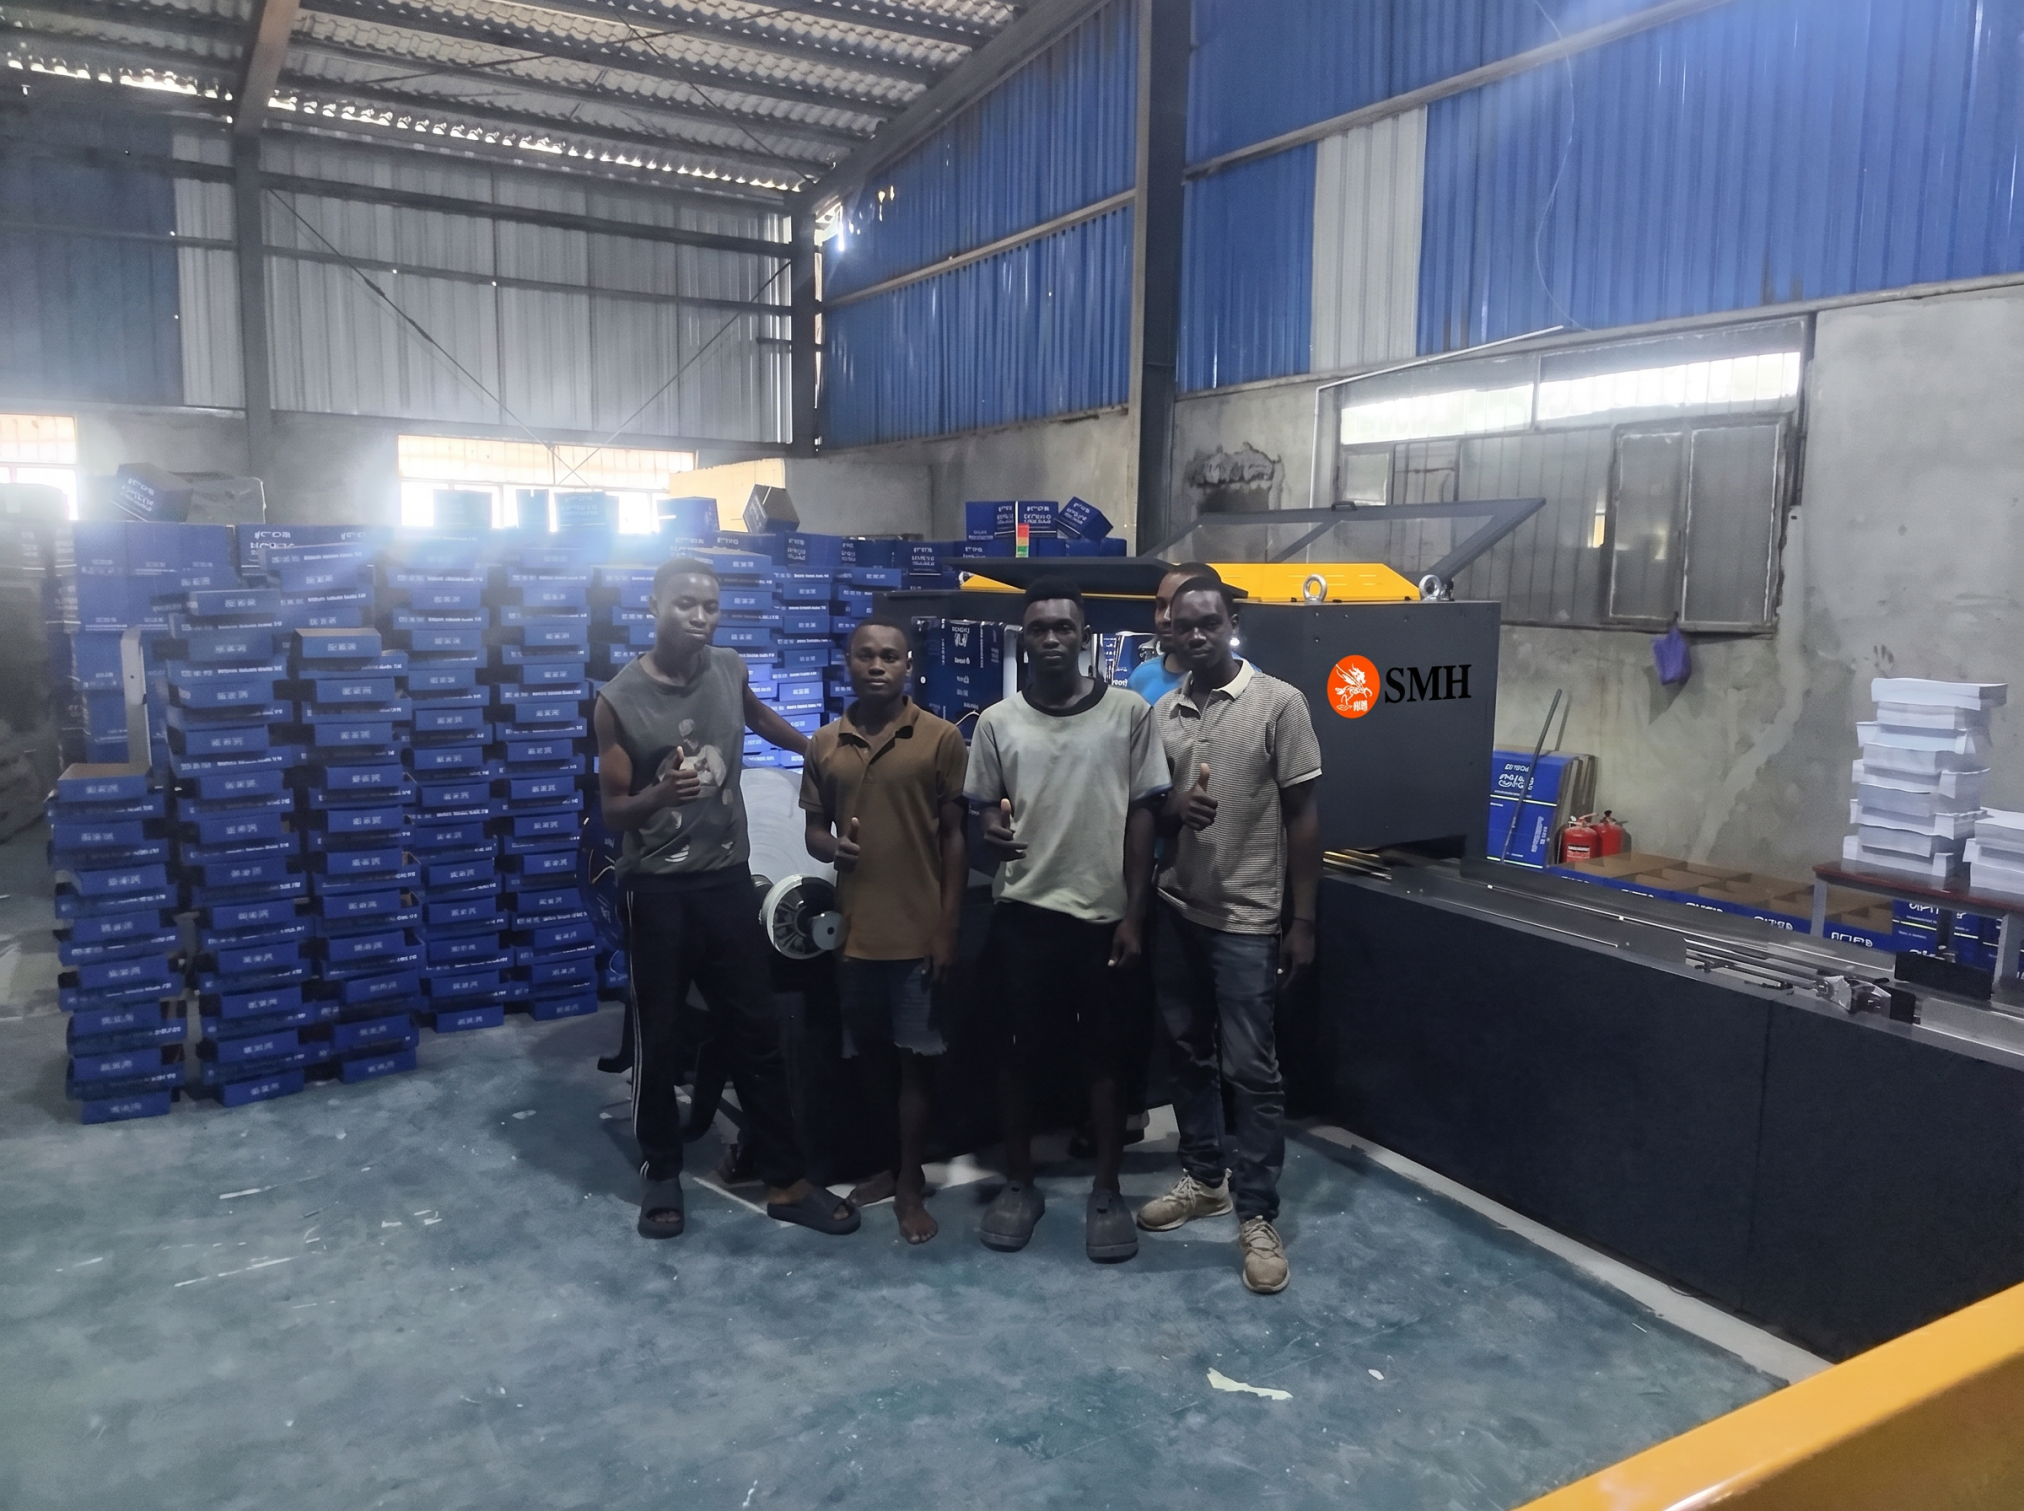
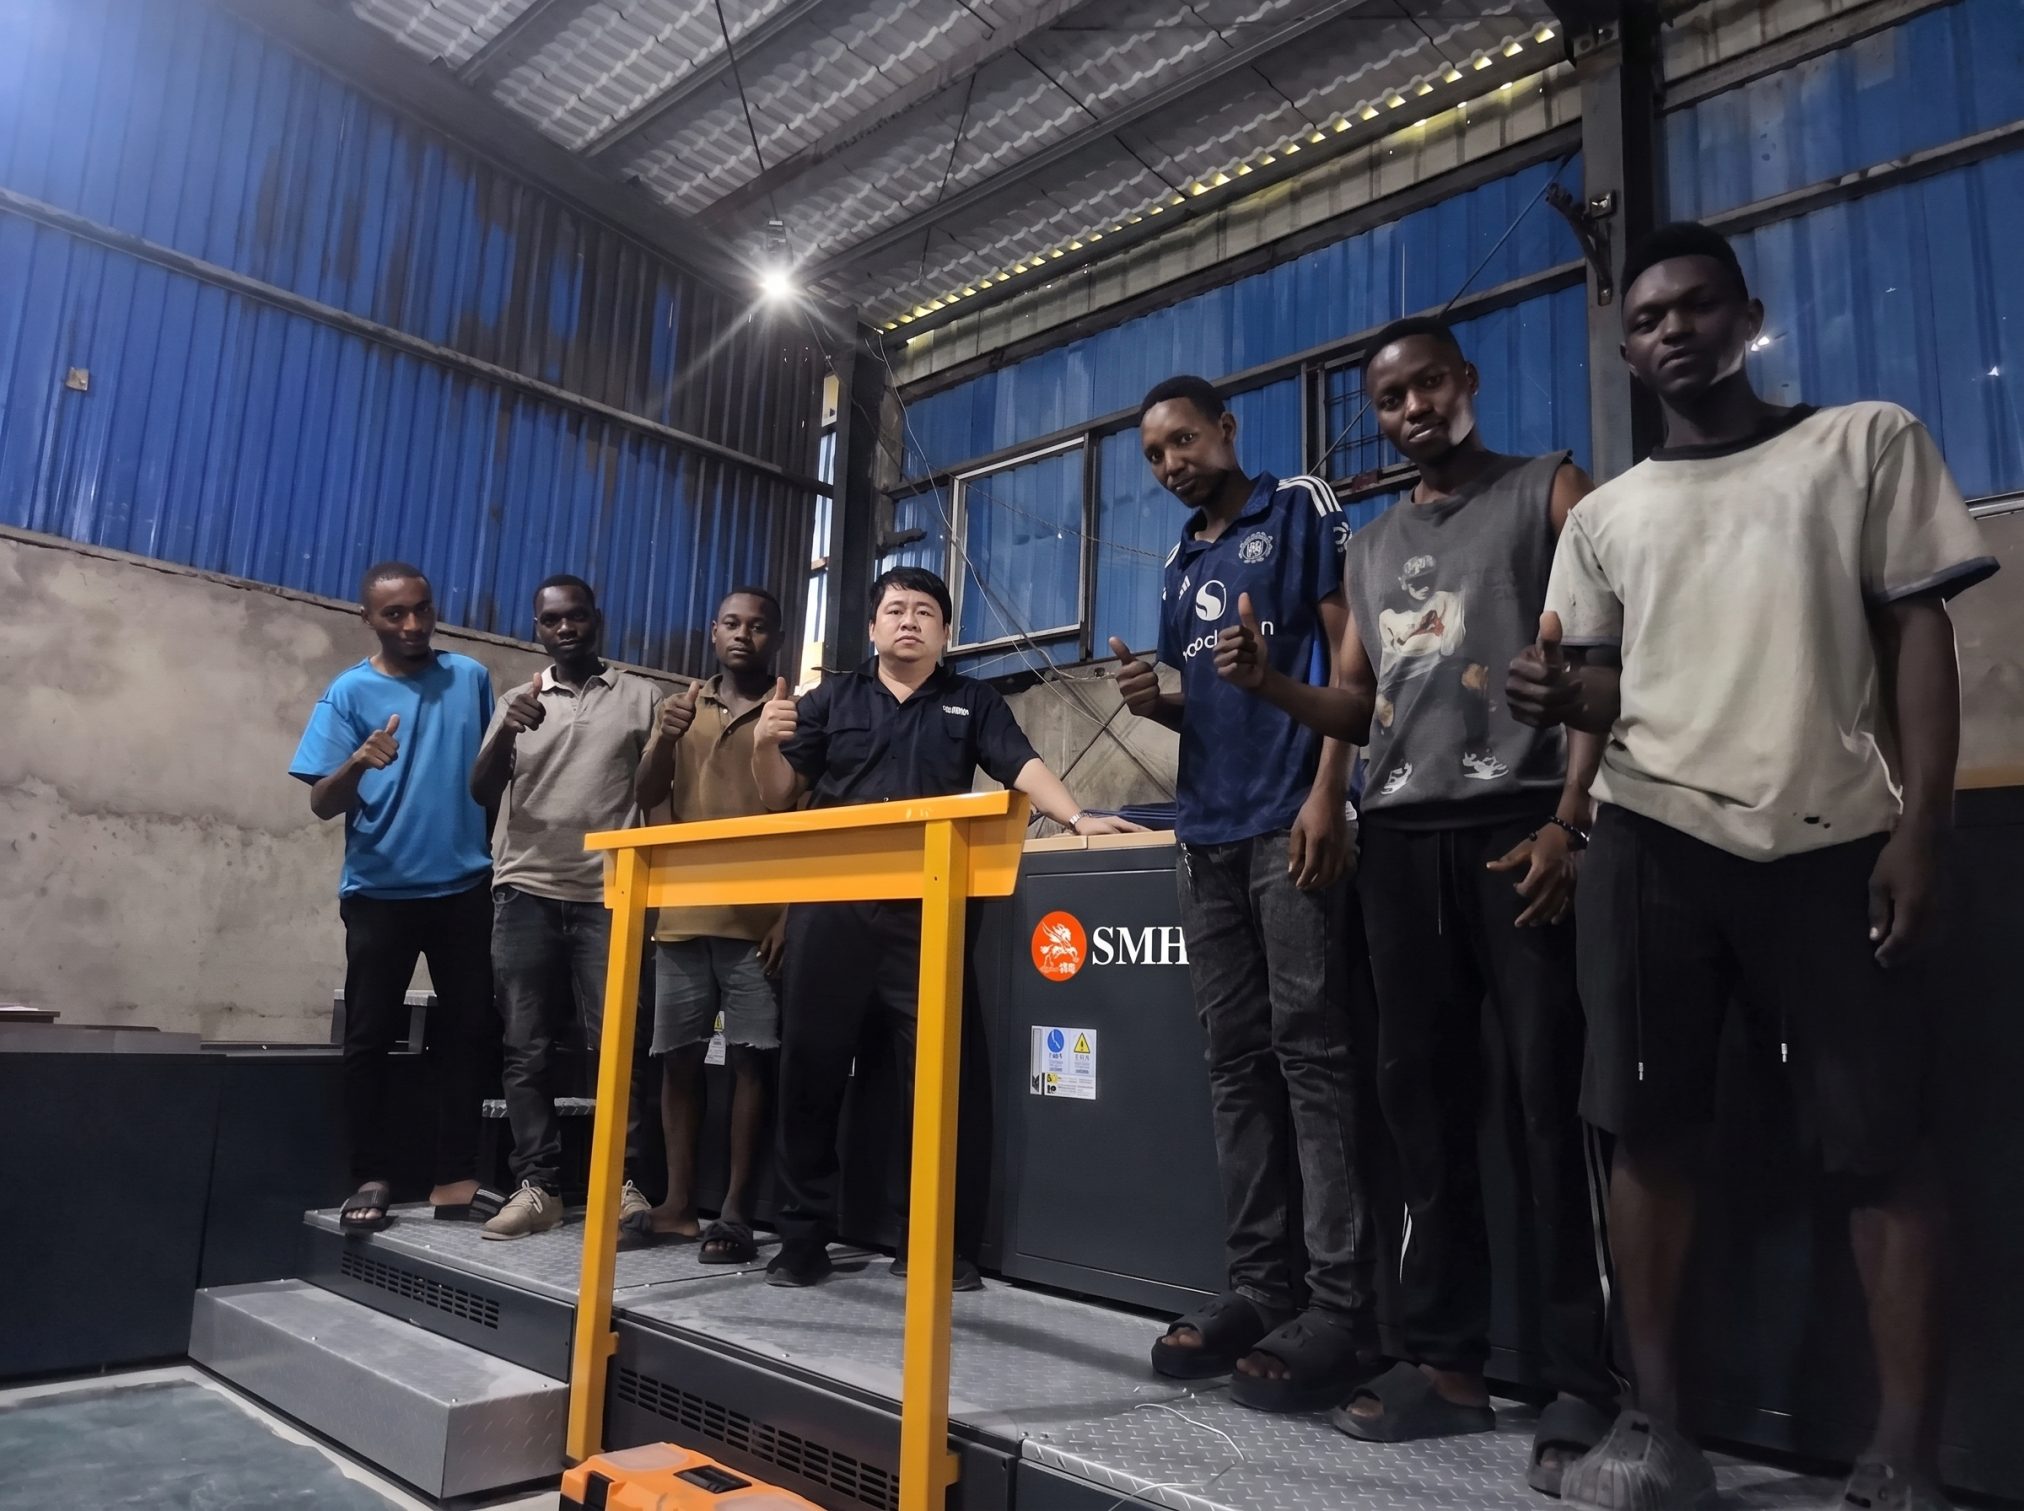
A new A4 paper production line featuring the SMH A4-5 sheeter and A4B packing machine has recently been installed and commissioned in Tanzania. The project marks a practical step for the local converter, moving from basic supply toward integrated, in-house processing.

From Manual to Continuous Production

Before the upgrade, the factory relied heavily on semi-manual operations. Cutting speed was limited, packing consistency varied, and output depended on labor coordination.

Now, with the A4-5 and A4B running, the workflow is stable and continuous. Jumbo rolls convert directly into A4 sheets, then automatically counted and packed. Output stays consistent across shifts, with less manual intervention and better predictability.

Why A4-5 Was Selected

The factory chose the A4-5 to meet rising demand and support future growth. Its wider web handling and higher cutting capacity allow more paper processed in the same time.

Key benefits in daily operation:

  • Stable cutting accuracy at continuous speed
  • Consistent sheet size across large volumes
  • Less material waste from better control

For a market where both volume and reliability matter, these give a clear edge.

Packing Stability with A4B

The A4B packing machine solves a common bottleneck: end-of-line handling. Instead of manual counting and wrapping, the system delivers uniform ream packaging, stable sealing, and synchronized output with the sheeter. Finished products are ready for shipment without rework or delay.

Adapted to Local Conditions

The Tanzania installation was configured with three practical considerations:

  • Compatibility with local paper grades
  • Stable performance under variable power conditions
  • Simplified operation for local teams

SMH engineers supported installation and operator training, so the line ran reliably from the start.

Operational Impact

Since commissioning, the factory reports:

  • Higher daily output with fewer interruptions
  • More consistent product quality
  • Reduced dependence on manual labor
  • Better ability to handle bulk and repeat orders

The business no longer limits itself to trading or basic processing – it now controls a larger part of the value chain.

Conclusion

The A4-5 and A4B installation in Tanzania reflects a broader shift: moving from manual, fragmented operations to integrated, automated production. By stabilizing both cutting and packing, the line provides not only higher capacity but also the consistency needed to compete in a growing market.

Need to upgrade your A4 line?

If you’re planning to move toward in-house A4 converting, SMH can help design a solution based on your actual production conditions.

Contact SMH to evaluate your line setup and improve output stability.

What Causes Paper Dust During Cutting & How to Reduce It

Keywords: paper dust problem, cutting quality, knife conditionPaper dust is one of those issues many factories ignore until it’s too late. It builds up in motors, sensors, and gearboxes, shortens maintenance cycles, and leaves messy edges on finished sheets—directly hurting product quality and customer satisfaction.

From our on-site observations, paper dust almost always comes from three root causes:

  • Worn or blunt knives: Instead of making clean cuts, dull blades tear paper fibers, creating a lot of fine dust.
  • Wrong cutting angle or pressure: Too much friction during cutting heats the paper and breaks fibers unnecessarily.
  • Over-dry paper: Paper that’s too low in moisture becomes brittle and sheds dust easily when cut at high speed.

Controlling dust isn’t just about cleaning the machine more often. SMH uses precision-ground blades, optimized cutting geometry, and stable running parameters to minimize fiber tearing at the source, giving you cleaner cuts, less dust, and higher material yield.