Why More Global Paper Mills Are Choosing SMH

Production Efficiency Is Becoming the Core Competitiveness of Paper Mills

In today’s paper converting industry, rising labor costs, increasing market competition, and higher delivery requirements are forcing paper manufacturers to improve production efficiency. For many factories, equipment stability and automation level directly affect production cost and profitability.

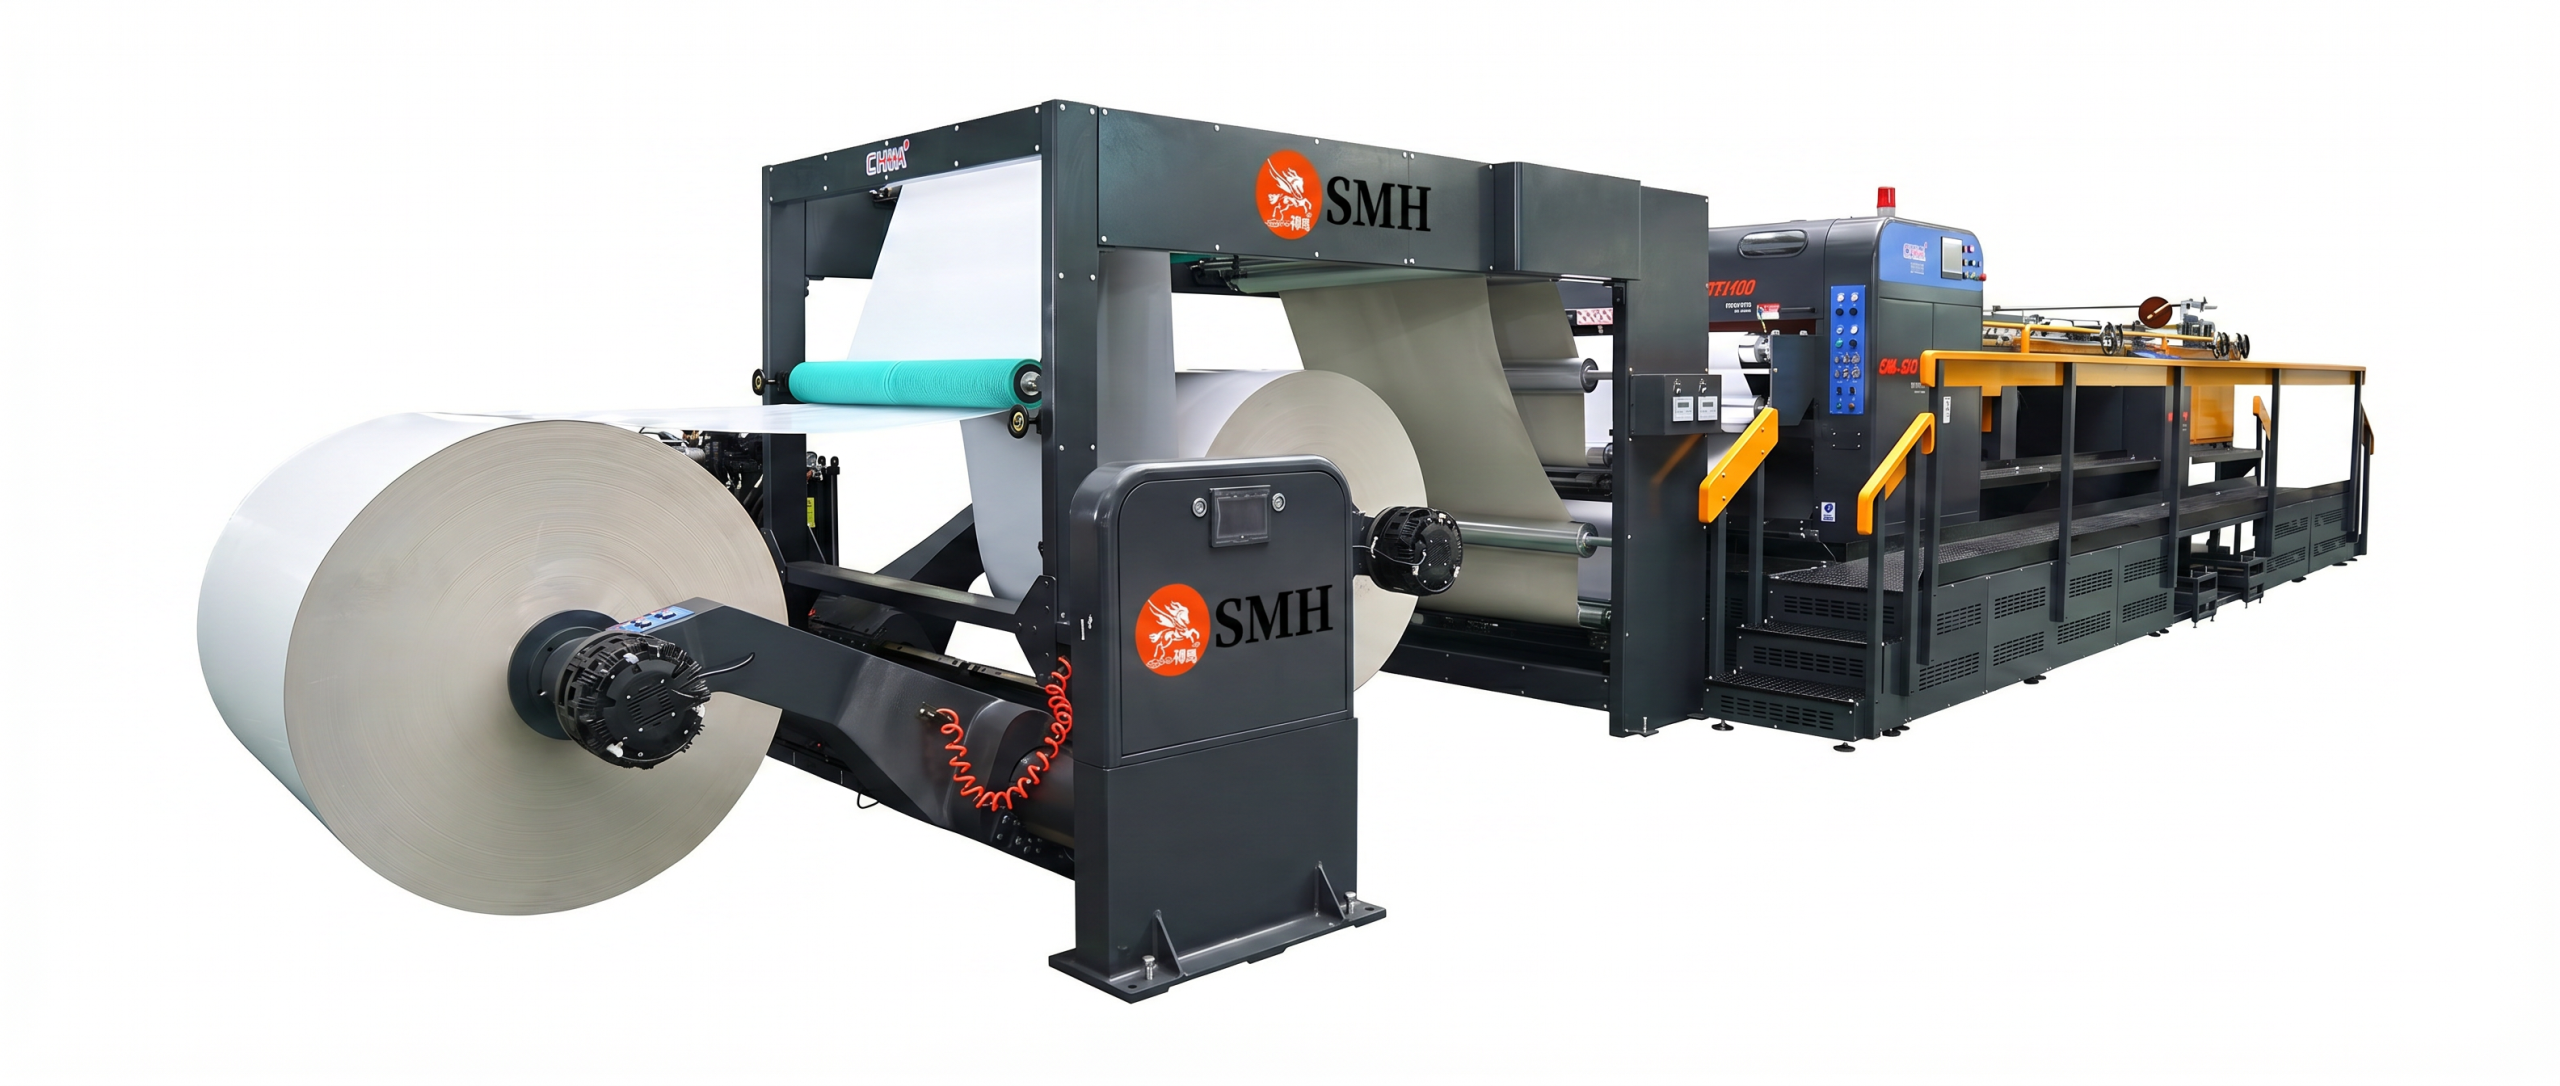
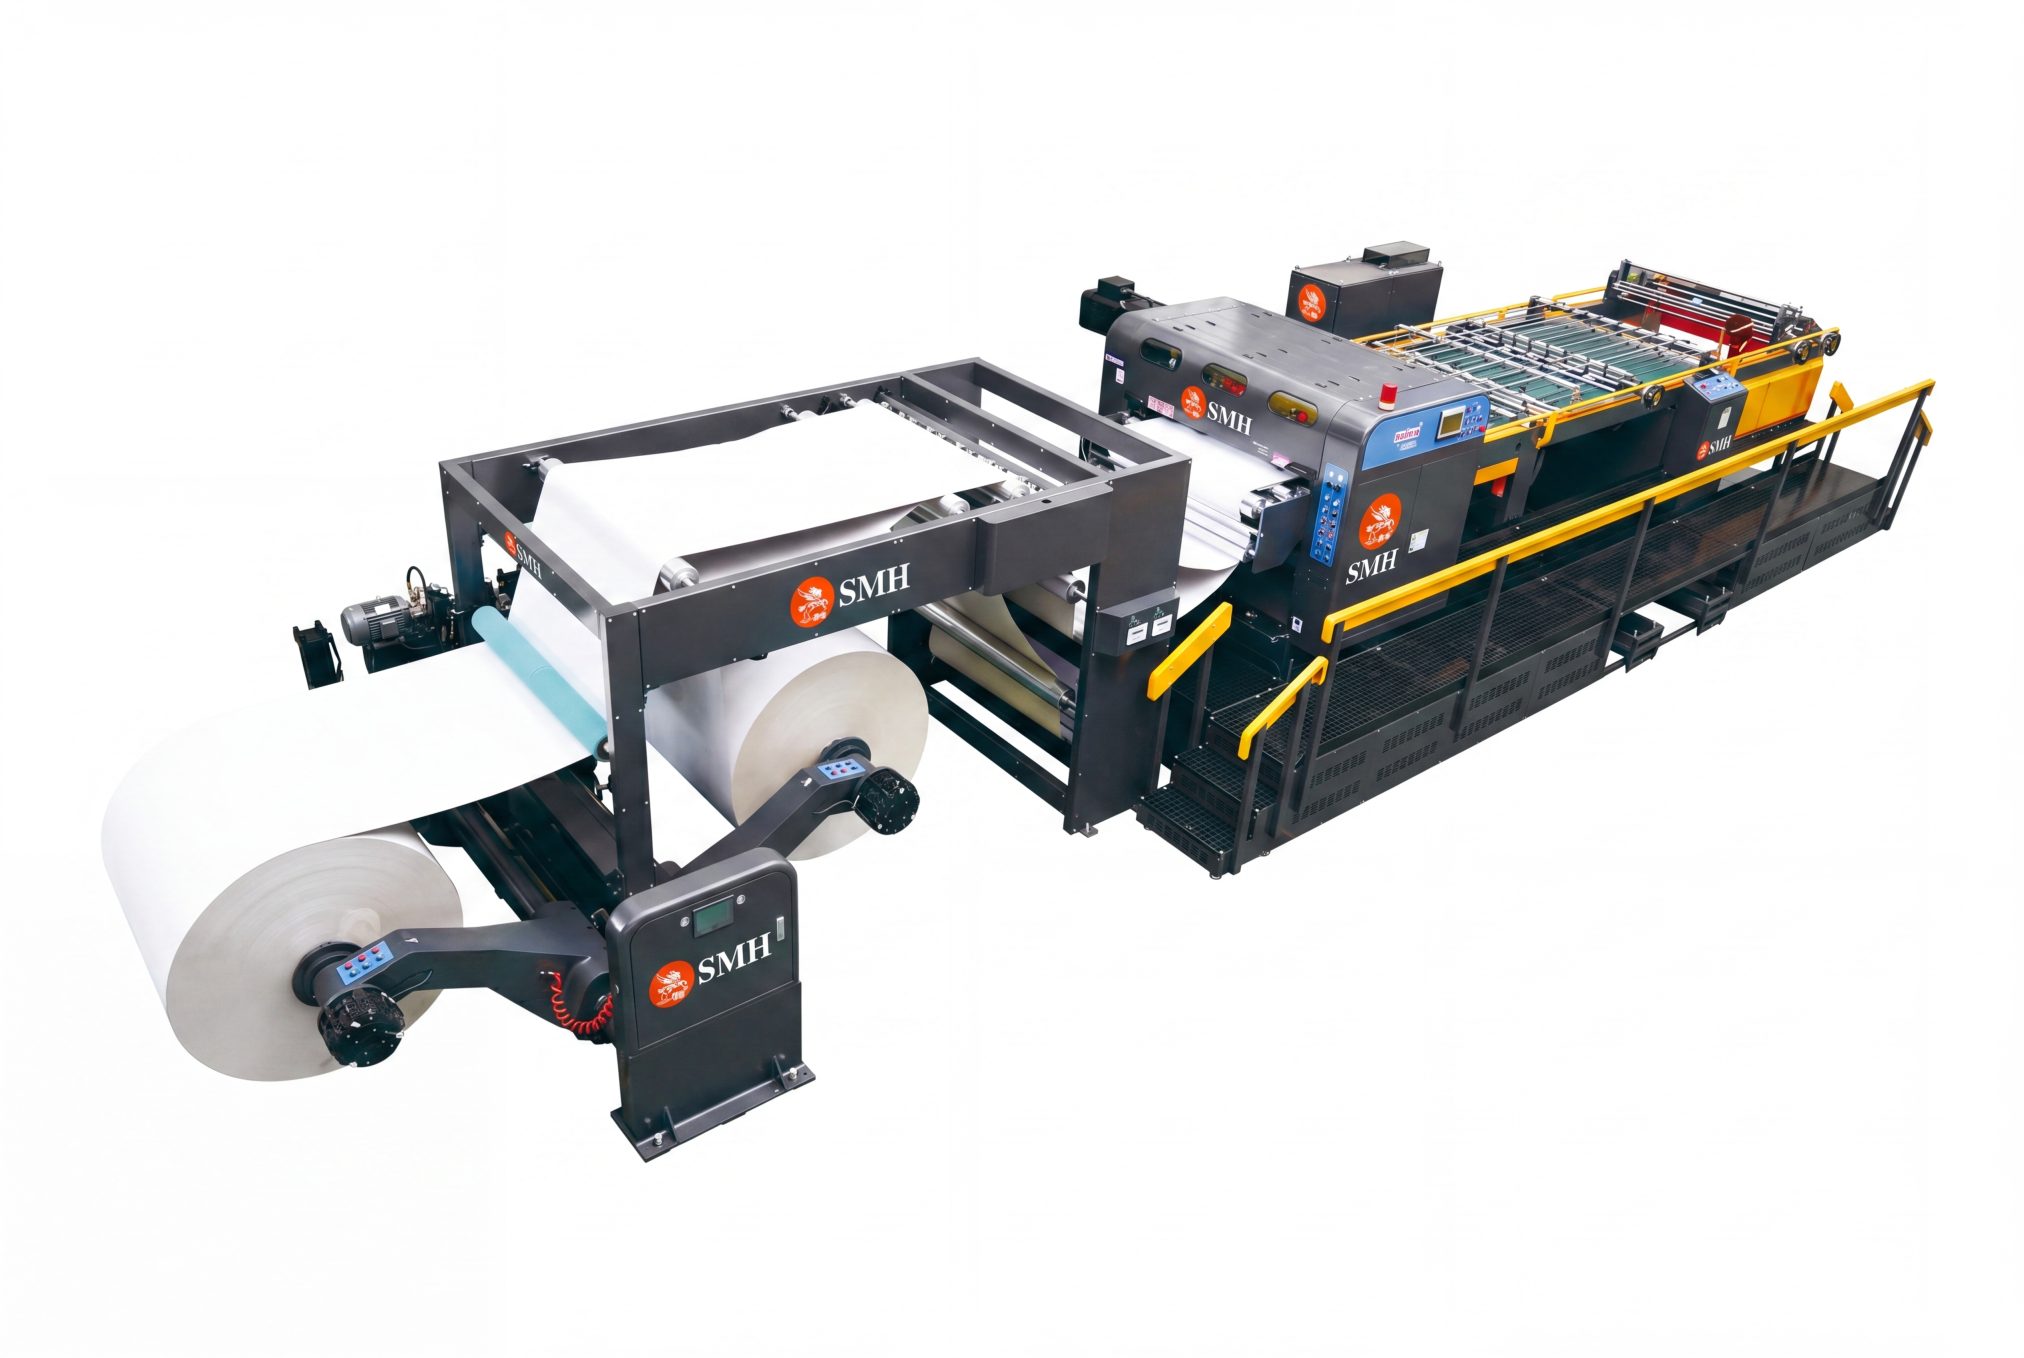
This is one of the main reasons why more paper mills worldwide are upgrading to automatic paper sheeting and packaging systems from SMH.

Reducing Labor Costs Through Automation
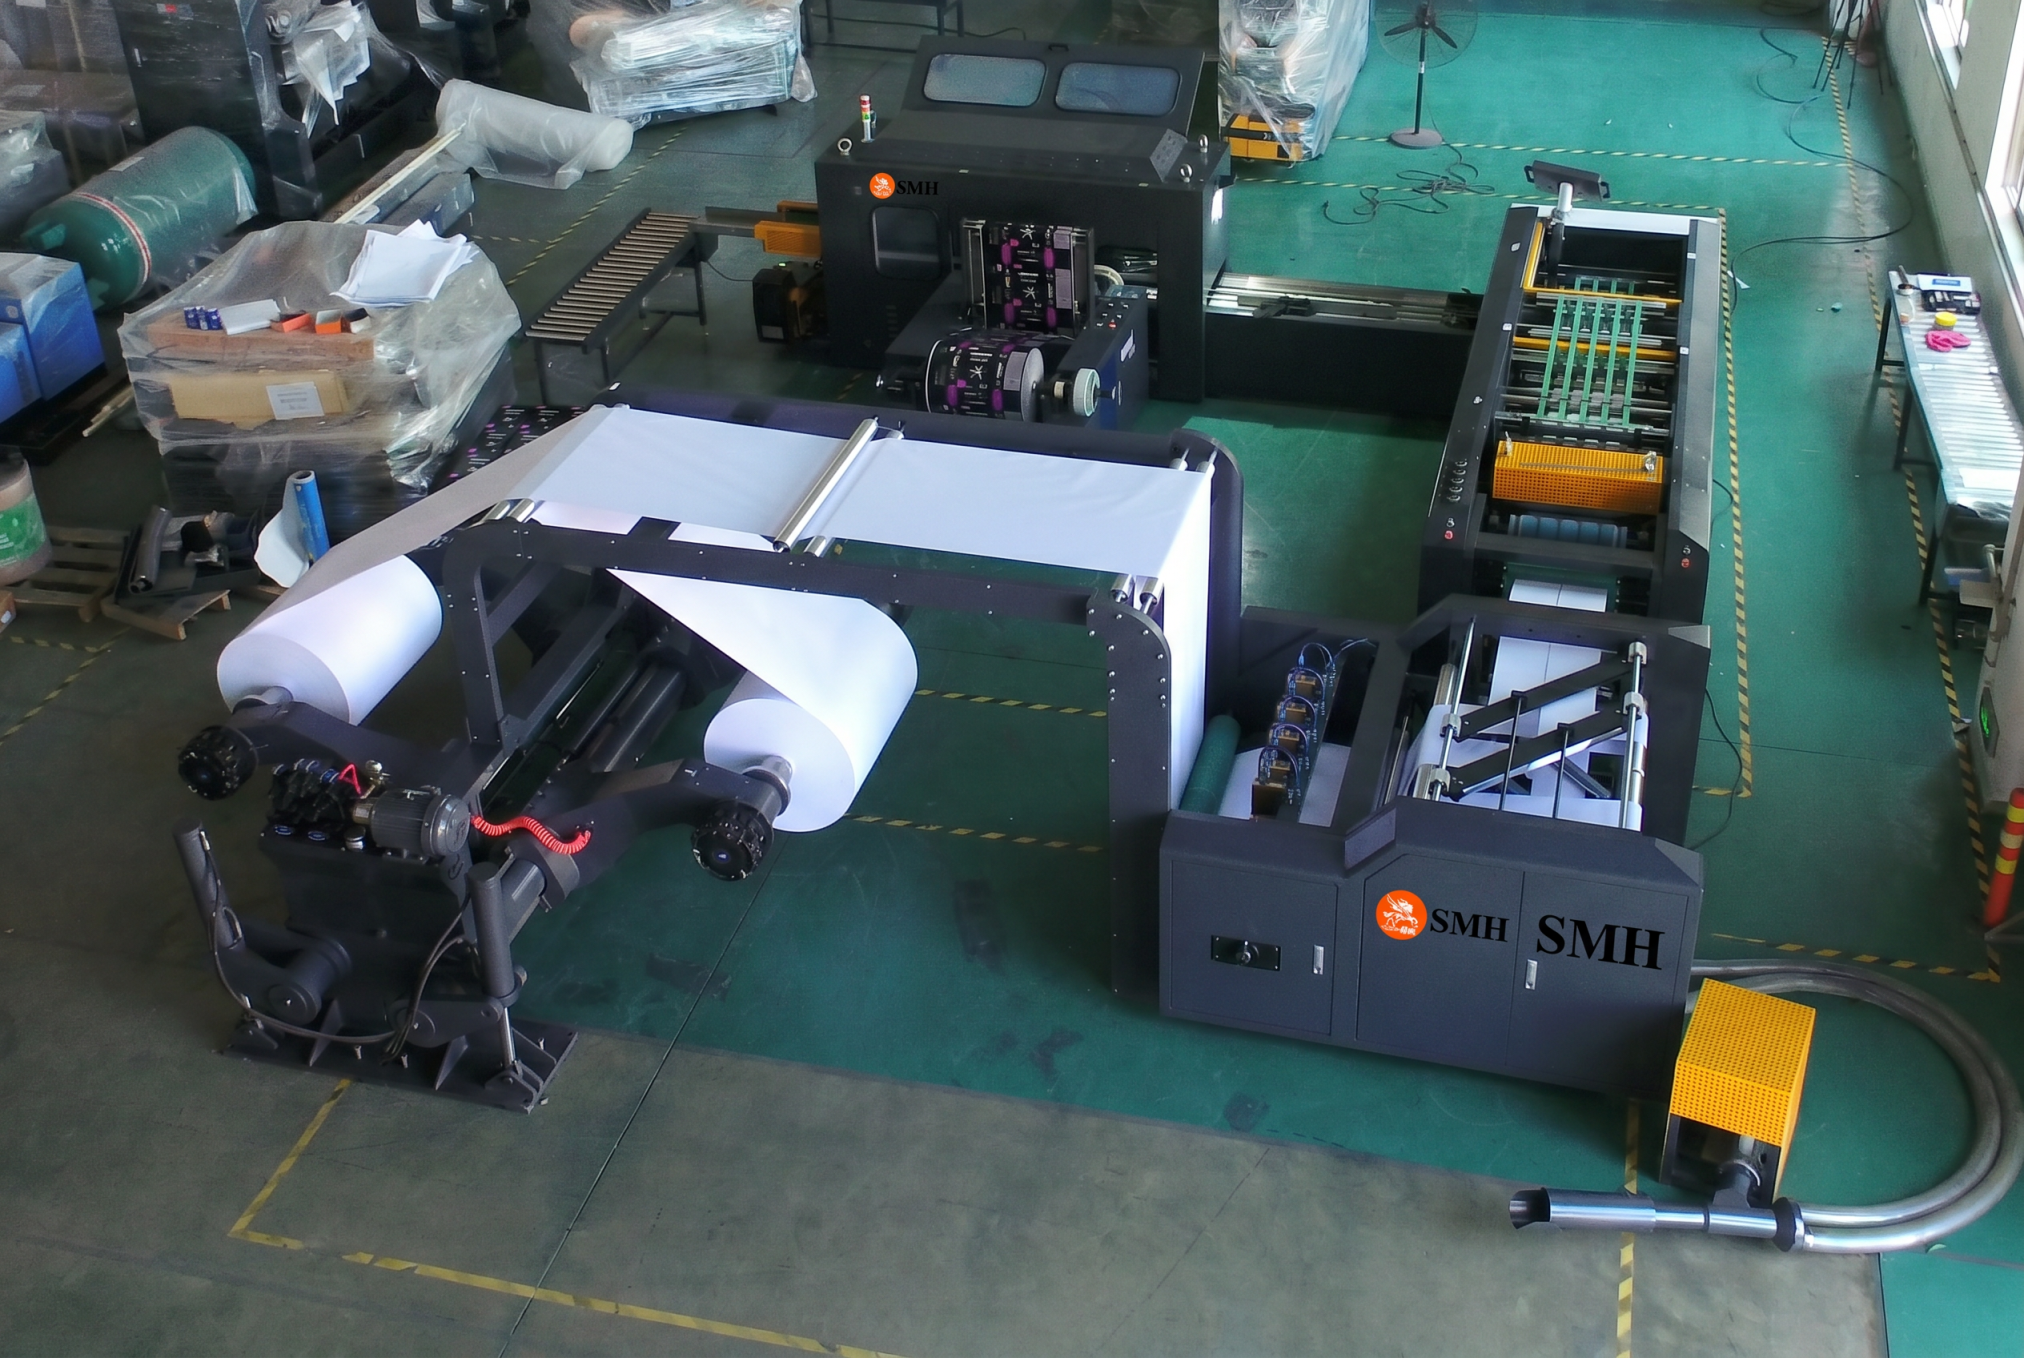
Traditional paper converting production often relies heavily on manual operation. Frequent material handling, packaging, pallet replacement, and paper inspection increase labor costs and production risks.

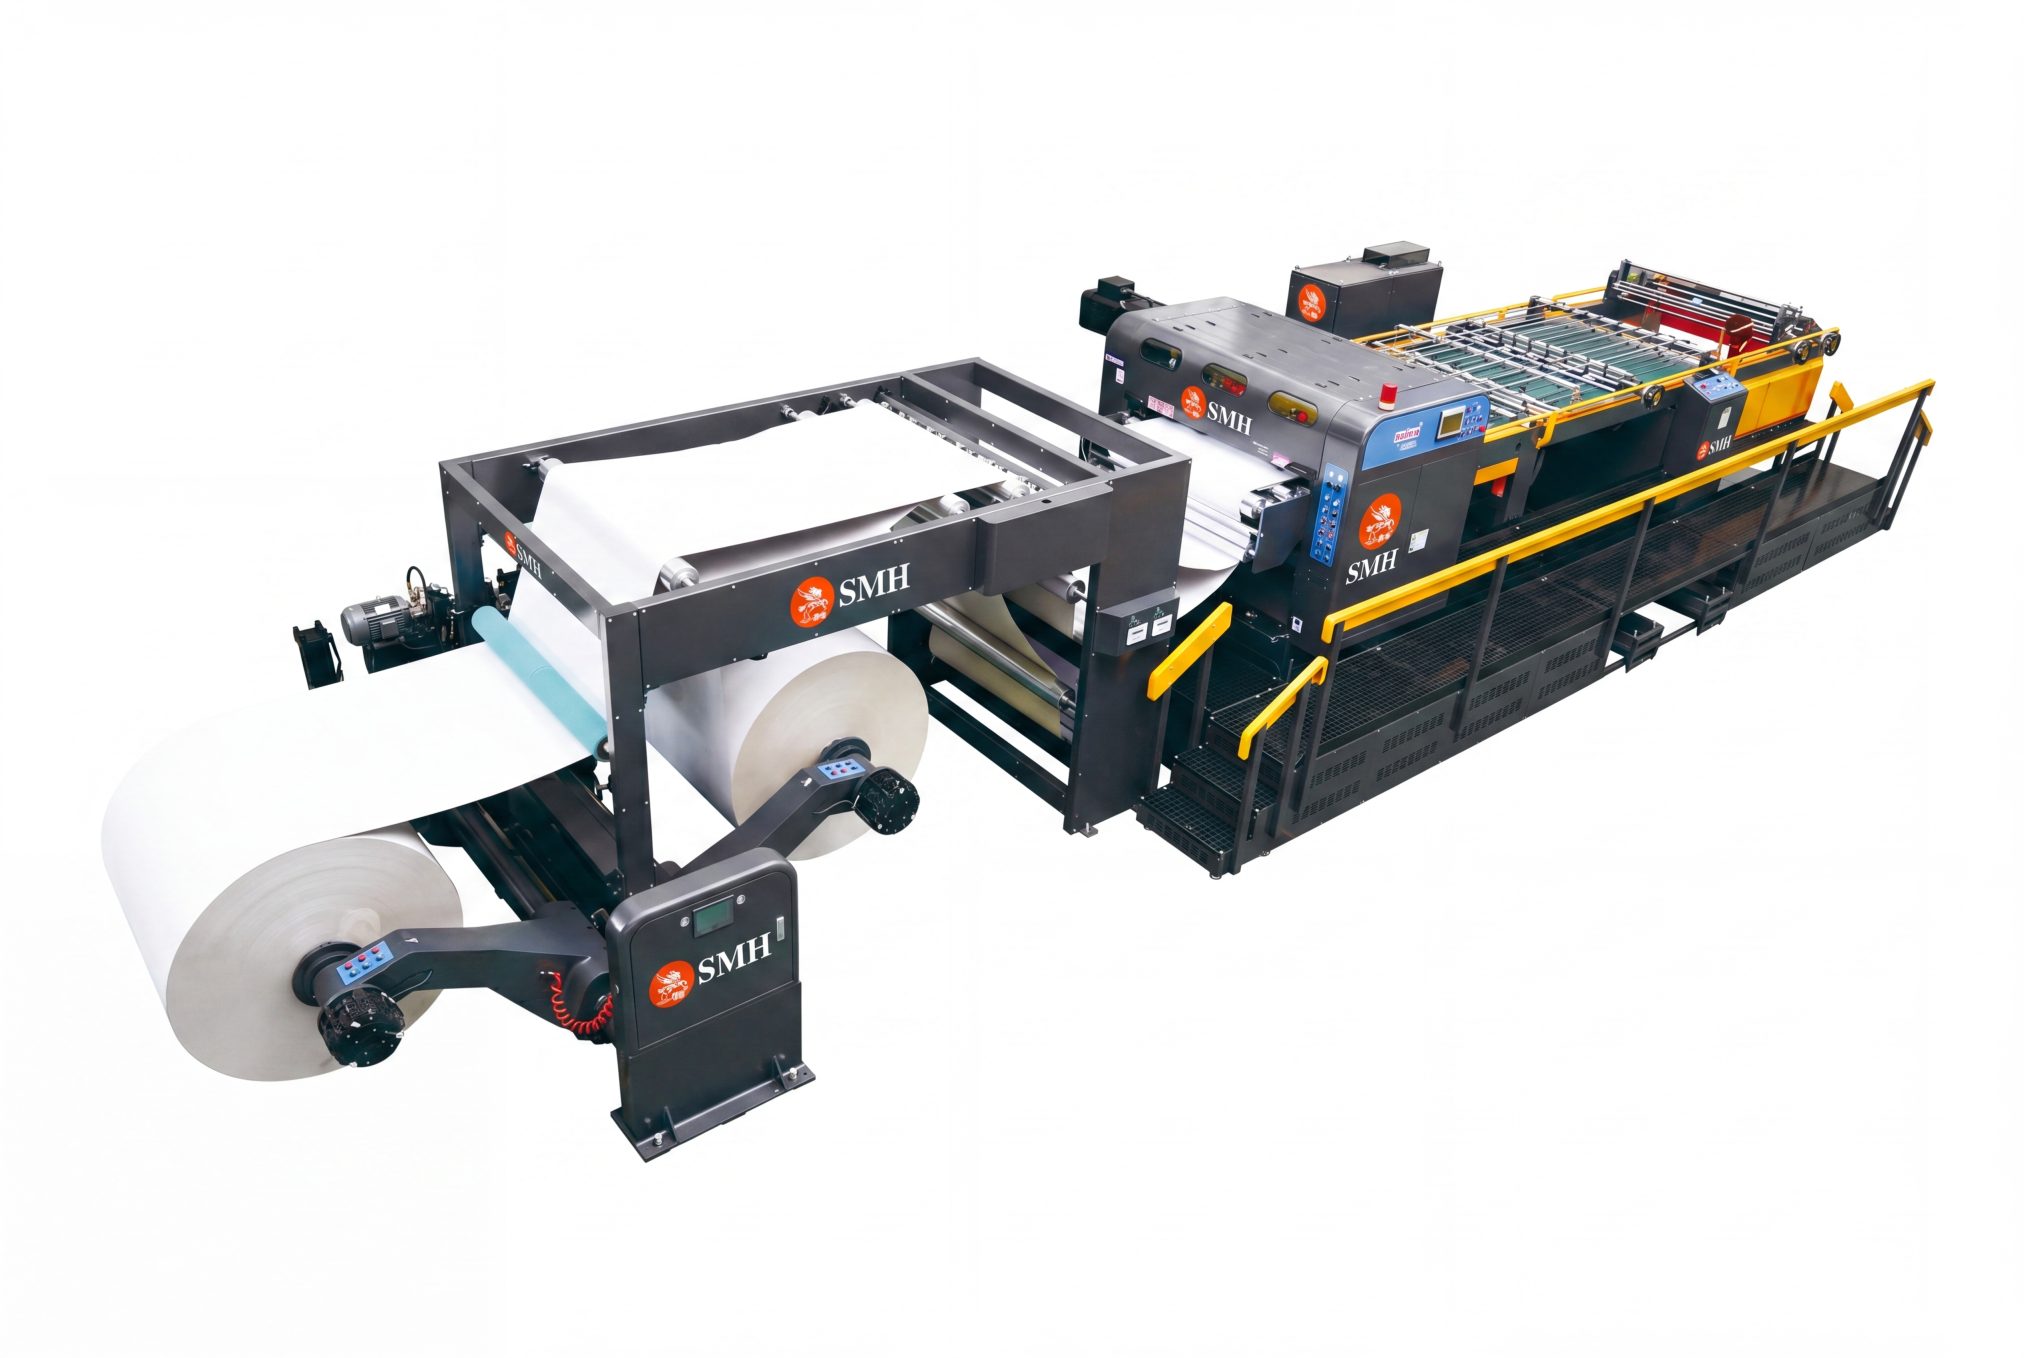
SMH automatic production lines integrate paper sheeting, counting, packaging, stacking, and conveying into one continuous process. Automatic pallet changing systems and robotic stacking devices help reduce manual operation while improving production consistency.

For large-scale paper mills, automation not only reduces labor dependency but also improves production stability during long-term operation.

Stable Production Means Lower Operating Costs

High-speed equipment must maintain stable operation over long production cycles. Unstable cutting precision, paper dust, and machine vibration can increase waste and maintenance costs.

SMH focuses on improving:

  • Cutting precision
  • Servo synchronization accuracy
  • Tension control stability
  • Automatic fault detection
  • Long-term running reliability

Stable production helps factories reduce paper waste, minimize downtime, and improve final product quality.

Complete Production Line Solutions

SMH provides complete paper converting solutions including:

  • Paper sheeters
  • A4 copy paper production lines
  • Ream wrapping systems
  • Carton packing systems
  • Automatic conveying solutions

By integrating multiple production processes into one automated workflow, customers can significantly improve overall factory efficiency.

Supporting Long-Term Factory Growth

Today, SMH equipment serves customers across Asia, Europe, Africa, and South America. As paper manufacturers continue expanding production capacity, automation and intelligent production systems will remain key drivers of industry development.

SMH continues providing efficient and stable equipment solutions to help customers improve productivity and reduce operating costs in competitive global markets.
Why Some Slitting Lines Produce More Paper Dust

Paper Dust Is Usually a Sign of Instability

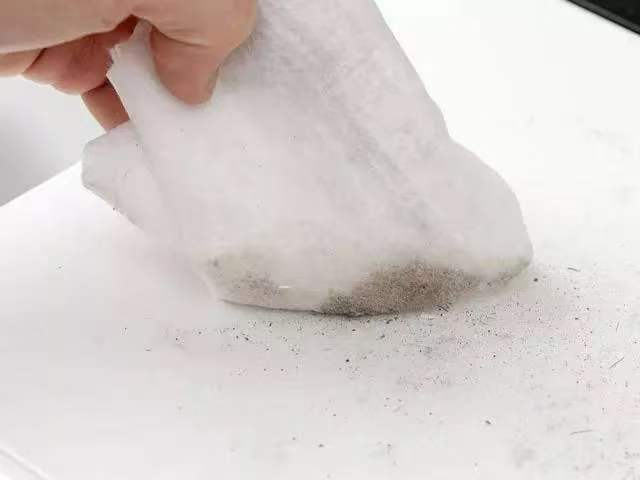
Paper dust
Paper dust

A small amount of paper dust is difficult to avoid completely.

But when dust becomes excessive, something in the process is usually unstable.

Operators often notice it first around the knife area. Dust begins collecting near rollers, conveyors, and finished stacks.

In serious cases, dust also affects printing quality and downstream converting.

Knife Condition Is Only One Part of the Problem

Worn knives are a common reason for dust. A dull edge tears fibers instead of cutting cleanly.

But even new knives can still create dust if:

  • knife alignment is incorrect
  • tension is unstable
  • machine vibration is high
  • pressure settings are inconsistent

That is why replacing blades alone does not always solve the issue.

Thick Paper and High Speed Increase Dust Risk

Heavy paper grades create stronger cutting resistance. At higher speed, the cutting force increases further.

If the cutting system is unstable, fiber tearing becomes more serious. That increases dust generation quickly.

Single knife systems are more sensitive to this because the cutting force comes mainly from one side.

Double knife systems usually reduce dust because the cutting force stays more balanced. The paper separates more smoothly during cutting.

Vibration Creates Hidden Quality Problems

Many factories underestimate vibration.

Even slight vibration affects knife contact consistency. Once knife contact changes, the edge quality changes too.

This can create:

  • uneven fiber cutting
  • rough edges
  • dust buildup
  • unstable slit quality

At low speed the problem may appear manageable. At high speed it becomes much more visible.

Stable Cutting Conditions Reduce Dust Naturally

Factories with lower paper dust levels usually maintain:

  • stable knife alignment
  • correct knife clearance
  • balanced tension
  • synchronized feeding speed
  • clean roller surfaces

The goal is not simply reducing dust after production. The goal is preventing unstable cutting conditions before dust forms.

Why High-Speed Slitting Machines Need Better Stability

High Speed Alone Does Not Guarantee Higher Output

warehouse
warehouse

Many factories want faster production. That is normal.

But after increasing machine speed, some lines actually produce more waste instead of more good products.

The paper starts drifting. Stacking becomes messy. Edge quality changes. Operators begin slowing the line down again.

This happens because high-speed production magnifies small mechanical problems.

Small Errors Become Bigger at High Speed

At low speed, slight tension changes may not be obvious. Minor vibration may also go unnoticed.

At high speed, those same problems become much more serious.

A tiny knife vibration can affect cutting accuracy. Small tension fluctuations can change sheet length. Slight roller slipping can cause feeding instability.

The faster the line runs, the less room there is for error.

That is why stable high-speed production depends heavily on machine rigidity and synchronized control.

The Machine Structure Matters More Than Operators Think

In many factories, operators try solving instability by adjusting parameters repeatedly. Sometimes they change tension. Sometimes they reduce speed. Sometimes they increase knife pressure.

But if the machine structure itself is unstable, adjustments only provide temporary improvement.

A stable high-speed slitting machine usually includes:

  • rigid machine frame
  • stable roller system
  • synchronized servo control
  • accurate guiding system
  • consistent tension control

Without these conditions, running faster only increases instability.

Why Double Knife Systems Run More Smoothly

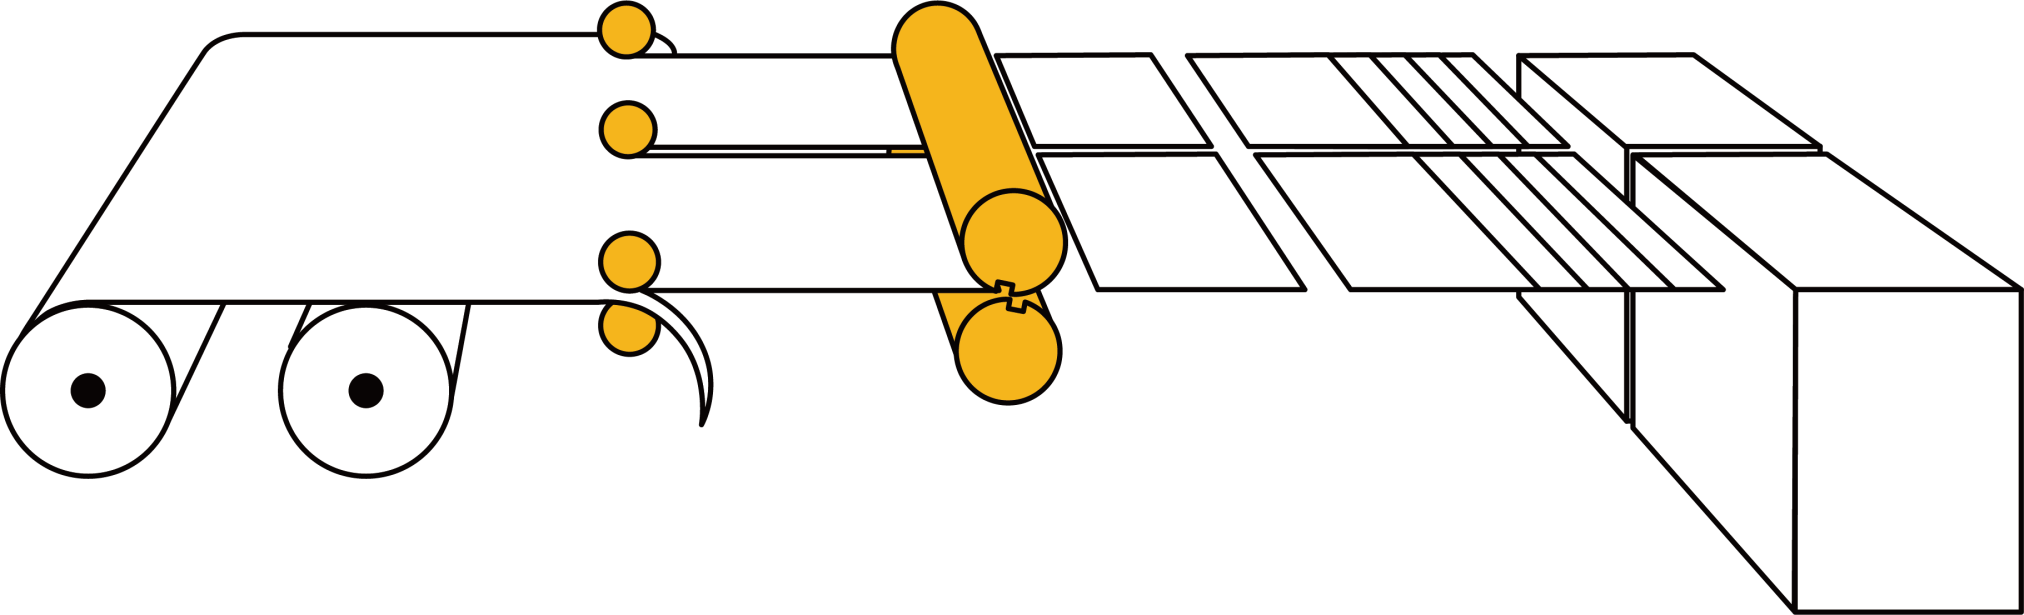
double rotary sheeter

Double knife systems are widely used in high-speed applications because the cutting process stays more balanced.

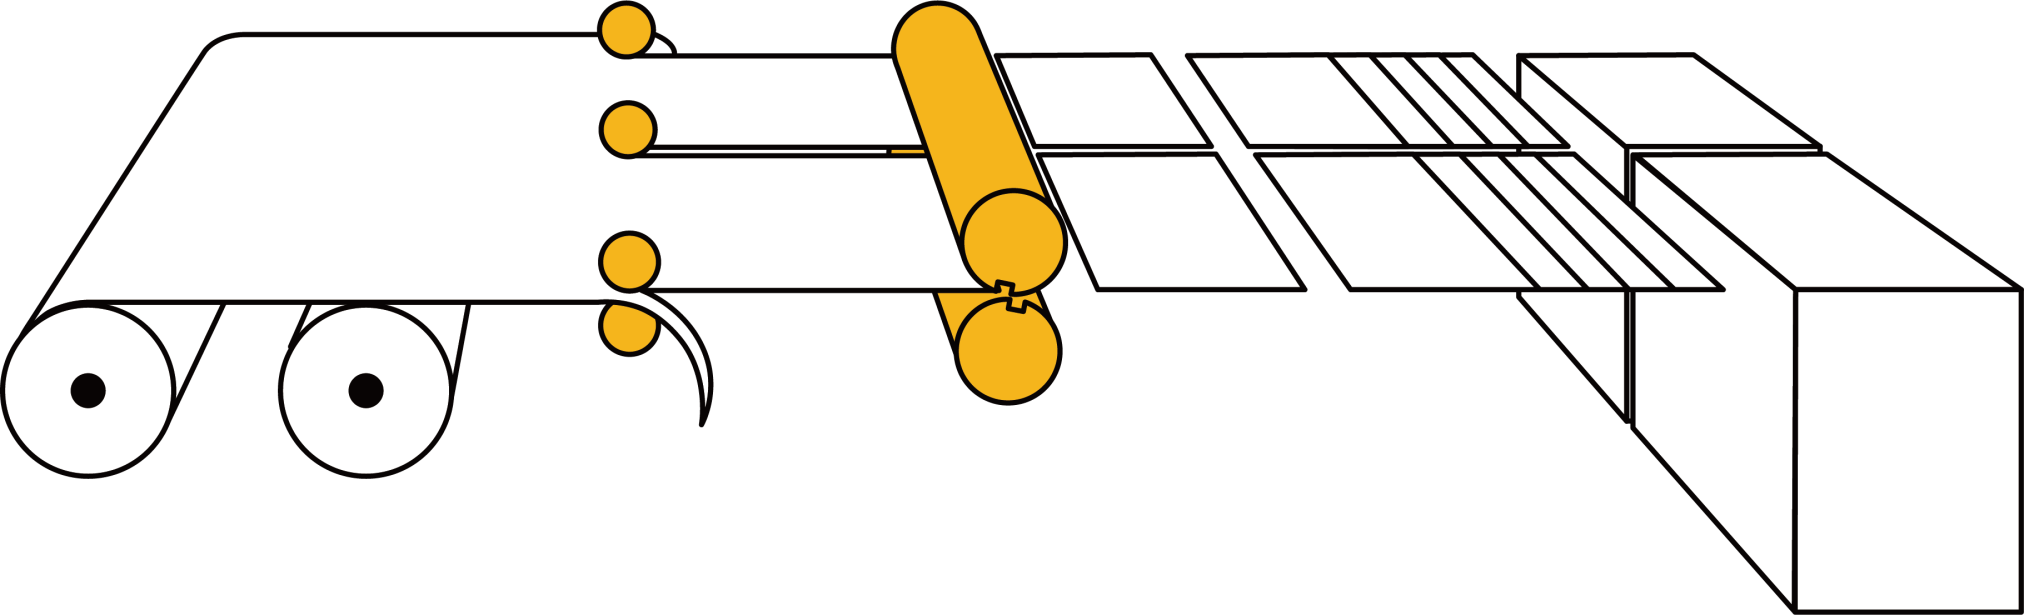
Both knife rollers rotate synchronously. The material receives cutting force from both sides. The paper movement becomes smoother.

Compared with impact-style cutting, vibration is lower. That helps maintain edge quality during long production runs.

This is especially important in:

  • coated paper production
  • packaging board converting
  • high GSM paper processing
  • large-volume paper mills

Stable Production Is More Valuable Than Peak Speed

In real factory operation, customers care more about consistent production than temporary peak speed.

A line that runs steadily for hours is usually more profitable than a line that reaches very high speed but stops constantly.

That is why experienced factories focus on:

  • stable output
  • lower waste
  • repeatable quality
  • reduced operator intervention

The real goal is not simply running fast. It is running fast without losing control.

Why Thick Paper Produces Burrs During Slitting

Burr Problems Usually Start When Material Changes

Edge of the paper
Edge of the paper

A production line may run perfectly with thin paper. Then one day the factory switches to heavier board. Suddenly the edge quality changes.

Paper dust increases. Small burrs appear. Sometimes the cut edge even feels rough by hand.

Many operators first suspect the knife. But in real production, the knife is often only part of the reason.

The bigger issue is that thick paper behaves completely differently during cutting.

Thick Paper Needs Different Cutting Force

thin paper
thin paper

Thin paper is flexible. It separates more easily during slitting.

Heavy board is different. The material is stiffer. The cutting resistance is much higher.

If the machine still uses impact-style cutting, the pressure concentrates on one side of the sheet. That creates stress around the cutting point.

At lower speed, the issue may not look serious. At higher speed, burrs become much more obvious.

This is why some factories notice edge problems only after increasing production speed.

Machine Structure Directly Affects Edge Quality

In single knife systems, the upper knife rotates while the lower knife stays fixed. The cutting process depends heavily on pressure and impact force.

For thin paper, this is usually acceptable. For thick board, the cutting process becomes less stable.

Double knife systems reduce this problem because both knife rollers rotate together. The material is cut from both sides simultaneously.

Double helical cross-cutting knife set

The cutting force stays more balanced. The paper deforms less. The edge quality becomes cleaner.

That is one reason why high-end packaging factories prefer double knife slitting machines for thick material production.

Burrs Are Not Caused by One Factor Alone

In actual factory production, burrs usually come from multiple small problems together.

Common causes include:

  • incorrect knife gap
  • worn knife edges
  • unstable tension
  • vibration at high speed
  • poor knife alignment
  • unsuitable machine structure

Operators sometimes keep adjusting knife pressure to solve the issue. But too much pressure can create more friction and shorten knife life.

The better solution is finding the real source of instability first.

Stable Production Depends on System Matching

SMH-SGT1400double rotary sheeter

Factories with stable thick paper production usually control several things carefully:

  • proper knife structure
  • stable web tension
  • synchronized feeding speed
  • correct knife clearance
  • rigid machine frame

When these conditions stay stable, burr problems reduce significantly.

The goal is not simply increasing pressure. The goal is maintaining stable cutting conditions throughout the entire run.