Inside SMH’s 140,000㎡ Manufacturing Base: How High-Precision Paper Sheeters Are Built

Modern Manufacturing Behind Precision Paper Converting Equipment

As the global paper converting industry continues moving toward automation and intelligent manufacturing, equipment precision and production stability have become key factors for paper mills and packaging factories. Behind every stable paper sheeter and slitting machine is a complete manufacturing system designed for accuracy, efficiency, and long-term operation.

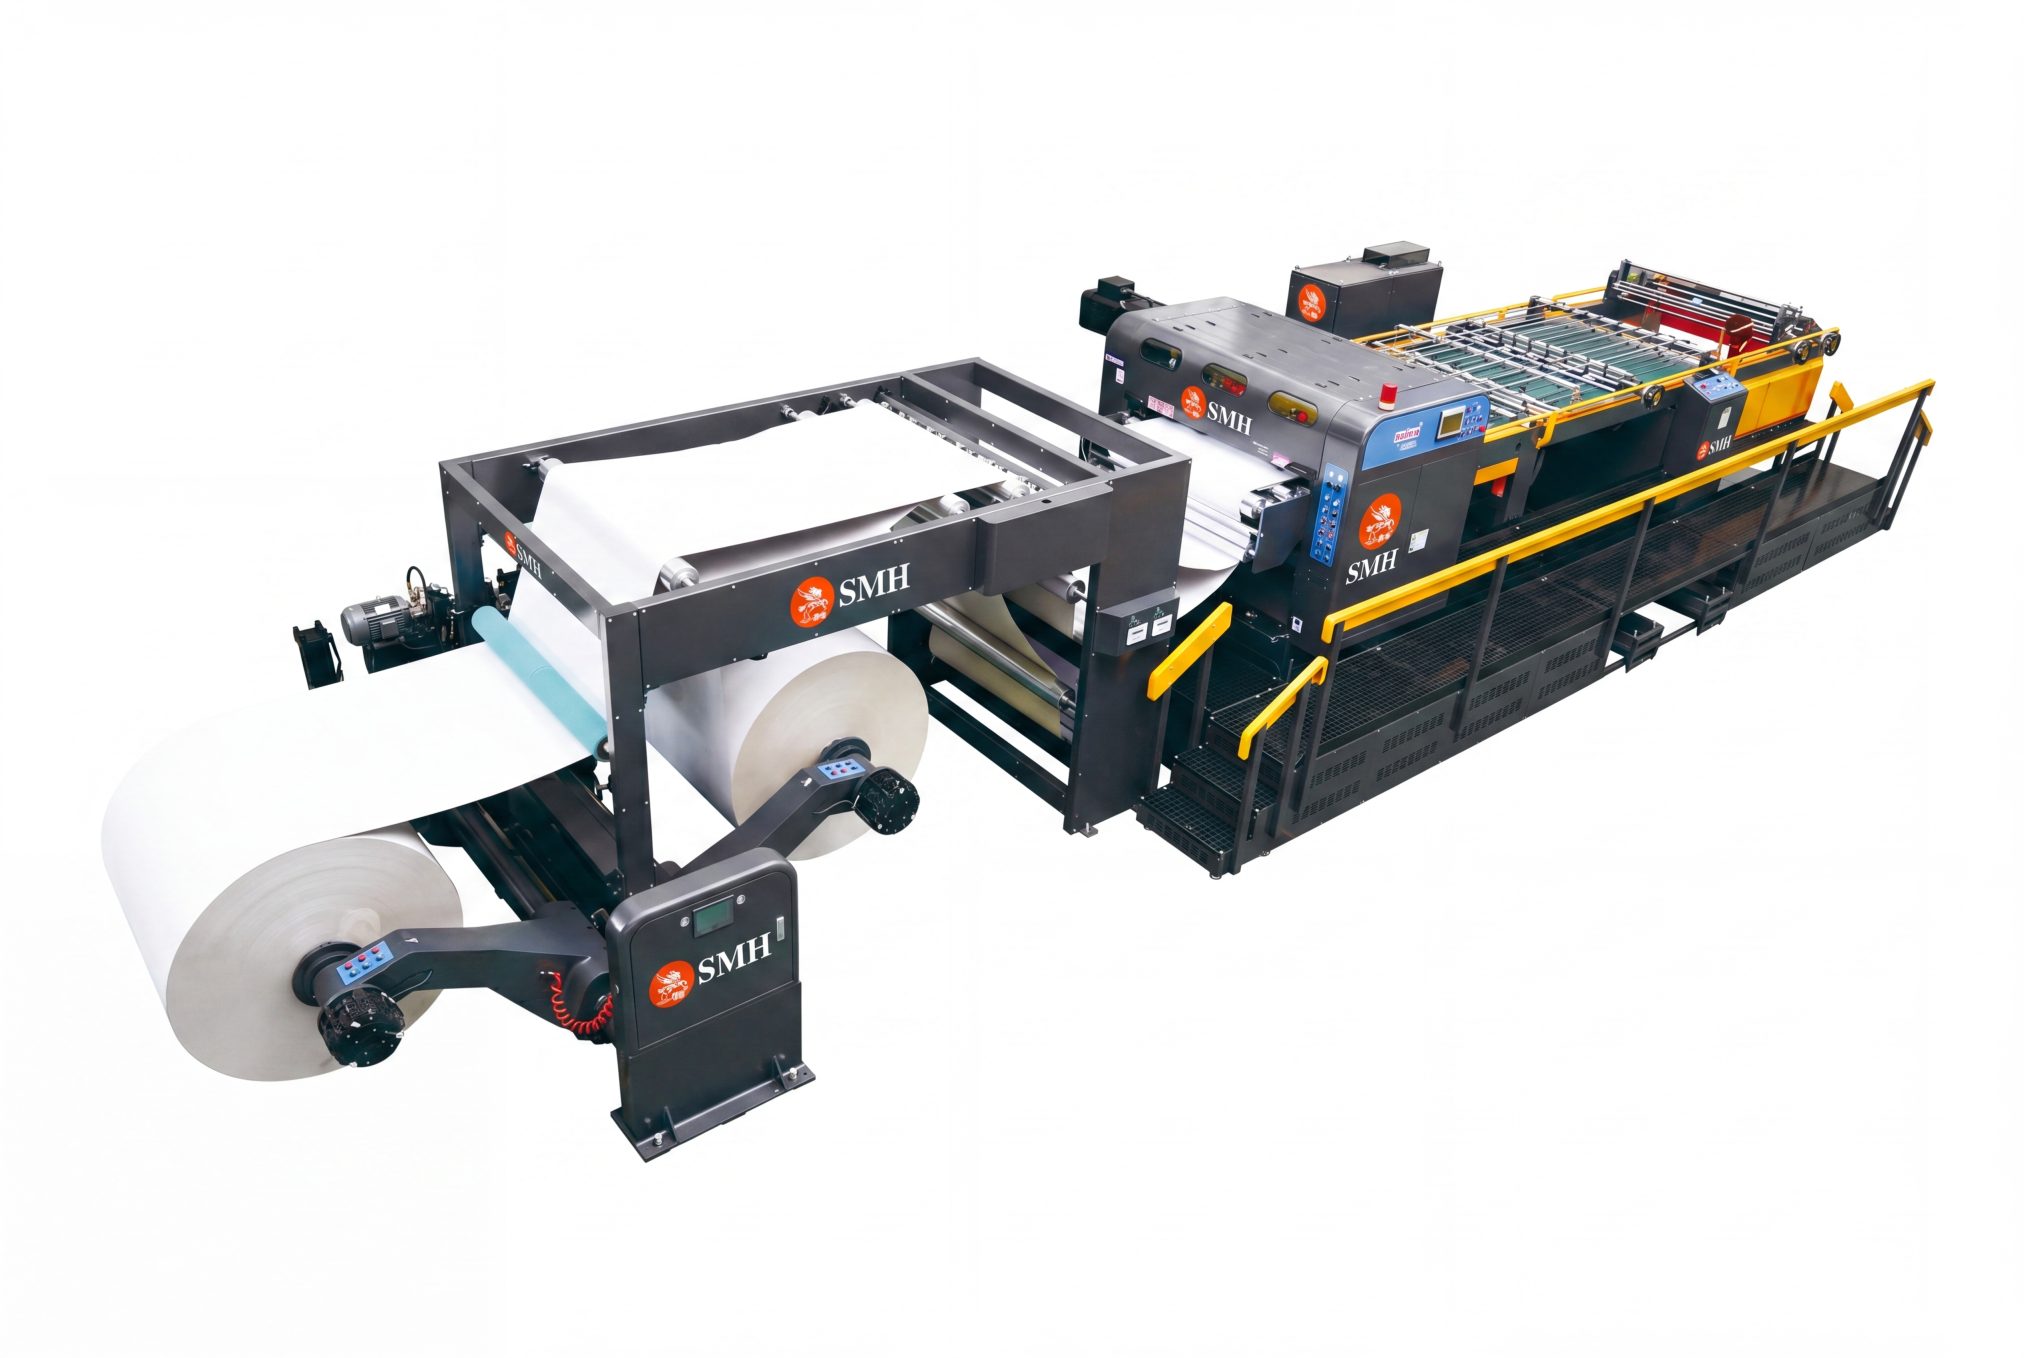
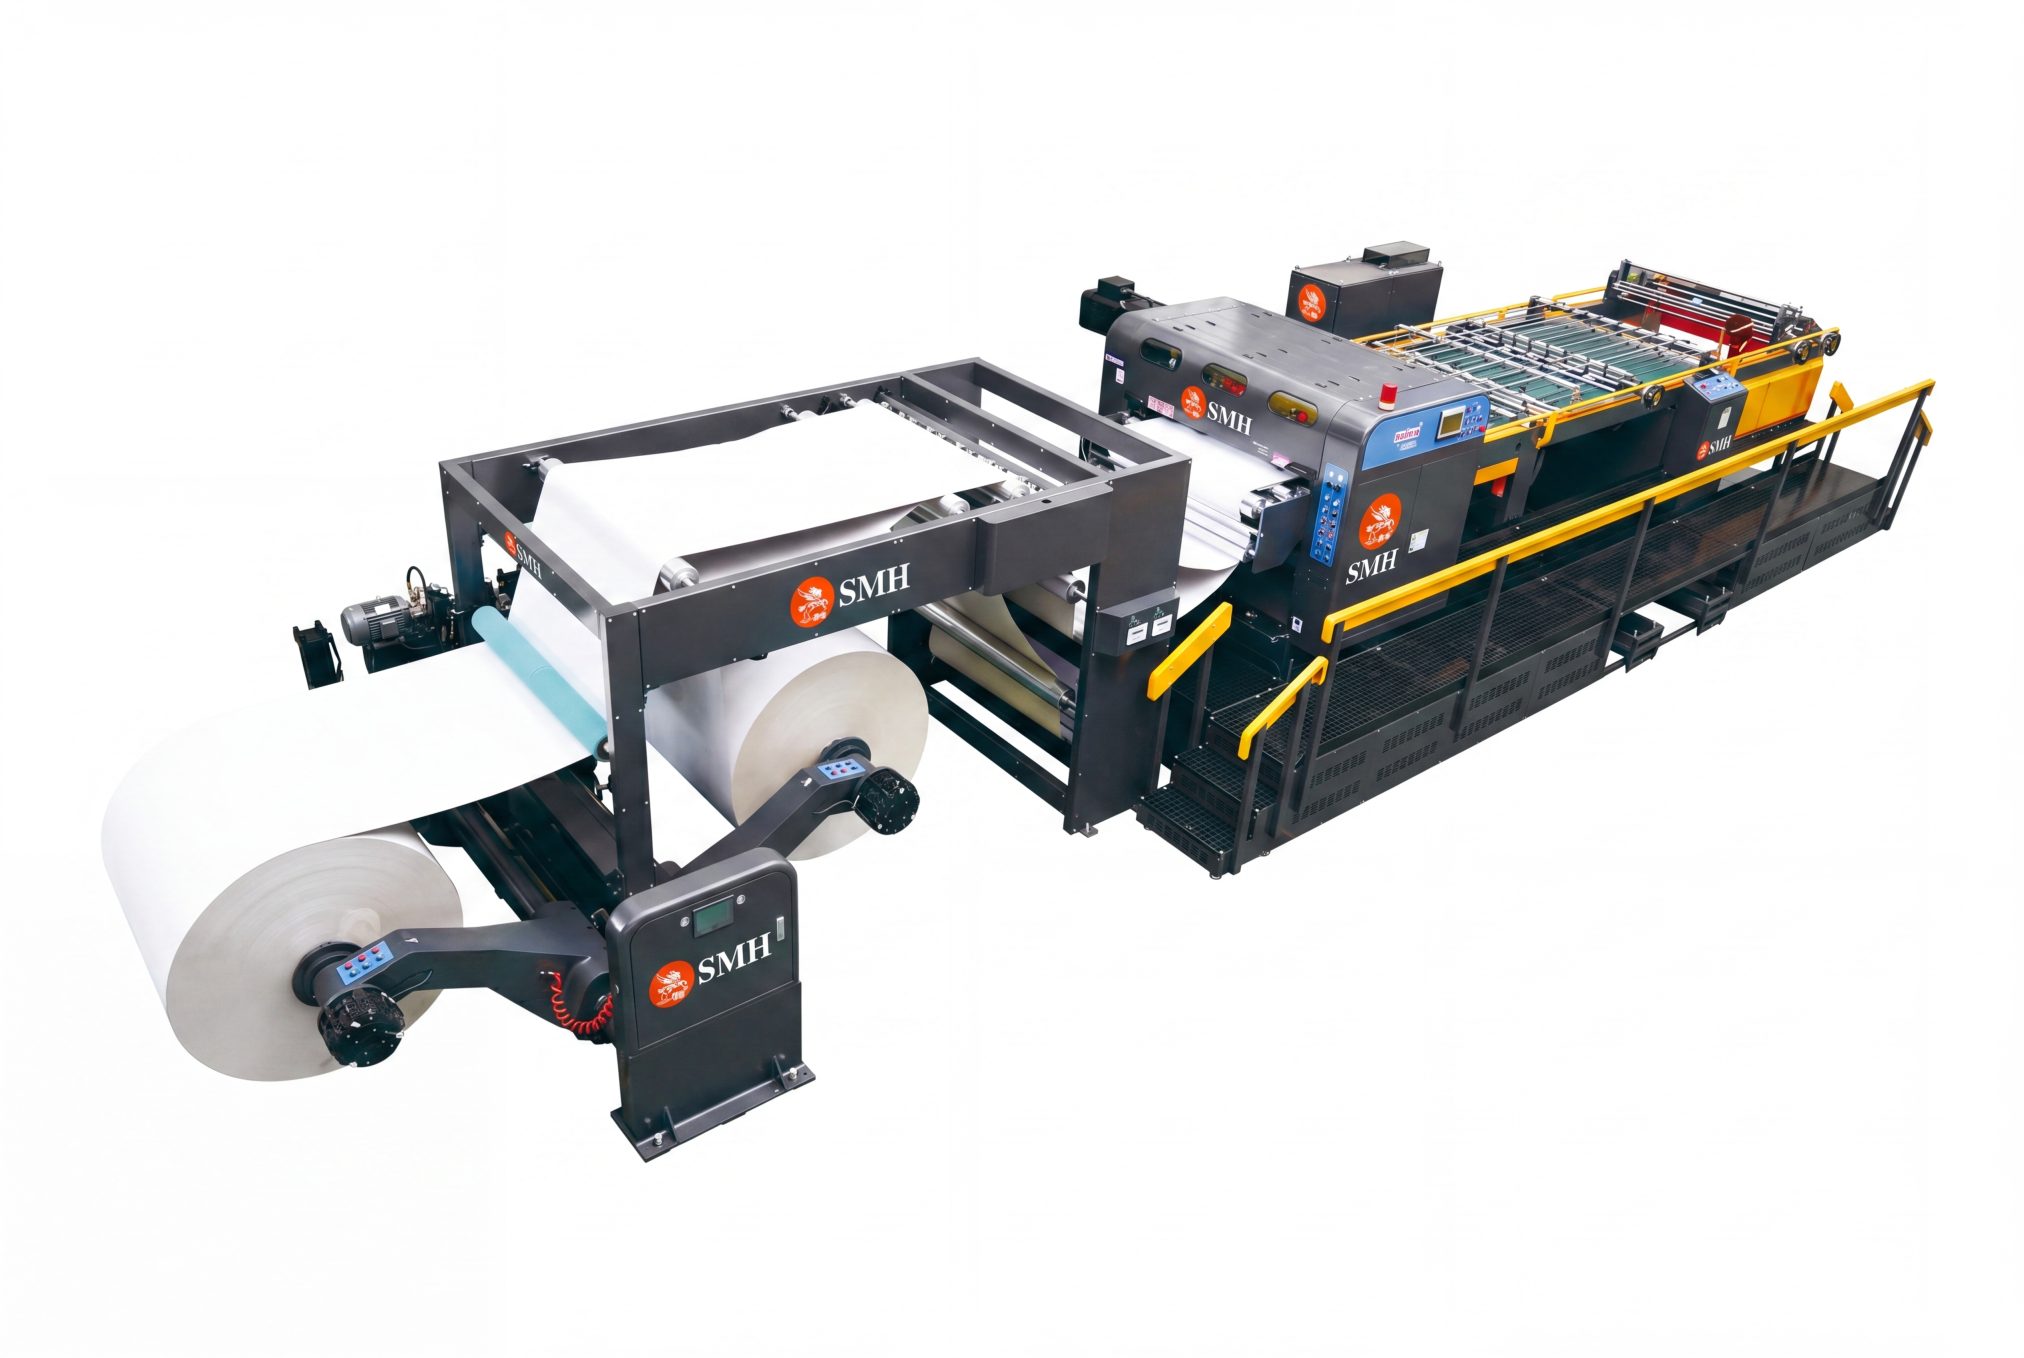
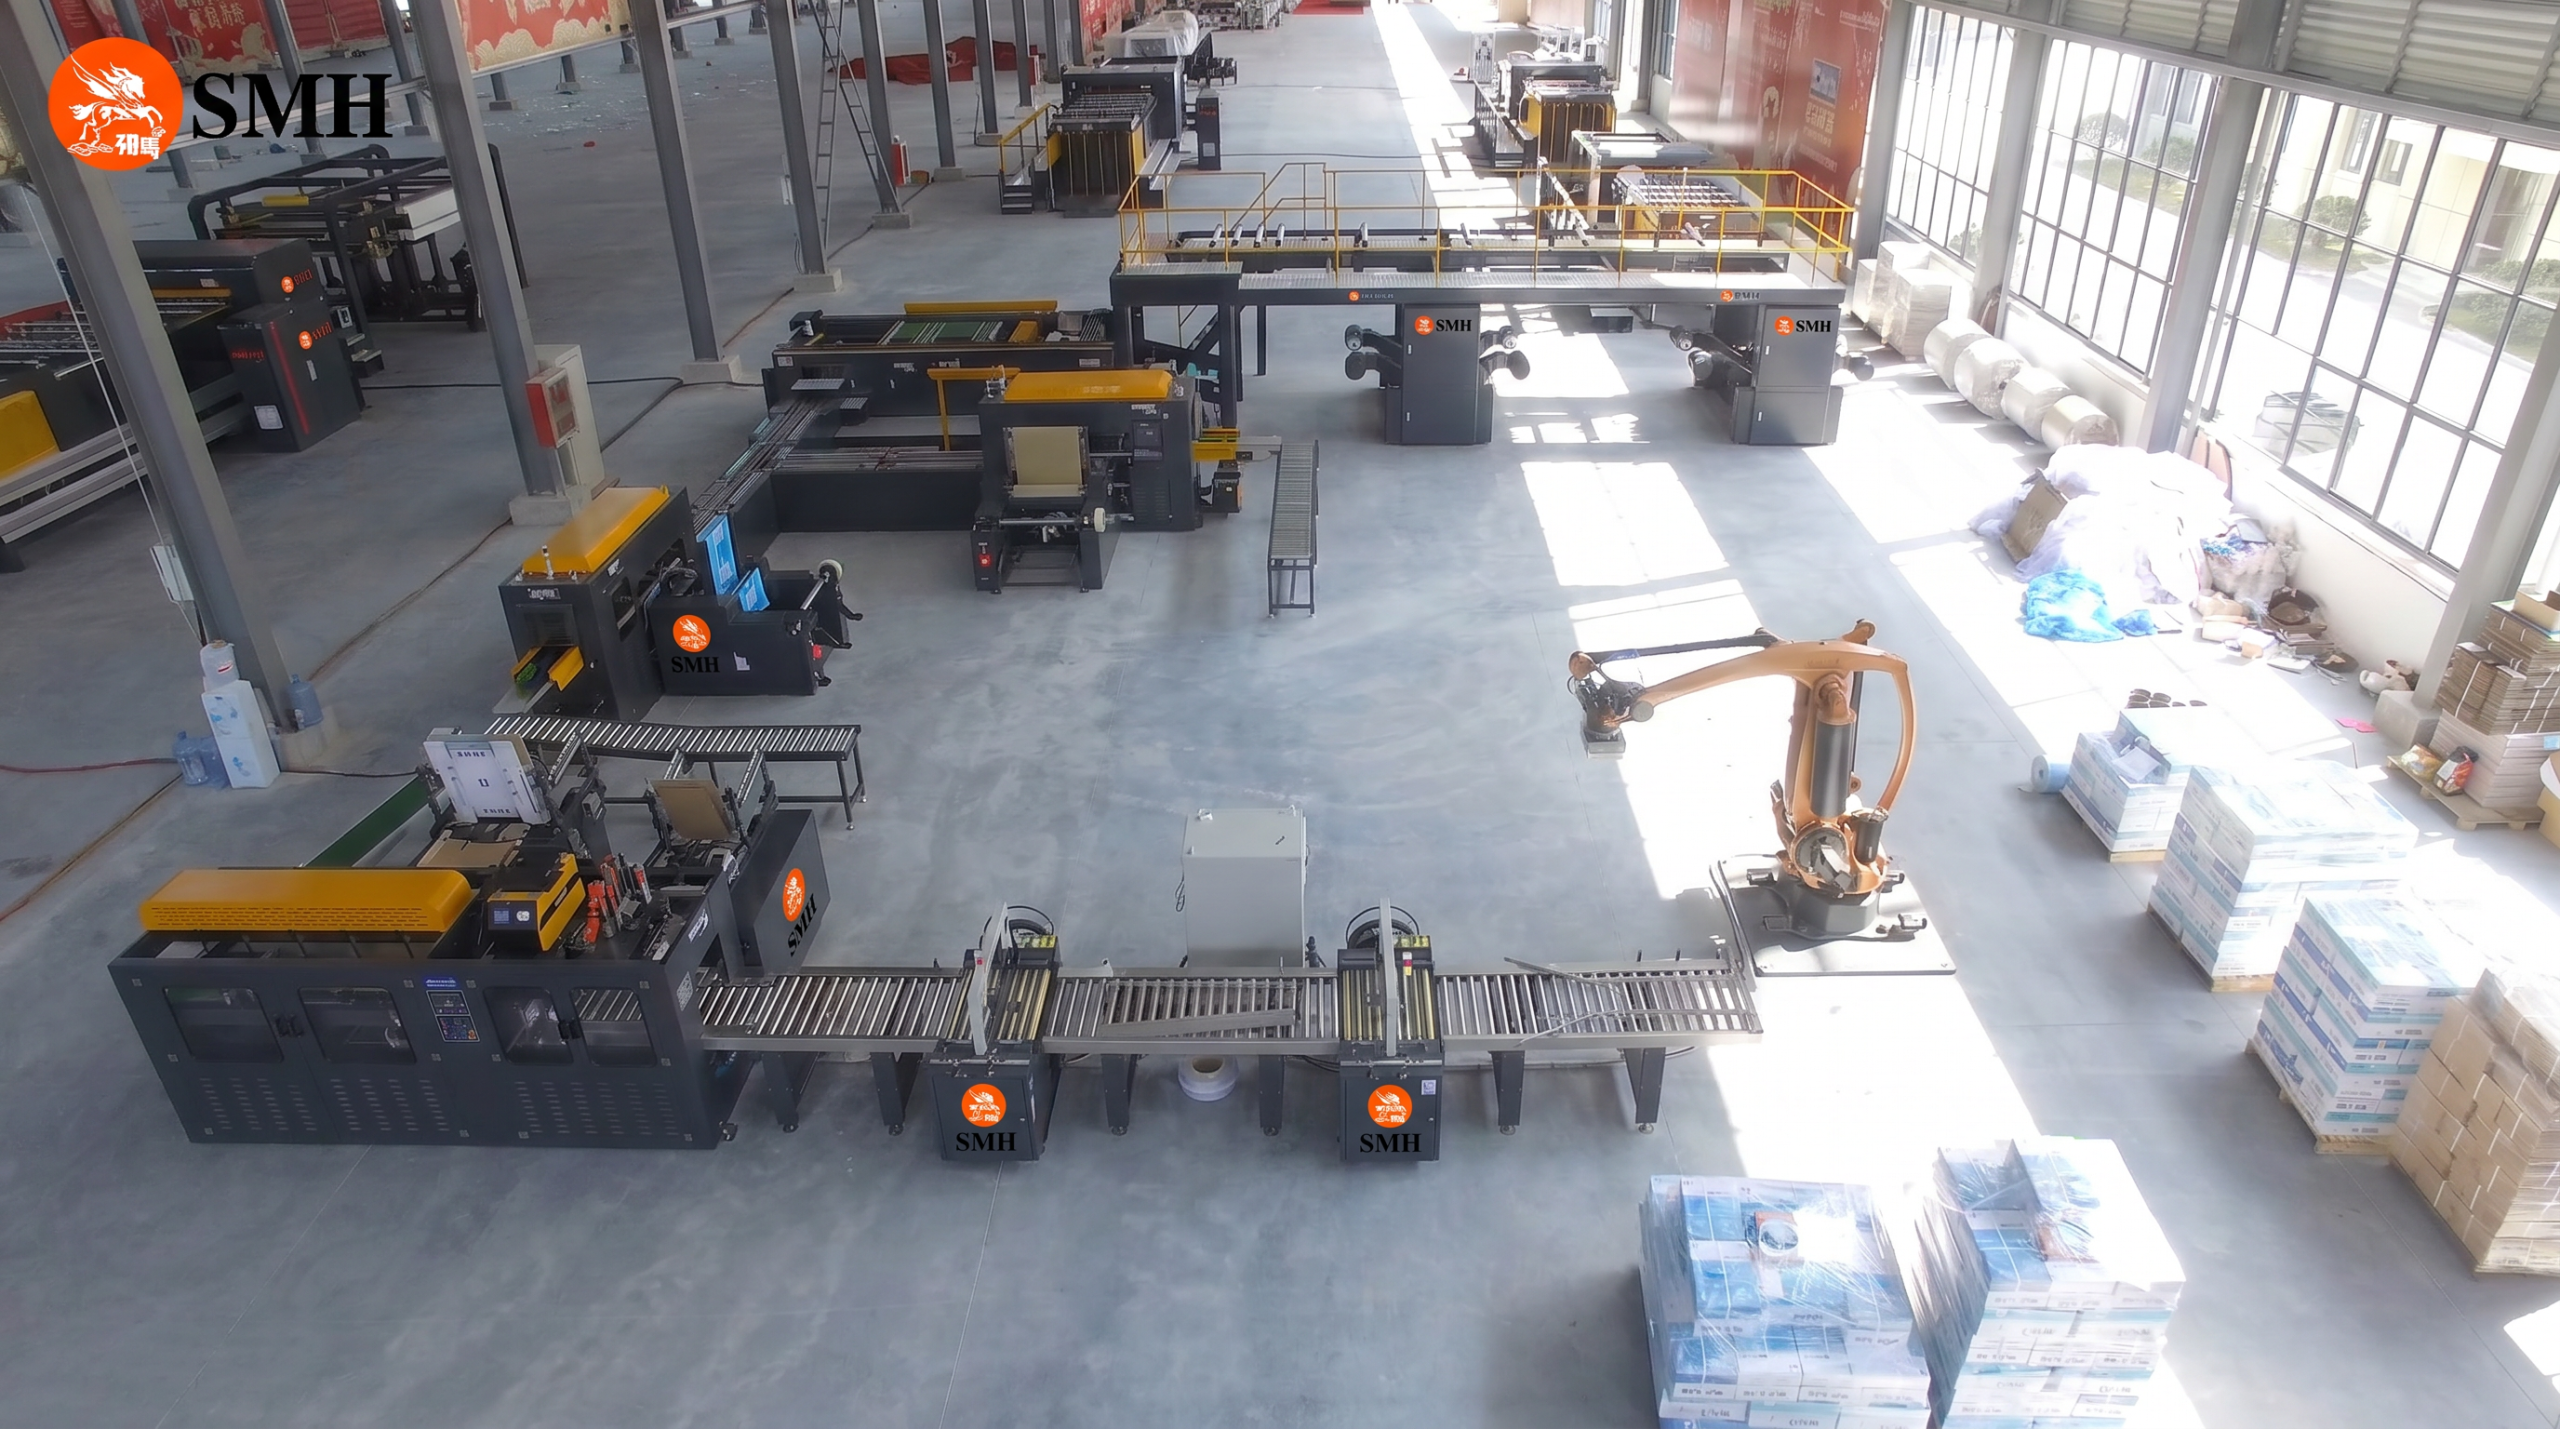
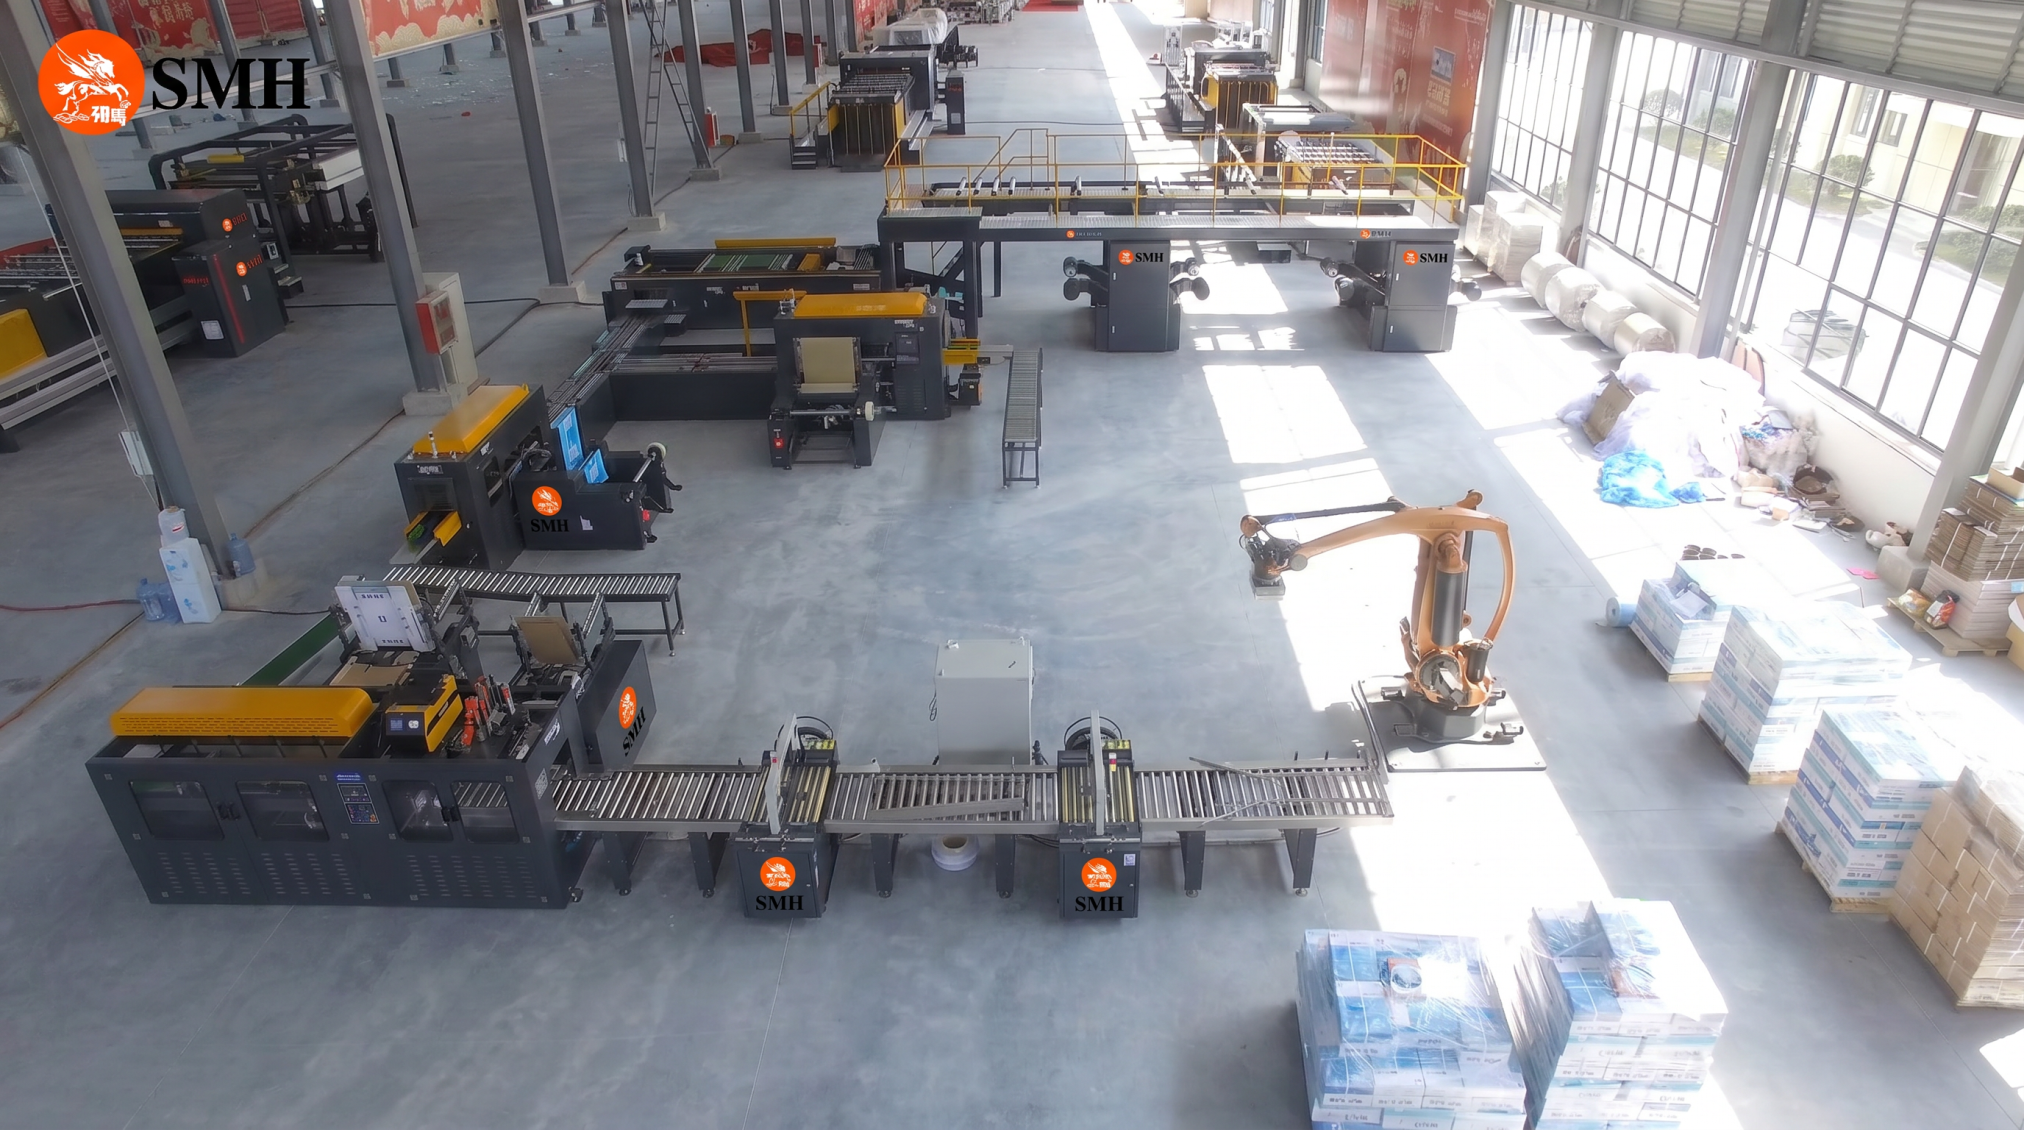
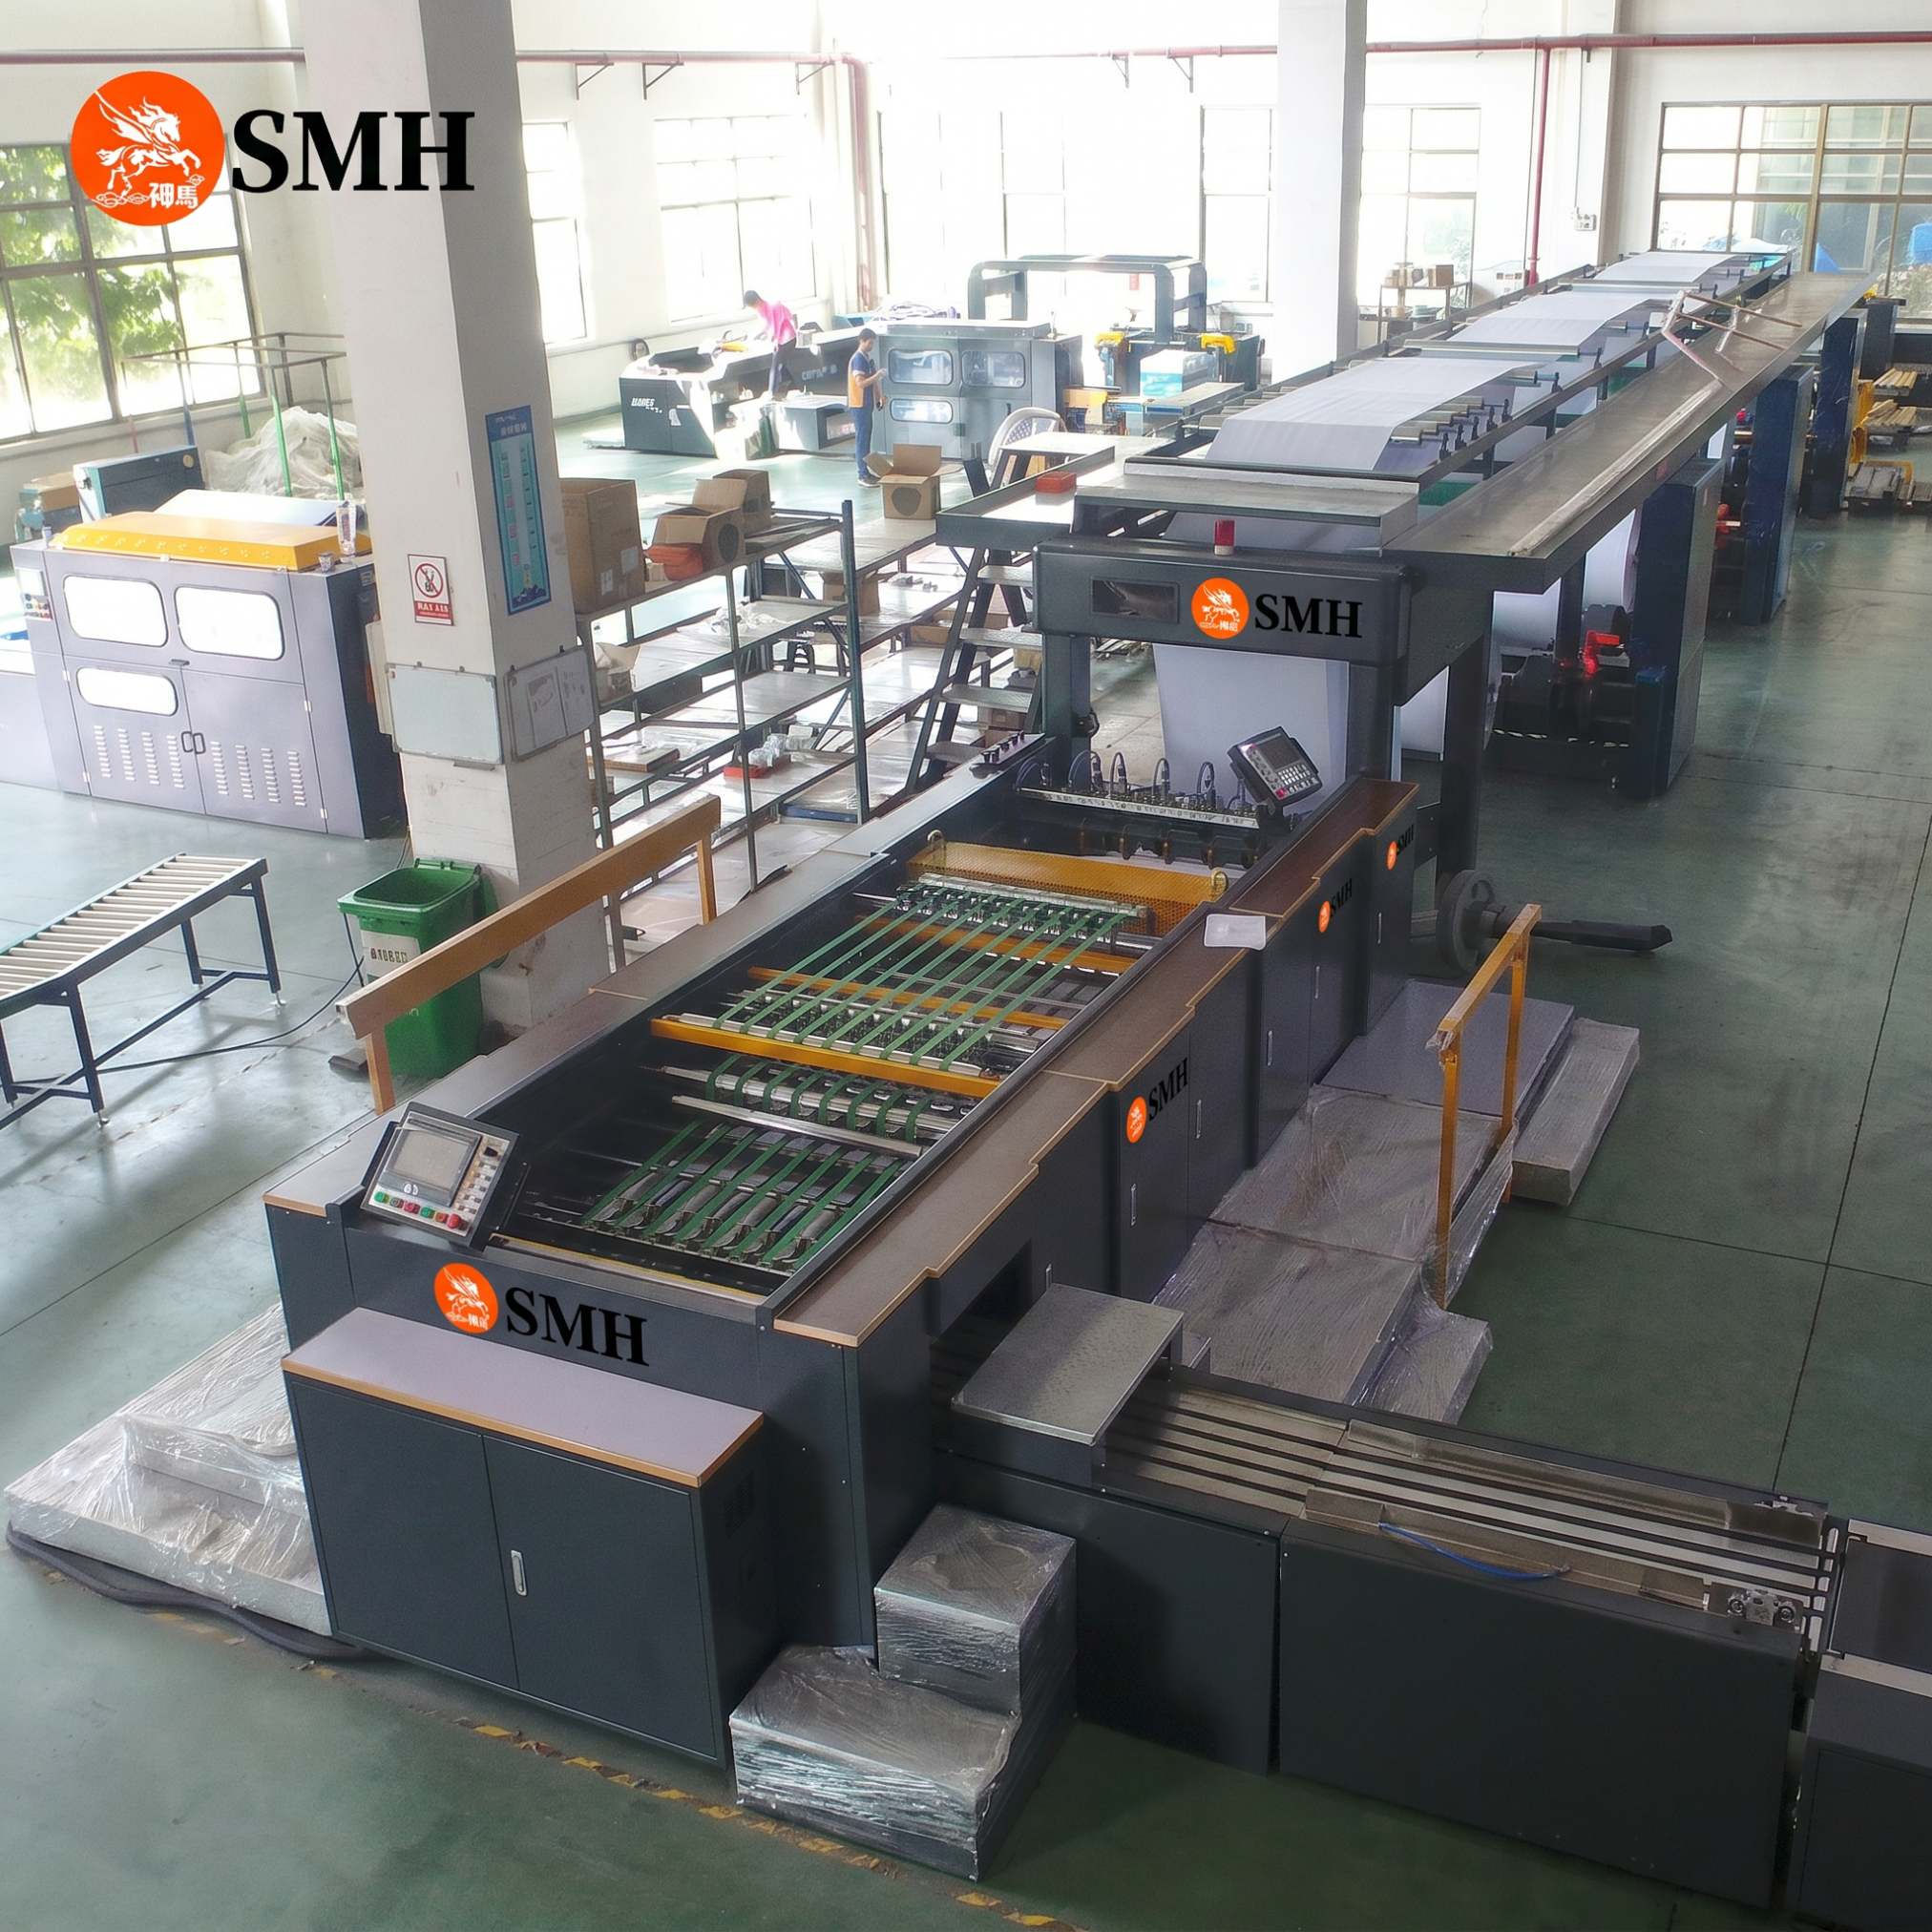
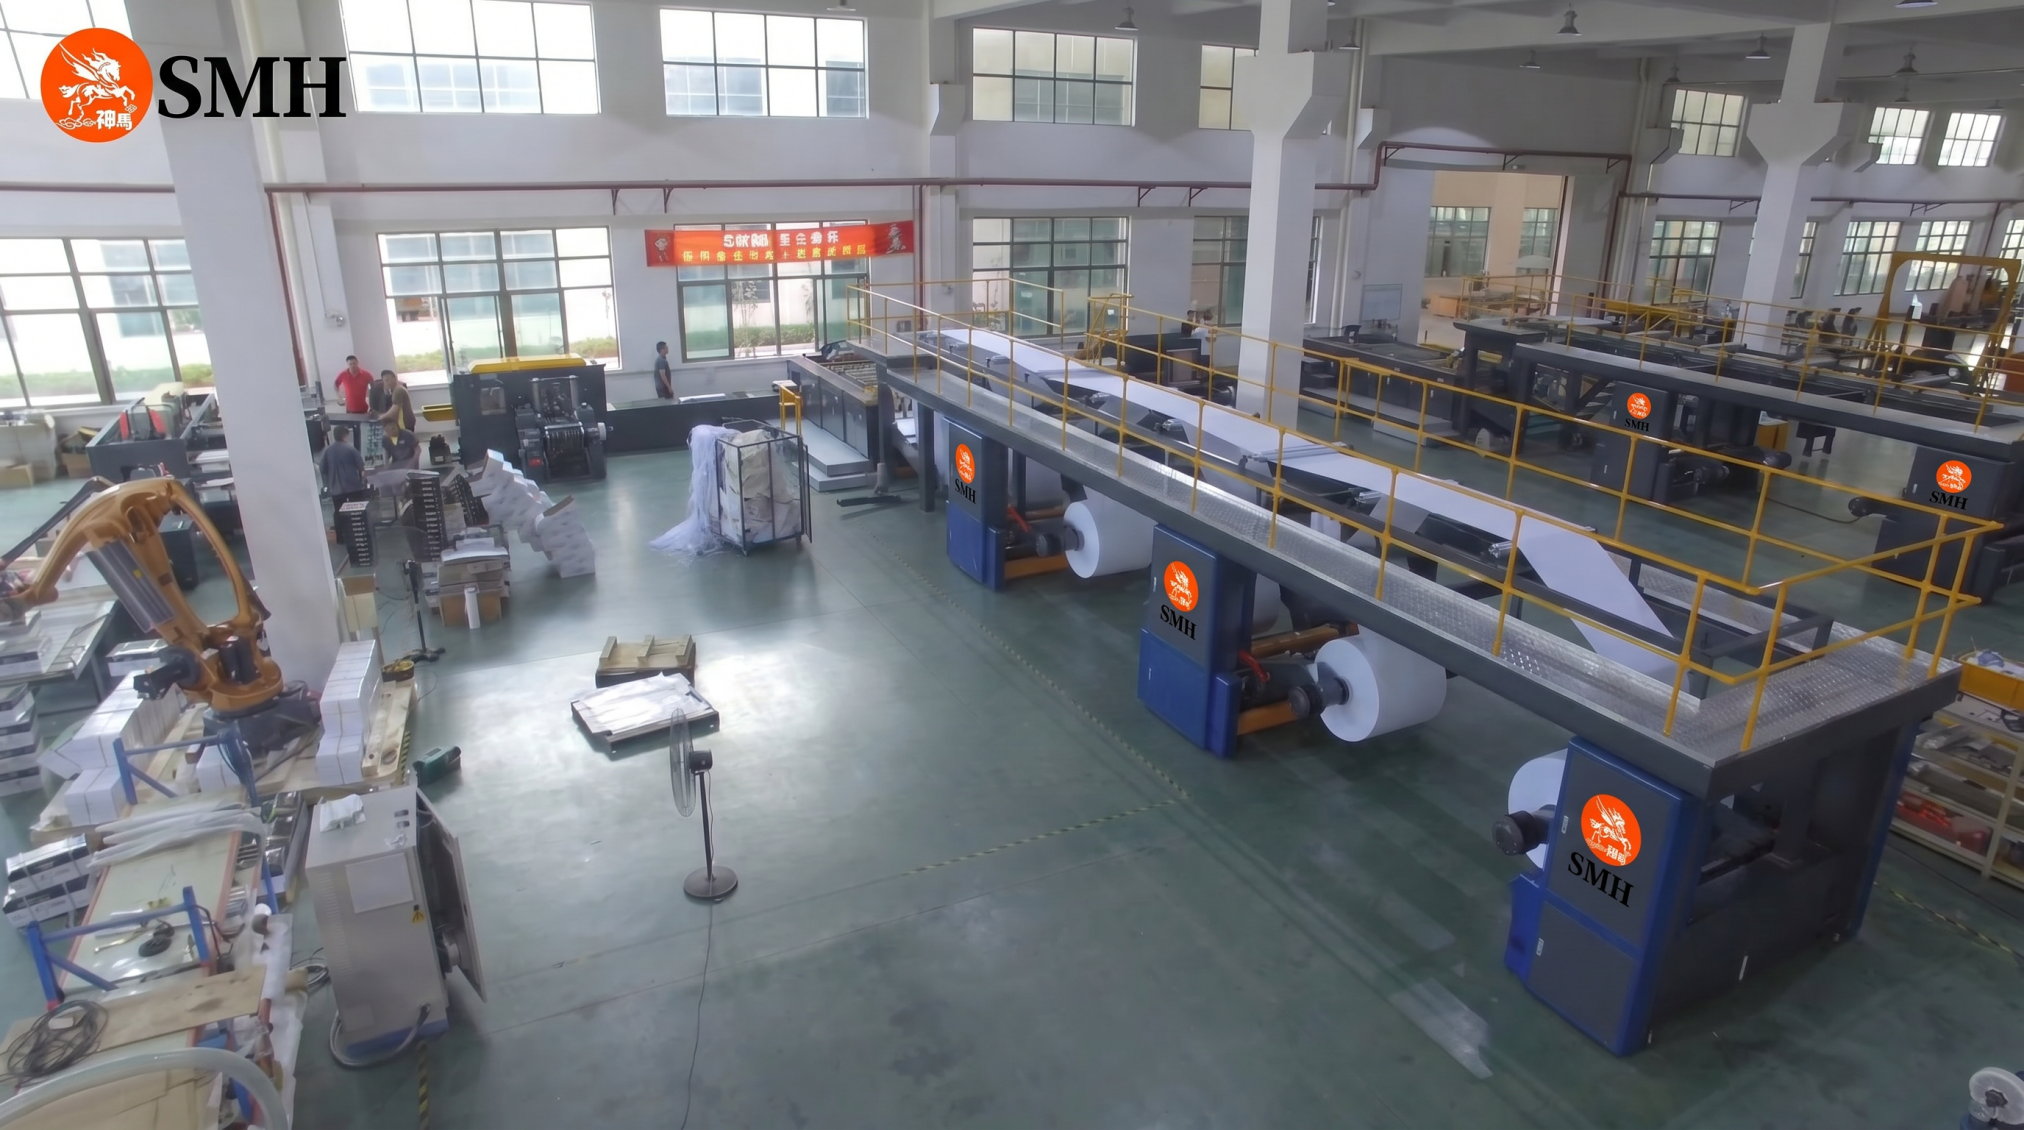
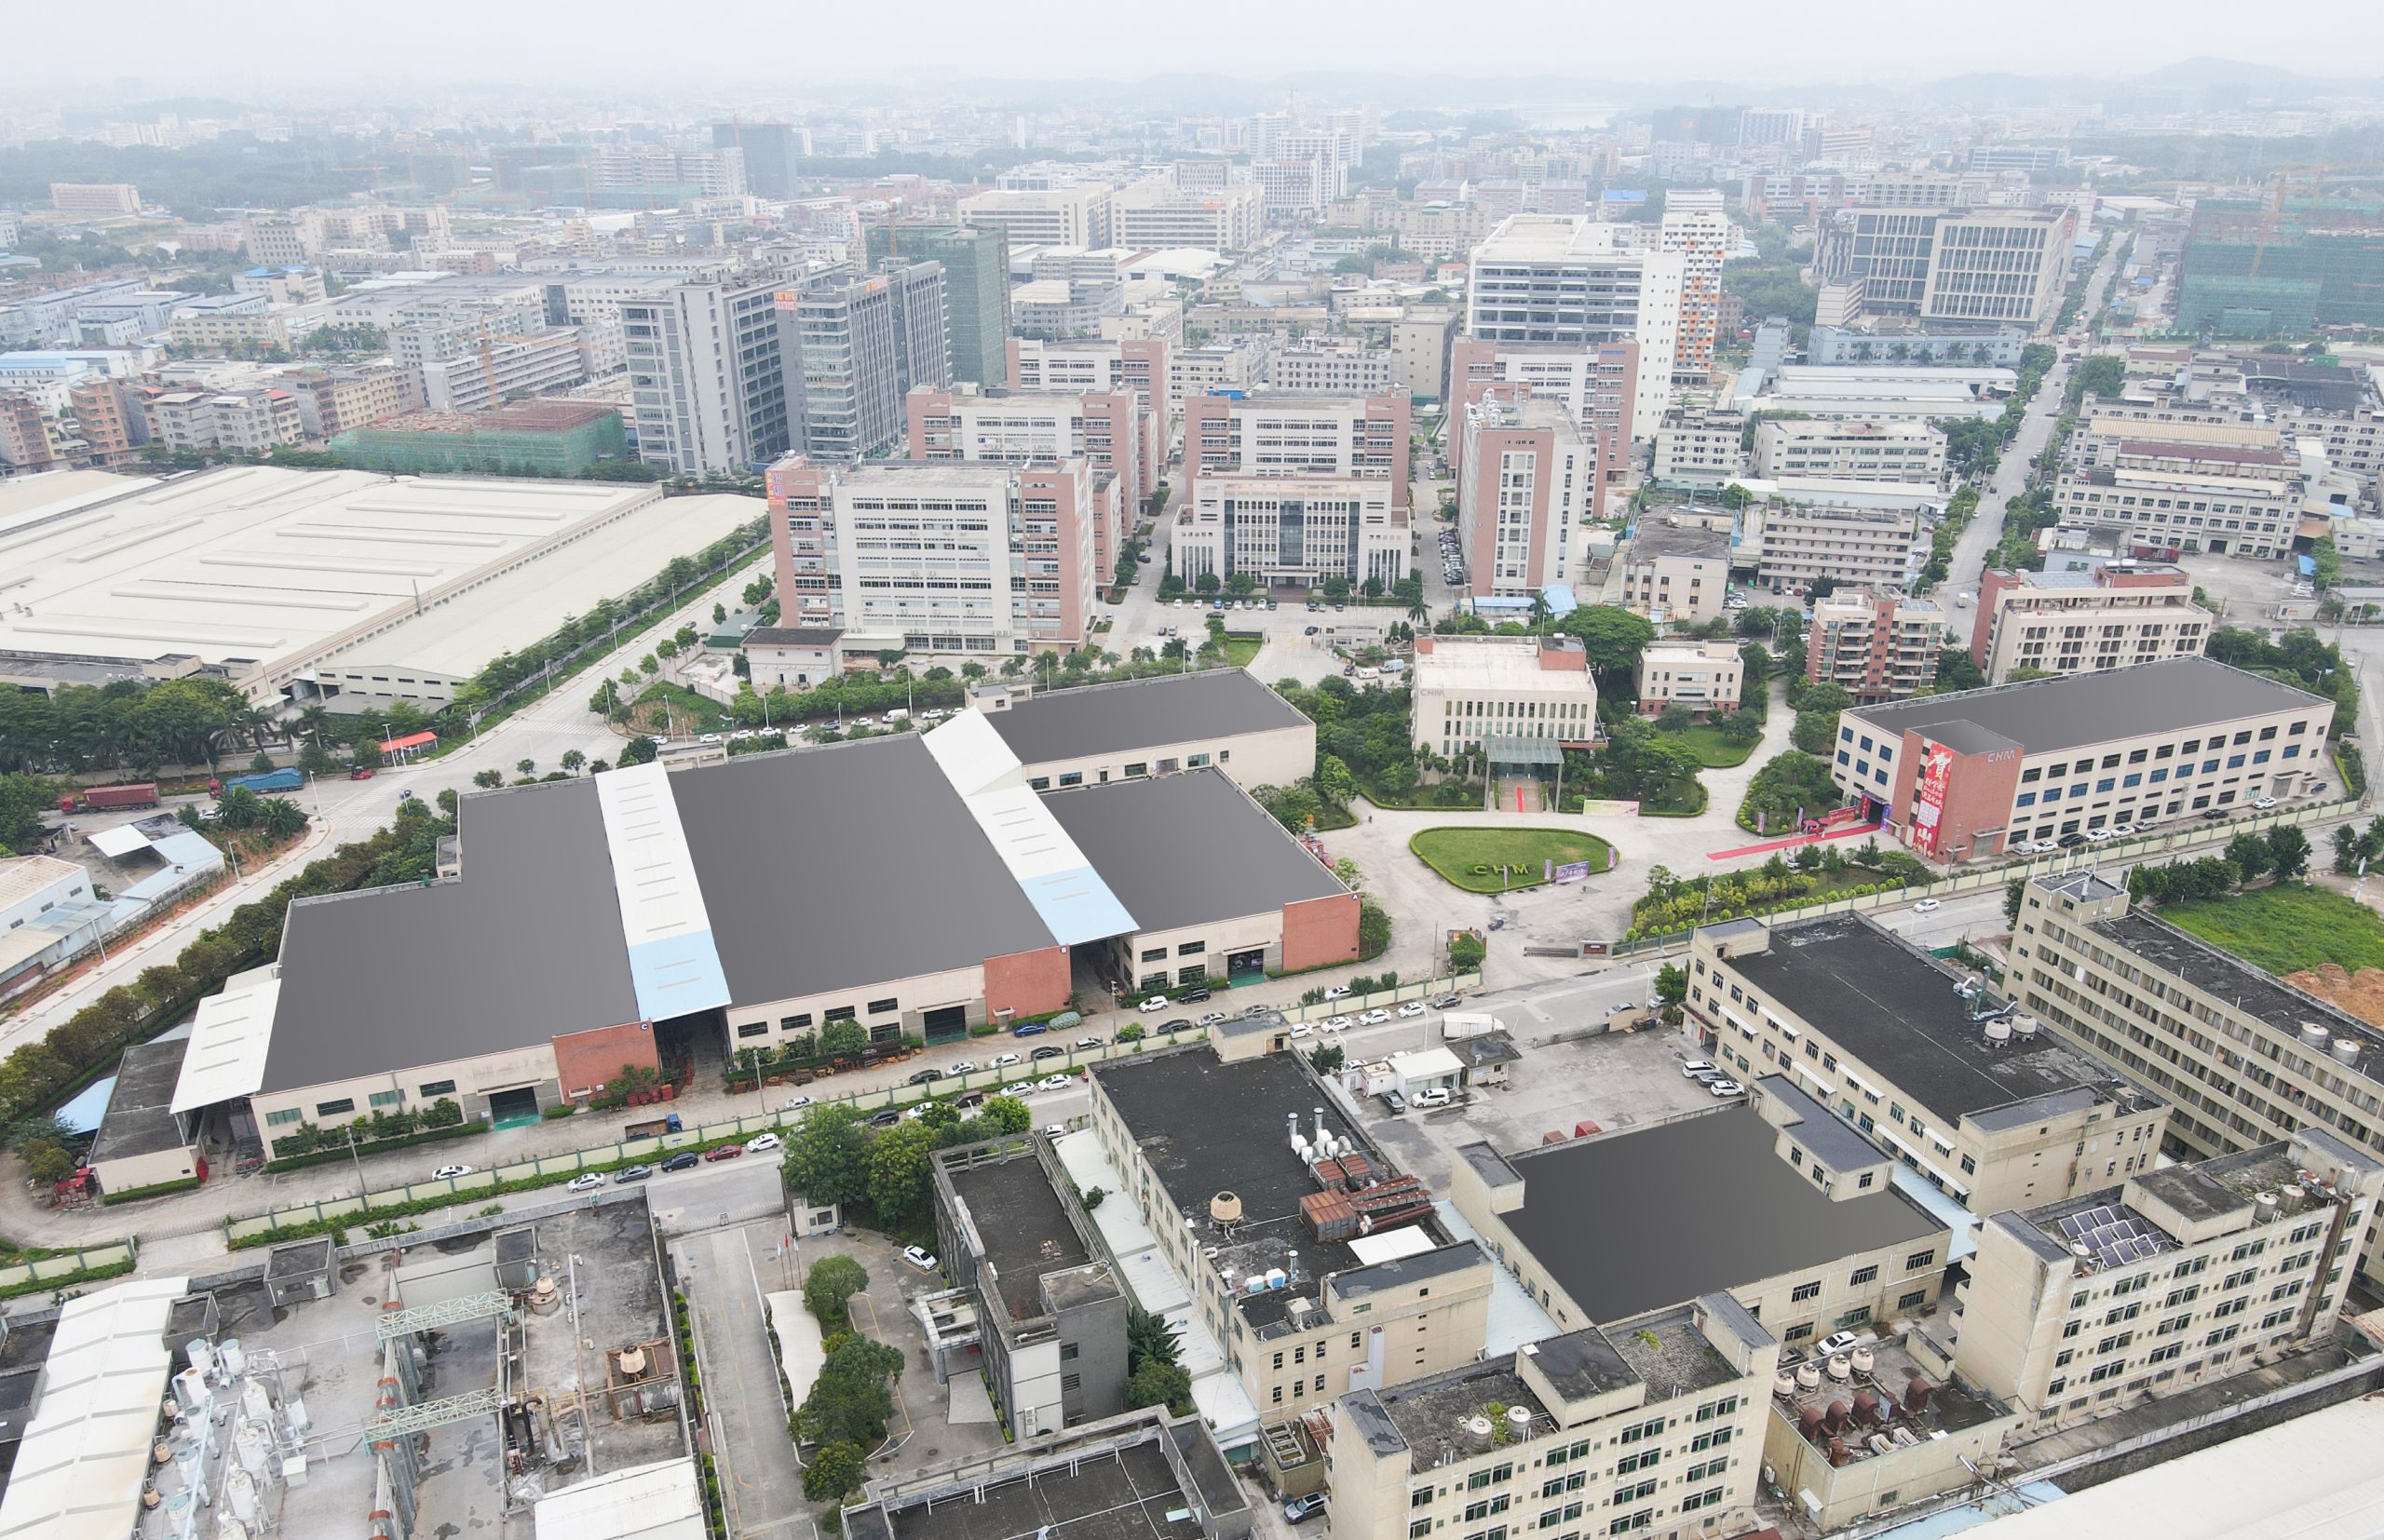
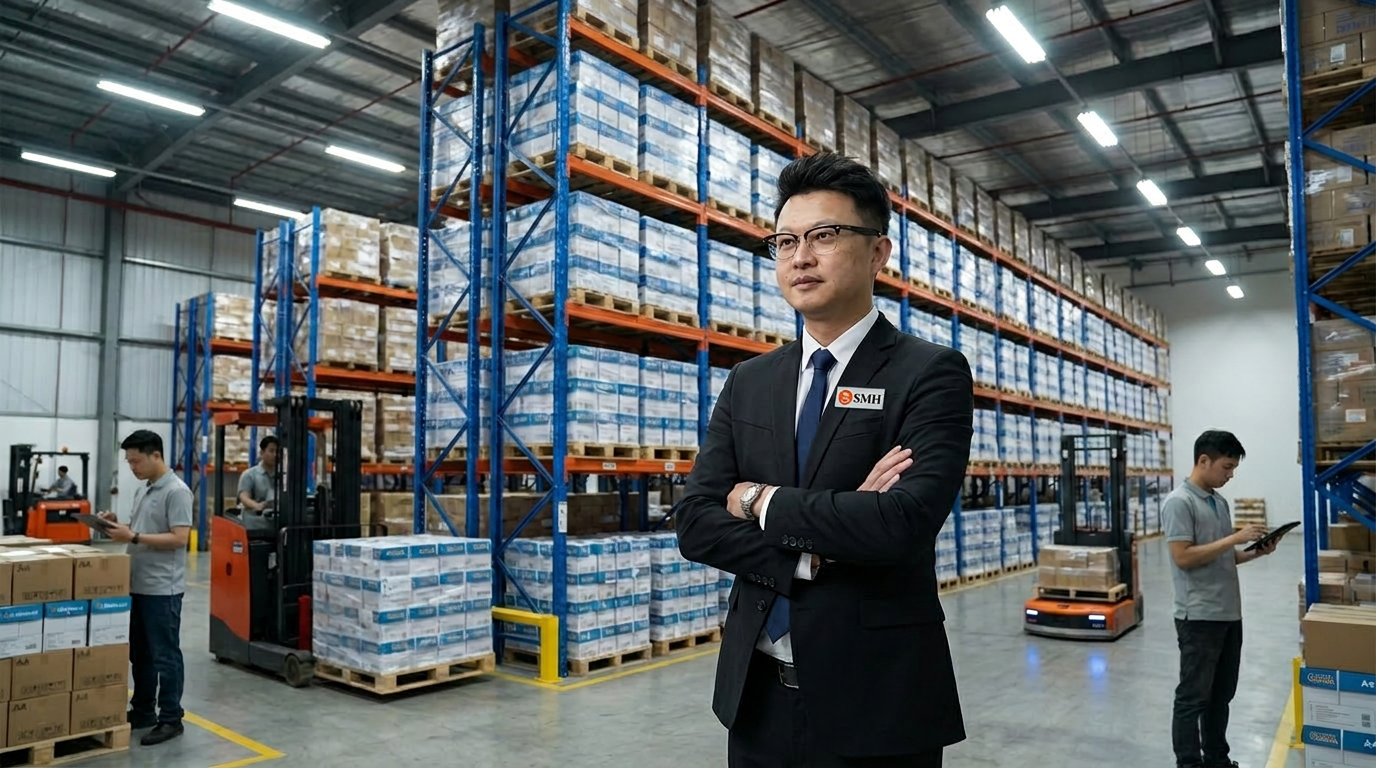
SMH operates a 140,000-square-meter manufacturing base dedicated to the production of paper sheeters, slitting machines, copy paper production lines, and automatic packaging systems. The facility integrates machining, welding, assembly, electrical integration, and machine testing into one complete manufacturing workflow.
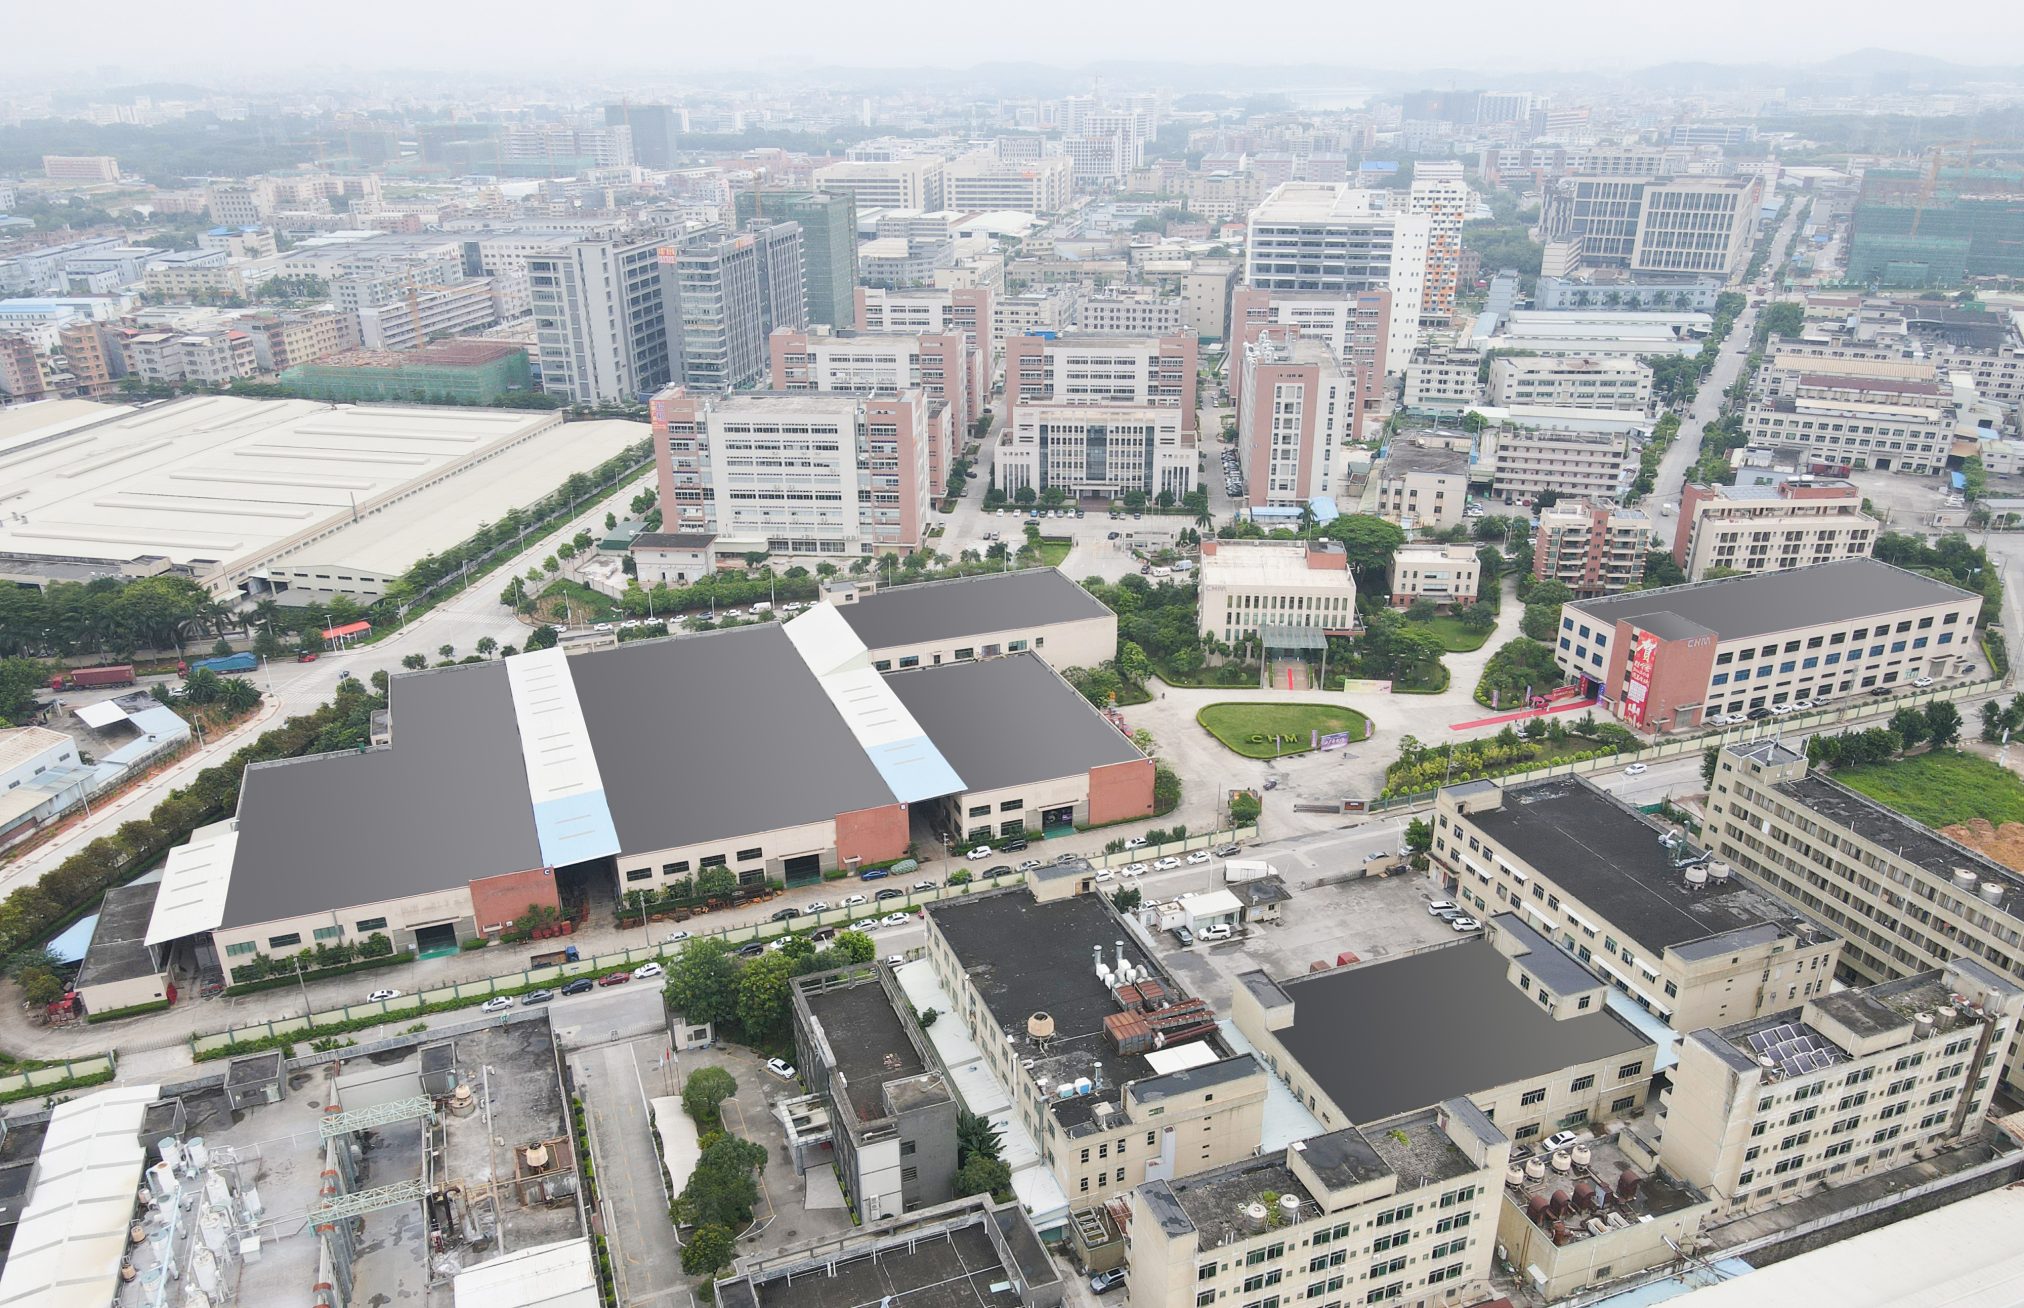
smh manufacture base

From Raw Materials to Complete Machine Assembly

Inside the SMH factory, large CNC machining centers process key machine components with strict dimensional control. Machine frames, rollers, knife holders, and transmission systems are manufactured according to high-precision standards to ensure stable operation during high-speed production.

After machining, components enter the assembly workshop where engineers install PLC control systems, servo motors, automatic tension control systems, and synchronization modules. Every machine is assembled according to standardized production procedures to maintain consistent quality.
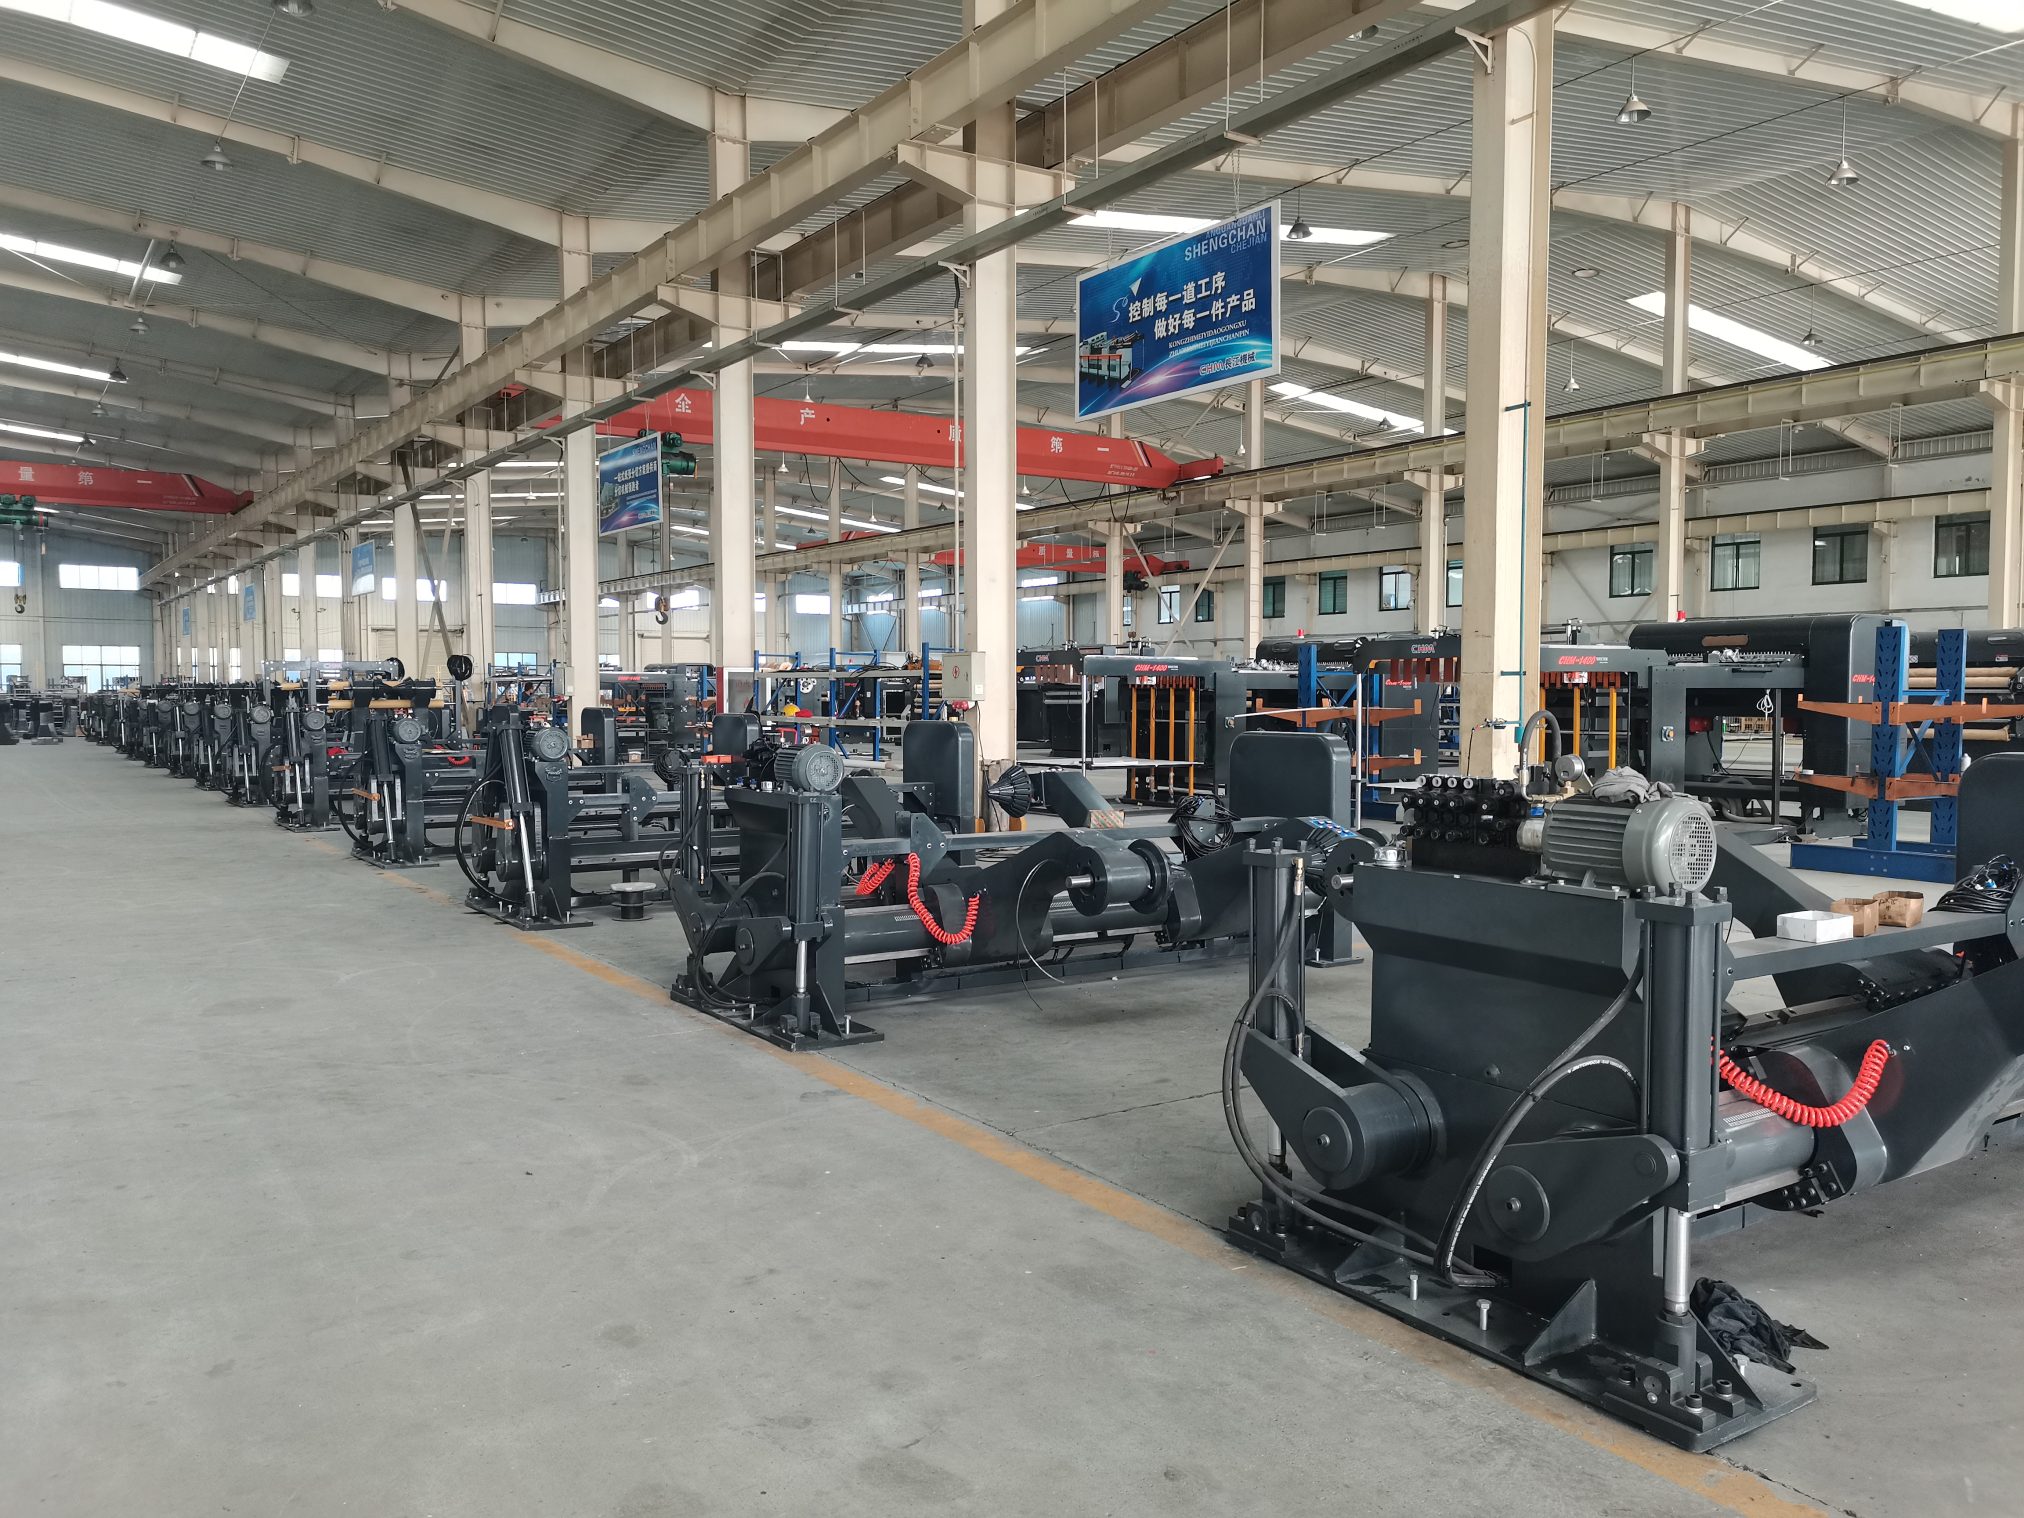
Strict Testing Before Delivery

Before shipment, each SMH machine undergoes complete testing under simulated production conditions. Engineers test cutting accuracy, tension stability, running speed, and automatic control performance.

Machines are adjusted according to different paper grades including copy paper, kraft paper, coated paper, cardboard, and thin paper materials. This helps customers reduce installation time and improve production efficiency after delivery.
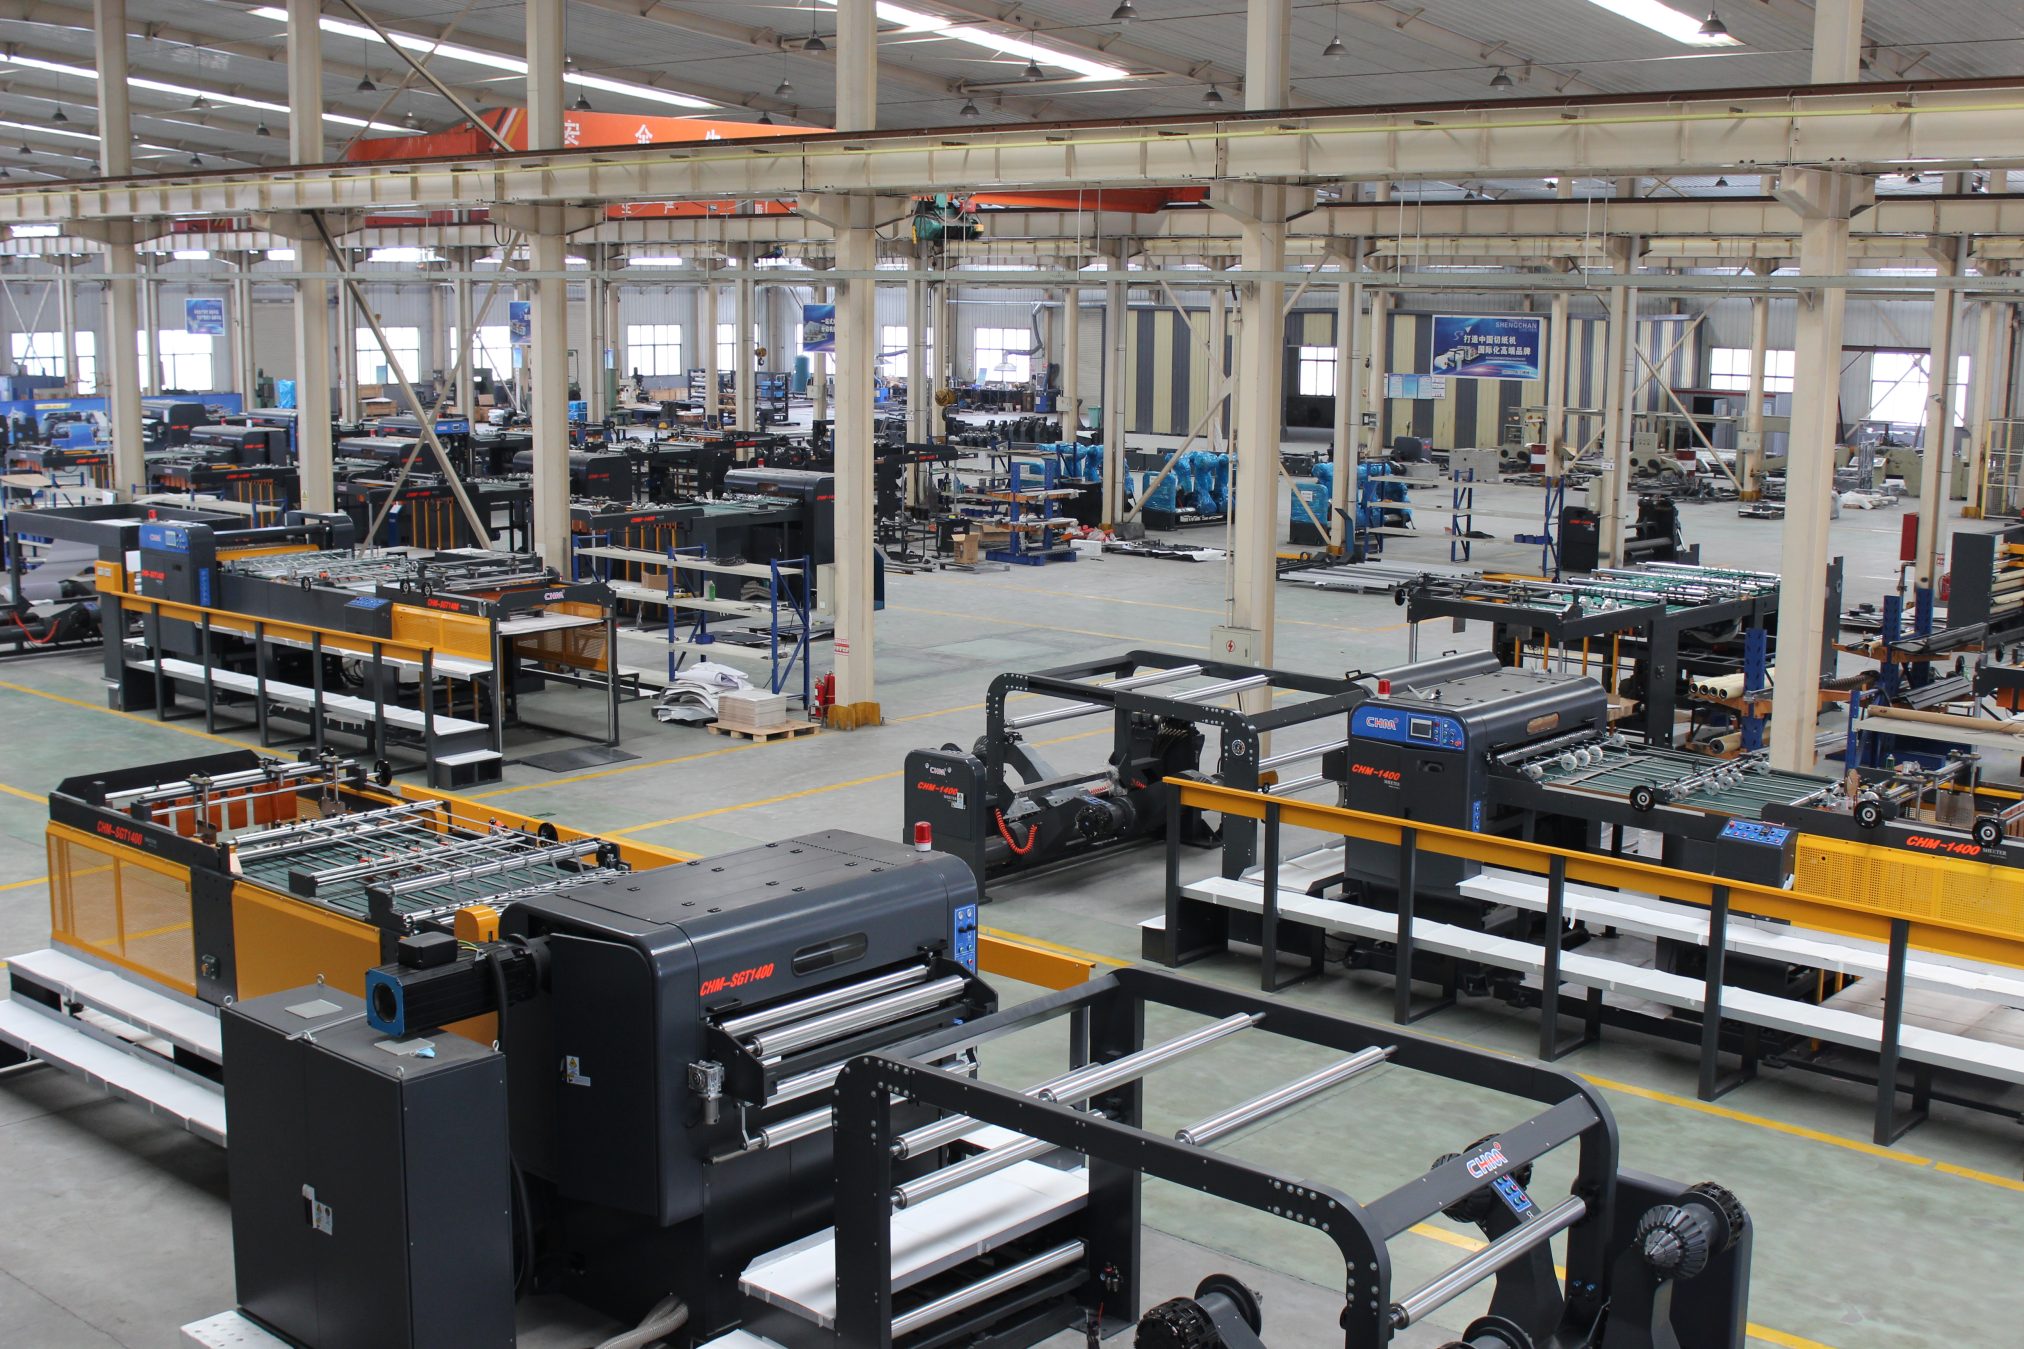
Supporting Global Paper Manufacturers

Today, SMH equipment has been exported to more than 80 countries and regions. From Asia to Europe and South America, SMH production lines continue supporting paper mills, printing factories, and packaging companies with reliable automation solutions.

As global demand for efficient paper converting equipment grows, SMH continues investing in manufacturing technology, engineering development, and intelligent automation systems to provide stable and efficient solutions for customers worldwide.
Why High-Speed Slitting Machines Need Better Stability

High Speed Alone Does Not Guarantee Higher Output

warehouse
warehouse

Many factories want faster production. That is normal.

But after increasing machine speed, some lines actually produce more waste instead of more good products.

The paper starts drifting. Stacking becomes messy. Edge quality changes. Operators begin slowing the line down again.

This happens because high-speed production magnifies small mechanical problems.

Small Errors Become Bigger at High Speed

At low speed, slight tension changes may not be obvious. Minor vibration may also go unnoticed.

At high speed, those same problems become much more serious.

A tiny knife vibration can affect cutting accuracy. Small tension fluctuations can change sheet length. Slight roller slipping can cause feeding instability.

The faster the line runs, the less room there is for error.

That is why stable high-speed production depends heavily on machine rigidity and synchronized control.

The Machine Structure Matters More Than Operators Think

In many factories, operators try solving instability by adjusting parameters repeatedly. Sometimes they change tension. Sometimes they reduce speed. Sometimes they increase knife pressure.

But if the machine structure itself is unstable, adjustments only provide temporary improvement.

A stable high-speed slitting machine usually includes:

  • rigid machine frame
  • stable roller system
  • synchronized servo control
  • accurate guiding system
  • consistent tension control

Without these conditions, running faster only increases instability.

Why Double Knife Systems Run More Smoothly

double rotary sheeter

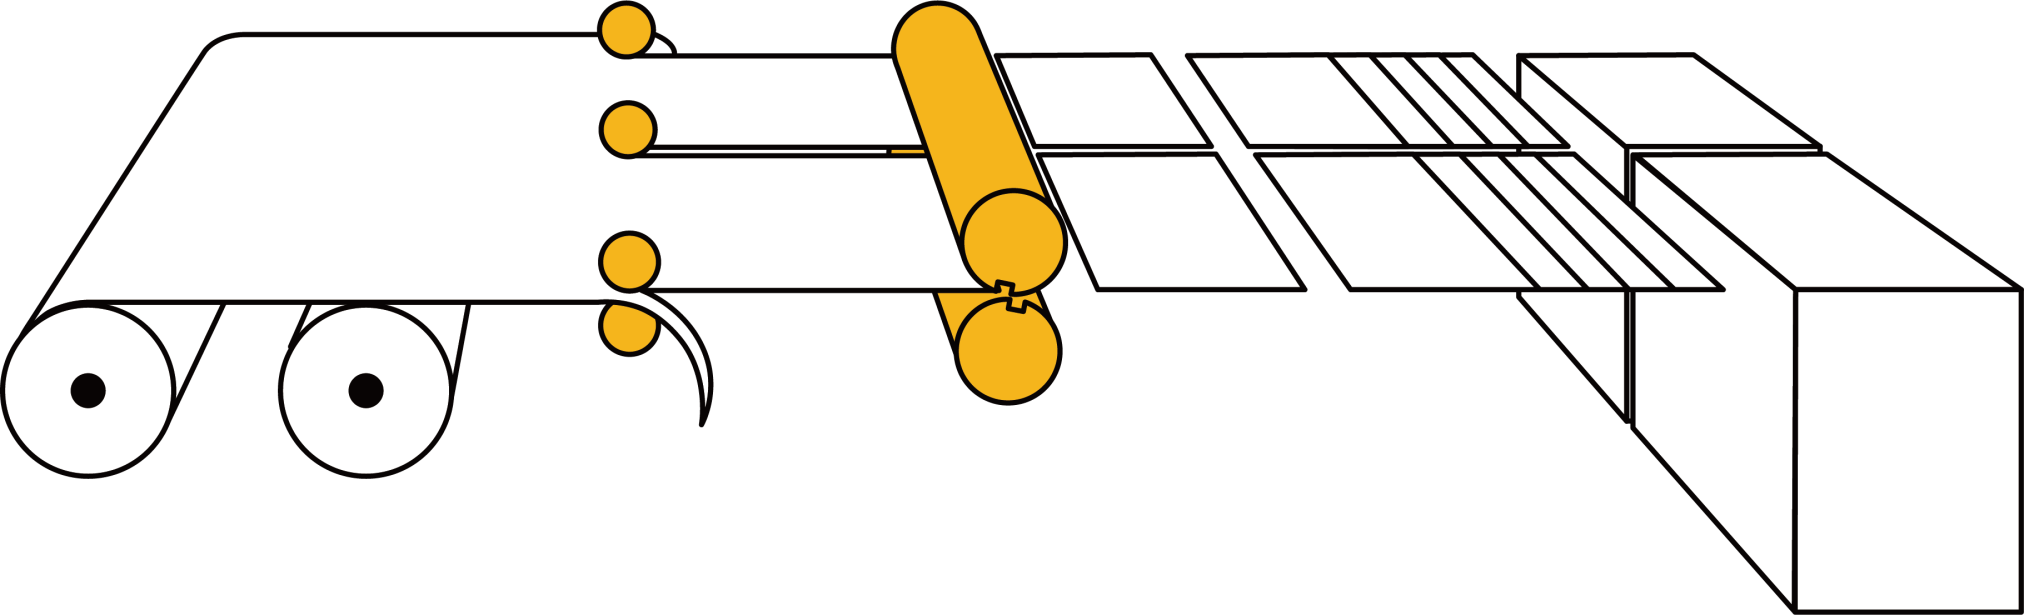
Double knife systems are widely used in high-speed applications because the cutting process stays more balanced.

Both knife rollers rotate synchronously. The material receives cutting force from both sides. The paper movement becomes smoother.

Compared with impact-style cutting, vibration is lower. That helps maintain edge quality during long production runs.

This is especially important in:

  • coated paper production
  • packaging board converting
  • high GSM paper processing
  • large-volume paper mills

Stable Production Is More Valuable Than Peak Speed

In real factory operation, customers care more about consistent production than temporary peak speed.

A line that runs steadily for hours is usually more profitable than a line that reaches very high speed but stops constantly.

That is why experienced factories focus on:

  • stable output
  • lower waste
  • repeatable quality
  • reduced operator intervention

The real goal is not simply running fast. It is running fast without losing control.

Why Thick Paper Produces Burrs During Slitting

Burr Problems Usually Start When Material Changes

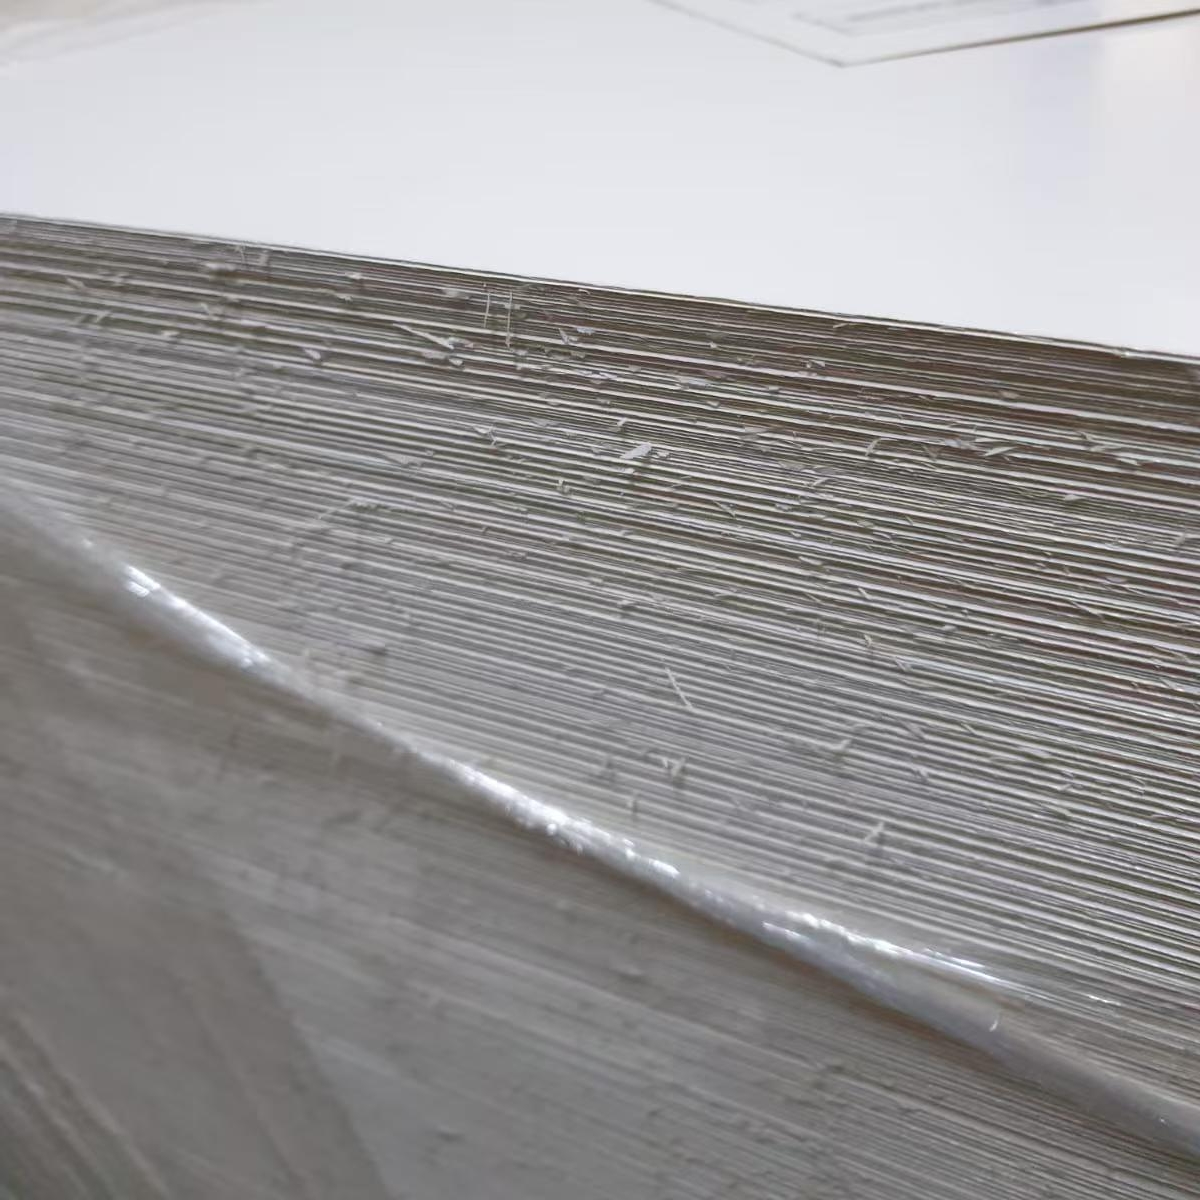
Edge of the paper
Edge of the paper

A production line may run perfectly with thin paper. Then one day the factory switches to heavier board. Suddenly the edge quality changes.

Paper dust increases. Small burrs appear. Sometimes the cut edge even feels rough by hand.

Many operators first suspect the knife. But in real production, the knife is often only part of the reason.

The bigger issue is that thick paper behaves completely differently during cutting.

Thick Paper Needs Different Cutting Force

thin paper
thin paper

Thin paper is flexible. It separates more easily during slitting.

Heavy board is different. The material is stiffer. The cutting resistance is much higher.

If the machine still uses impact-style cutting, the pressure concentrates on one side of the sheet. That creates stress around the cutting point.

At lower speed, the issue may not look serious. At higher speed, burrs become much more obvious.

This is why some factories notice edge problems only after increasing production speed.

Machine Structure Directly Affects Edge Quality

In single knife systems, the upper knife rotates while the lower knife stays fixed. The cutting process depends heavily on pressure and impact force.

For thin paper, this is usually acceptable. For thick board, the cutting process becomes less stable.

Double knife systems reduce this problem because both knife rollers rotate together. The material is cut from both sides simultaneously.

Double helical cross-cutting knife set

The cutting force stays more balanced. The paper deforms less. The edge quality becomes cleaner.

That is one reason why high-end packaging factories prefer double knife slitting machines for thick material production.

Burrs Are Not Caused by One Factor Alone

In actual factory production, burrs usually come from multiple small problems together.

Common causes include:

  • incorrect knife gap
  • worn knife edges
  • unstable tension
  • vibration at high speed
  • poor knife alignment
  • unsuitable machine structure

Operators sometimes keep adjusting knife pressure to solve the issue. But too much pressure can create more friction and shorten knife life.

The better solution is finding the real source of instability first.

Stable Production Depends on System Matching

SMH-SGT1400double rotary sheeter

Factories with stable thick paper production usually control several things carefully:

  • proper knife structure
  • stable web tension
  • synchronized feeding speed
  • correct knife clearance
  • rigid machine frame

When these conditions stay stable, burr problems reduce significantly.

The goal is not simply increasing pressure. The goal is maintaining stable cutting conditions throughout the entire run.

A4-4 vs A4-5 Production Line: Which Copy Paper Machine Is Better?

Choosing the right A4 paper production line is critical for paper converting factories. Production capacity, paper width, factory layout, and automation requirements all influence machine selection.

The CHM A4-4 and A4-5 production lines are both designed for automatic A4 copy paper manufacturing, but they serve different production needs.

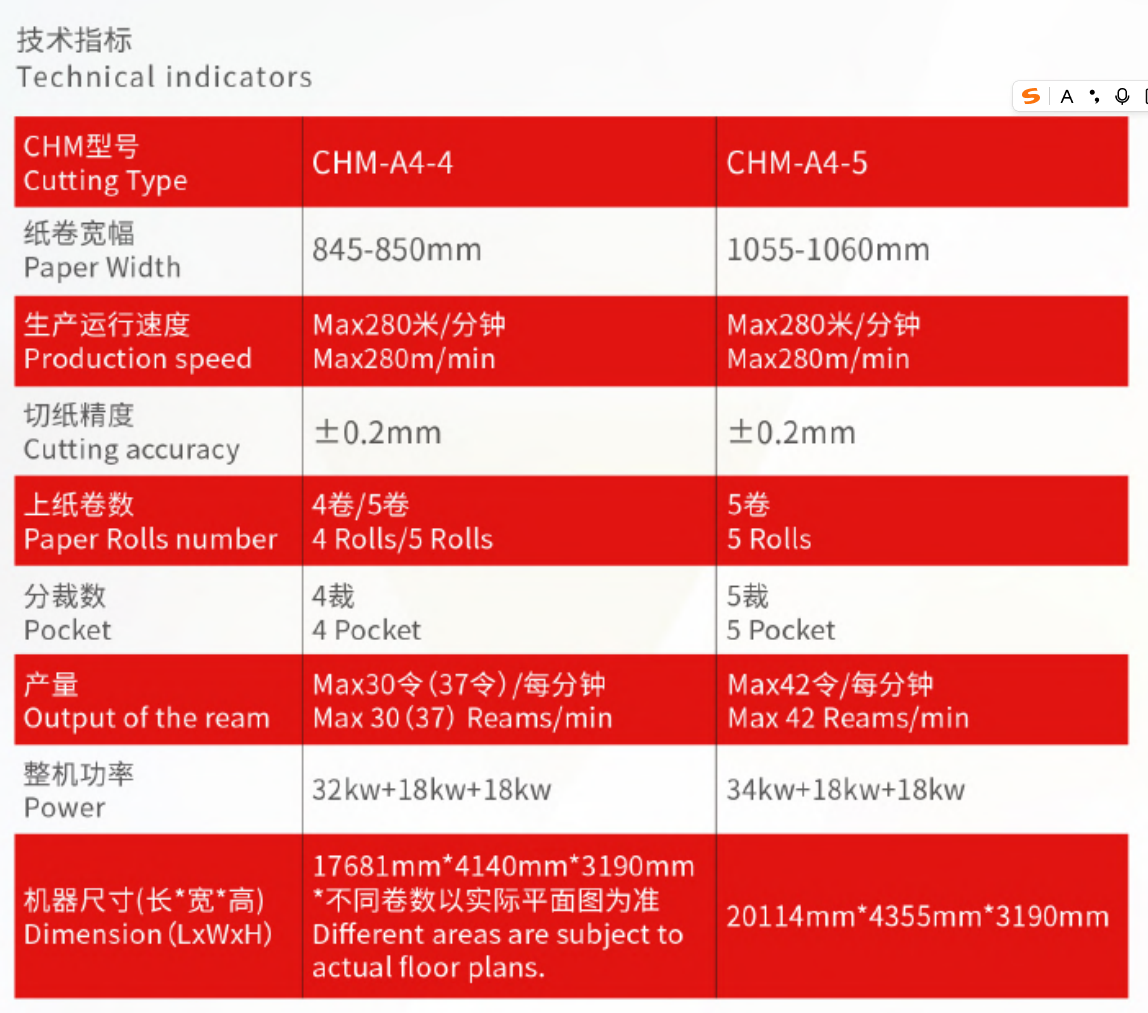
Main Difference Between A4-4 and A4-5

The biggest differences include:

  • Paper width
  • Cutting lanes
  • Production output
  • Machine dimensions
  • Power configuration

The A4-5 model supports wider paper rolls and higher production capacity.

Production Capacity Comparison

CHM A4-4

  • Output: 30–37 reams per minute
  • Main power: 32 kW
  • Suitable for medium-volume production

CHM A4-5

  • Output: 42 reams per minute
  • Main power: 34 kW
  • Suitable for high-volume production

For factories requiring maximum productivity, A4-5 provides stronger capacity advantages.

Machine Size Comparison

A4-4 Dimensions

17681 × 4140 × 3190 mm

A4-5 Dimensions

20114 × 4355 × 3190 mm

Factories with limited workshop space may prefer the more compact A4-4 model.

Automation Configuration

Both models support:

  • Automatic unwinding
  • Web guiding
  • Slitting
  • Cross cutting
  • Automatic stacking
  • Ream wrapping
  • Carton packing
  • Robotic palletizing

The fully automatic closed-loop system reduces manual operation and improves production stability.

Which Machine Should You Choose?

Choose A4-4 If:

  • You have limited factory space
  • You run medium production volumes
  • You require stable and flexible production
  • You have lower initial investment requirements

Choose A4-5 If:

  • You need maximum production output
  • You process wider paper rolls
  • You focus on large-scale copy paper manufacturing
  • You require high-speed continuous operation

Conclusion

Both A4-4 and A4-5 production lines provide advanced automation and high cutting precision. The final choice depends on production goals, factory conditions, and expected output.

For high-capacity factories, A4-5 delivers stronger productivity. For balanced production and flexible operation, A4-4 remains an excellent solution.