Tag SMH A4 Paper Cutting and Packaging Machine

Why Some Factories Enjoy Much Lower Waste Rates

Why Some Factories Enjoy Much Lower Waste Rates

In paper converting, some waste – trim loss or startup scrap – is expected. But when waste rates stay consistently high, the issue usually isn’t the material or even the machine. It’s how the process is controlled.

Interestingly, factories with the lowest waste rates aren’t always using the newest equipment. What sets them apart is how consistently they run their process.
Waste Is Often a Control Problem

The gap in waste rates rarely comes from a single factor. Instead, it’s from small variations throughout production:

  • Inconsistent setup between shifts
  • Frequent parameter changes without clear standards
  • Lack of repeatability between similar orders

Each variation may seem minor, but together they lead to higher reject rates, off-spec sheets, and increased material loss.

Three Habits of Low-Waste Operations

1. Strict Process Control
Once a set of conditions works for a specific paper grade, document it and follow it consistently. Changes are only made when necessary, based on clear reasons. This reduces trial‑and‑error and keeps results predictable.

2. Consistent Parameter Management
Treat parameter settings as production assets. Save job‑specific recipes, reuse proven settings, and record adjustments for future reference. This shortens setup time and reduces the risk of errors that cause waste.

3. Standardized Operator Practices
Operator behavior directly affects waste. In low‑waste plants, procedures are clearly defined, each step follows a standard method, and results depend less on individual experience. This ensures consistency across shifts.

Why Equipment Alone Does Not Solve the Problem

Upgrading machines can improve performance, but it doesn’t automatically reduce waste. If the process remains inconsistent, new equipment will face the same issues: unstable operation, repeated adjustments, inconsistent output. Waste reduction requires both capable equipment and disciplined process control.

Practical Impact on Production

When these habits are applied:

  • Startup waste is reduced
  • Fewer sheets are rejected during production
  • Output becomes more stable
  • Material utilization improves over time

Even small improvements in waste rate have a measurable impact on total production cost.

Conclusion

Lower waste isn’t the result of working harder or running faster. It comes from running the same process the same way, every time.

Factories that control parameters, standardize operations, and reduce unnecessary variation achieve consistently lower waste rates – regardless of equipment level.

Want to lower your waste rate?
If your waste levels are higher than they should be, SMH can help you assess your process control, parameter management, and operator practices.

Contact SMH – get a practical waste reduction plan based on real production habits, not just new hardware.
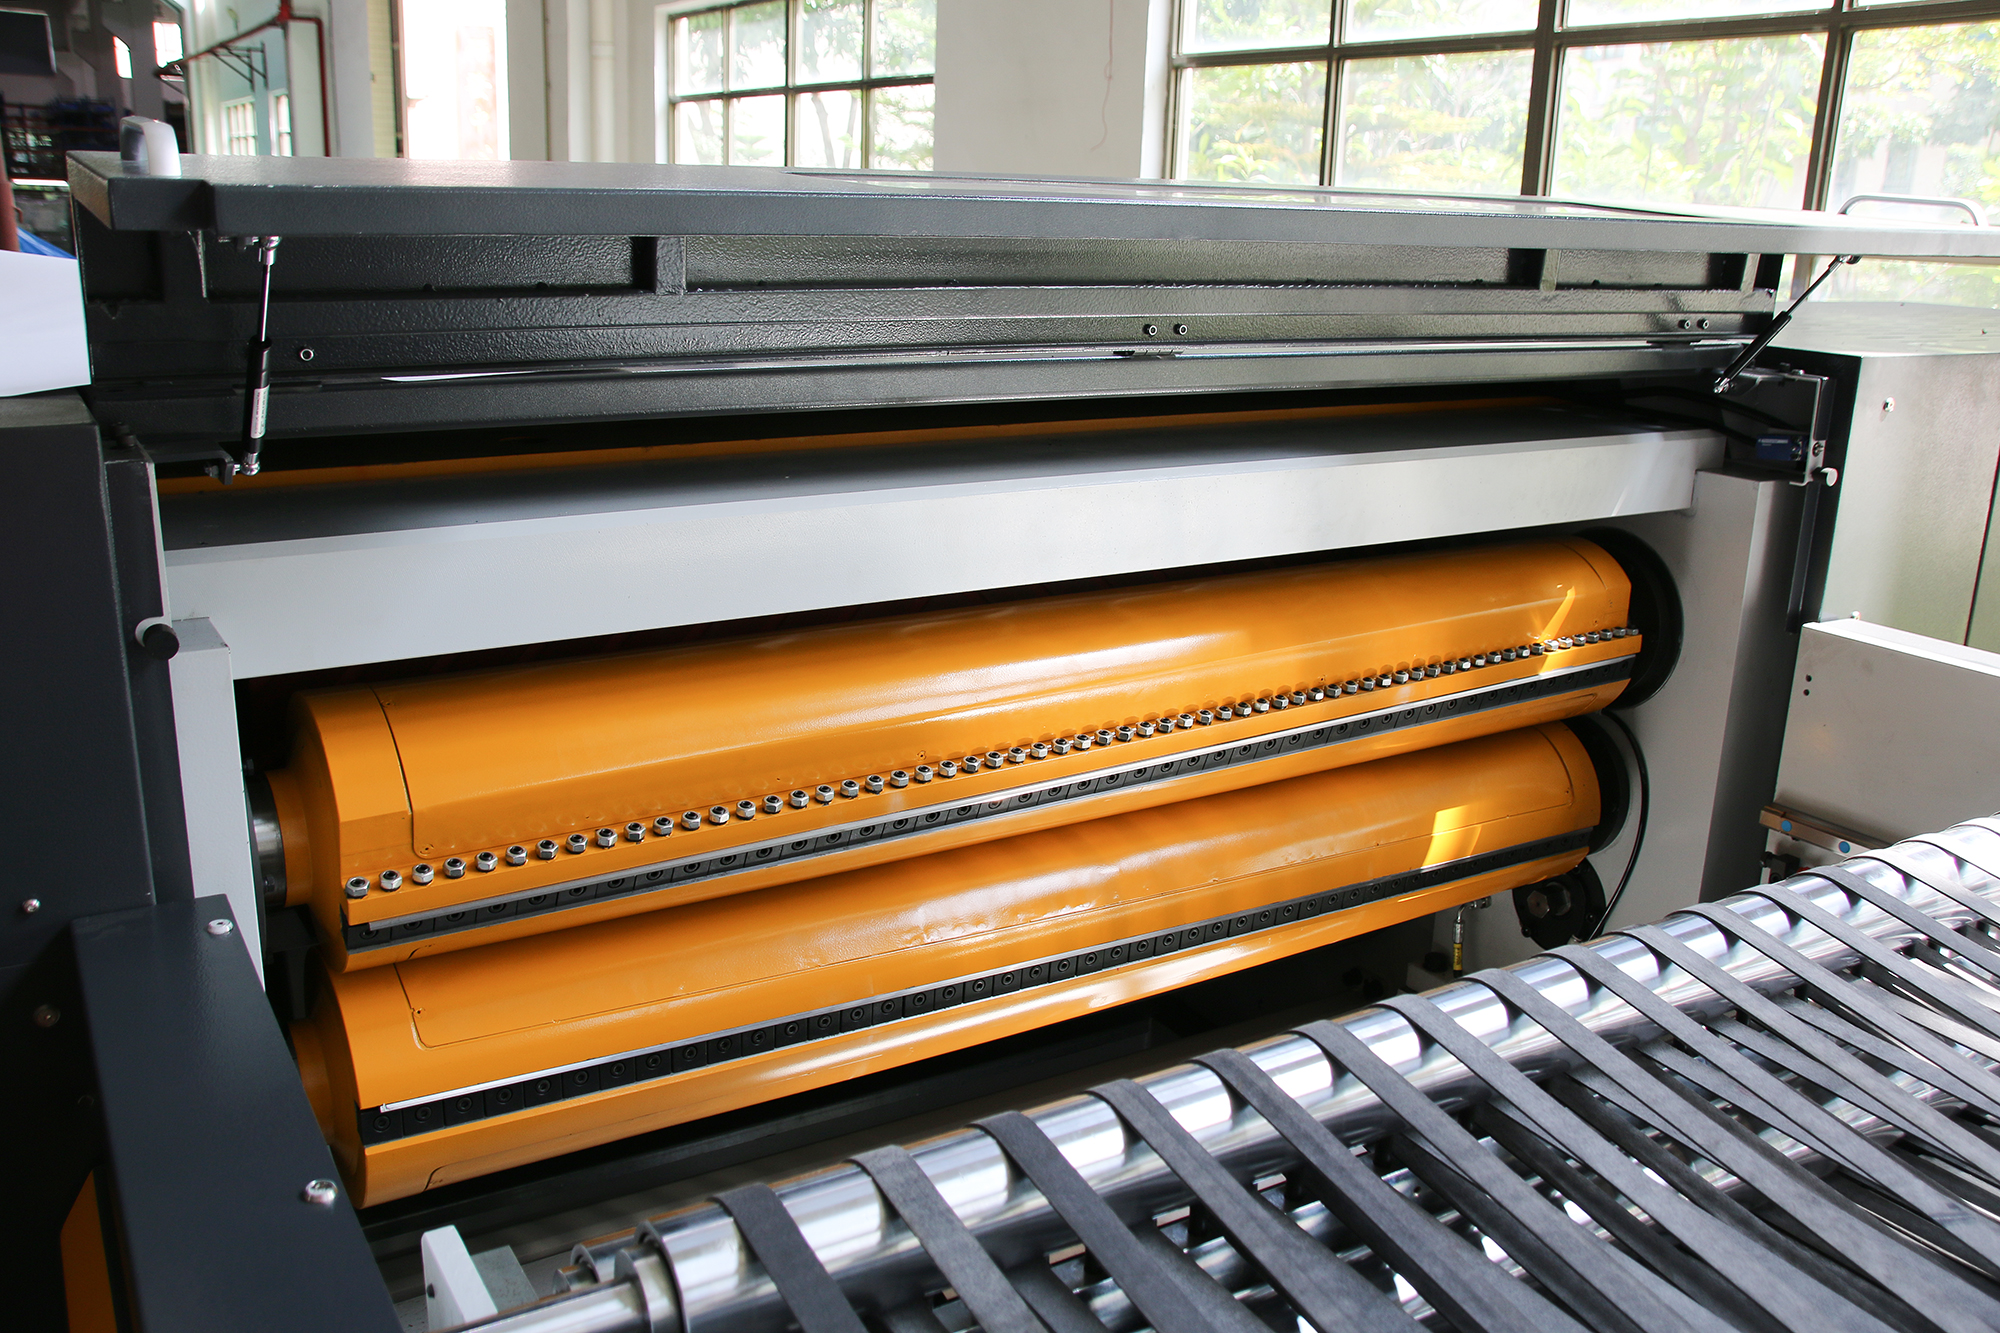
How Roller Condition Impacts Paper Quality Secretly

Rollers are one of the most underestimated components in a sheeting line.
Attention is usually placed on cutting units, motors, and control systems, while rollers are expected to “just work.”

In reality, rollers directly affect how paper moves through the machine.
When their condition is not stable, problems appear gradually—often without being immediately traced back to the rollers themselves.

Why Rollers Matter More Than Expected

Every stage of the process depends on controlled paper movement.
Rollers are responsible for:

  • feeding the paper forward
  • maintaining traction
  • supporting stable tension
  • guiding the web through different sections

If any of these functions become inconsistent, the impact will show up in product quality.

Common Roller-Related Issues

1. Surface Wear
Over time, roller surfaces lose their original friction characteristics.

When grip decreases:

  • paper may slip slightly during transport
  • feed accuracy becomes inconsistent
  • sheet length may begin to vary

This issue often develops slowly, making it difficult to detect early.

2. Contamination Build-Up
Dust, paper fibers, coating residue, or adhesive can accumulate on roller surfaces.

This leads to:

  • uneven contact across the roller width
  • inconsistent feeding force
  • localized slipping or drag

In some cases, contamination creates small but repeated disturbances in paper movement.

3. Misalignment
Even a slight deviation in roller alignment can affect web behavior.

If rollers are not parallel:

  • the paper may drift to one side
  • tension becomes uneven across the width
  • edge quality and cutting position are affected

These problems are often mistaken for guiding or tension issues, while the root cause lies in mechanical alignment.

Why These Problems Are Often Overlooked

Roller-related issues rarely cause immediate failure.
Instead, they introduce small variations into the process.

Operators may respond by adjusting tension, guiding, or speed, without realizing that the underlying problem remains.
This leads to repeated corrections without long-term improvement.

Impact on Final Product Quality

When roller condition is not consistent:

  • sheet length accuracy becomes unstable
  • wrinkles or waviness may appear
  • edge alignment can drift
  • stacking quality may decline

These effects are cumulative and become more visible during long production runs.

Maintaining Stable Roller Performance

To avoid these issues, roller condition should be part of routine maintenance rather than occasional inspection.

Key practices include:

  • regular cleaning to remove dust and residue
  • checking surface wear and replacing when necessary
  • verifying alignment across the full width
  • monitoring feeding consistency during operation

Consistent maintenance helps prevent gradual quality loss.

Conclusion

Rollers may seem like simple mechanical parts, but they play a critical role in process stability.
Small issues—wear, contamination, or misalignment—can lead to noticeable quality problems over time.

Maintaining roller condition is not just maintenance work; it is a necessary step to ensure stable feeding, consistent tension, and reliable cutting results.

Why Your Line Looks Busy but Output Is Low | Practical Analysis

It’s common to see a production line running all day with operators constantly moving, adjusting, and handling materials.
On the surface, everything looks active. But when you check the actual output, the numbers don’t match the effort.

This gap between activity and real productivity is a frequent issue in paper converting plants.

Pallet truck for transporting roll paper

Activity Does Not Equal Output

A line can be “busy” for many reasons that don’t contribute to finished product.
Operators may be:

  • moving stacks between sections
  • correcting alignment issues
  • waiting for the next step to catch up
  • handling small interruptions

All of this creates motion, but not necessarily usable output.

Where Efficiency Is Actually Lost

Based on practical production observations, low output in a busy line usually comes from three areas.

1. Excessive Manual Handling
When too many steps depend on manual work, speed becomes limited by people rather than machines.

Typical examples include:

  • manual counting and sorting
  • repositioning stacks
  • repeated adjustments between processes

Even if each step only takes a short time, the cumulative effect reduces overall throughput.

2. Unbalanced Workflow Layout
Layout design directly affects how materials move through the factory.

If the process is not well arranged:

  • raw materials travel longer distances than necessary
  • semi-finished products are temporarily stored and moved again
  • finished goods require additional handling before shipment

These extra movements do not add value but consume time and labor.

3. Frequent Small Interruptions
Short stops are often overlooked because they seem minor.

In reality, they are one of the biggest sources of lost efficiency.
These include:

  • minor jams
  • repeated parameter adjustments
  • sample checks and corrections
  • coordination delays between sections

Individually, each stop may last only a few minutes. Over a full shift, they significantly reduce effective production time.

Why the Problem Persists

Many operations try to solve these issues by adding more operators or increasing machine speed.
In most cases, this does not improve output.

If the process itself is not smooth, increasing speed only creates more instability, and adding labor increases complexity without fixing the root cause.

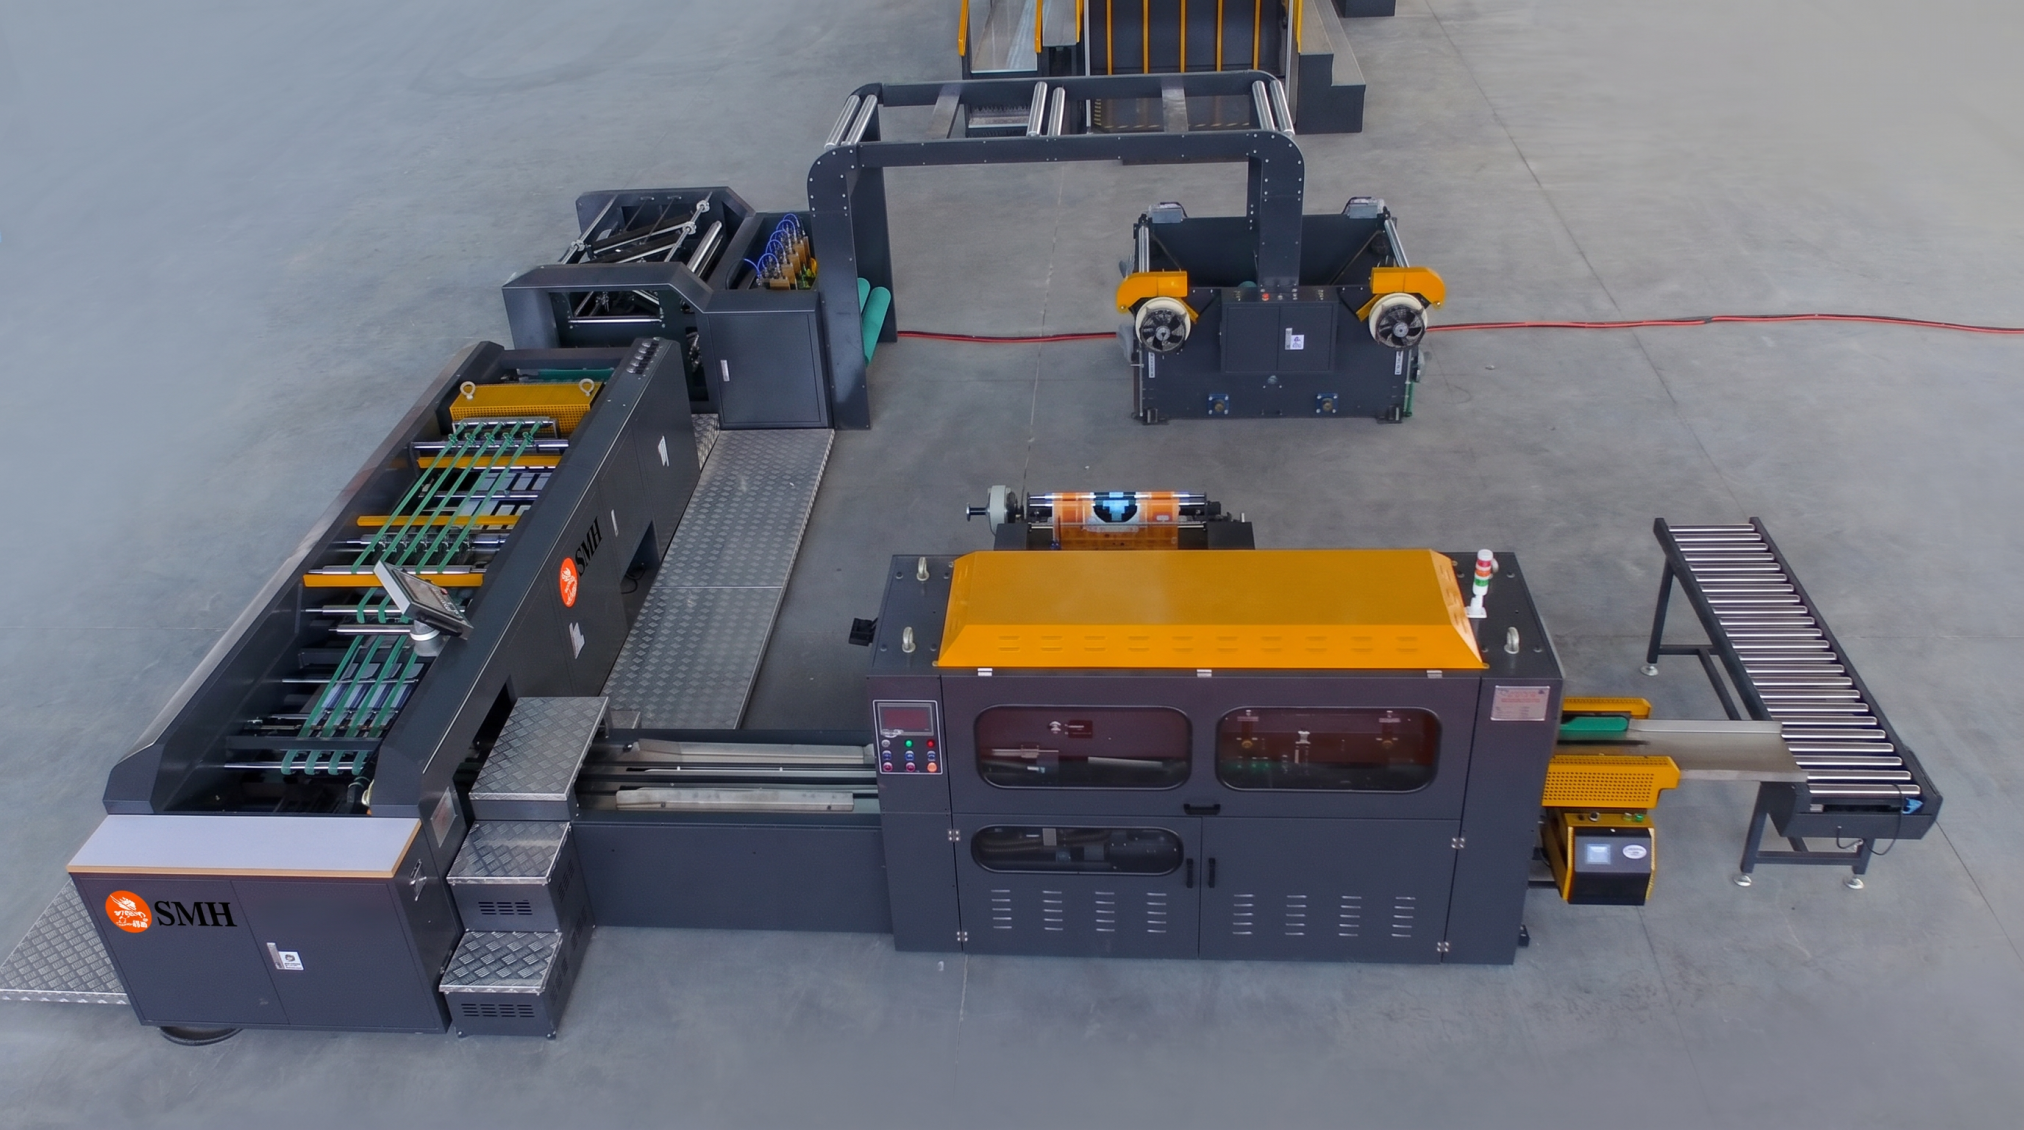
SMH A4 Paper Cutting and Packaging Machine

What an Efficient Line Looks Like

A high-efficiency line is not defined by how busy it appears, but by how smoothly it runs.

In a well-structured process:

  • material flows continuously from one step to the next
  • each section is matched in capacity
  • manual intervention is minimized
  • interruptions are rare and controlled

The result is steady, predictable output rather than fluctuating performance.

Practical Outcome

When workflow and process balance are improved:

  • total output increases without raising nominal speed
  • operator workload becomes more manageable
  • product quality becomes more consistent
  • planning and delivery become more reliable

Efficiency comes from reducing unnecessary actions, not increasing activity.

Conclusion

A busy production line is not always a productive one.
If output remains low despite constant activity, the issue lies in process design, not effort.

Real efficiency is achieved when the entire line operates as a coordinated system, where each step supports continuous flow rather than interrupting it.

How Paper Grade Affects Cutting Performance | Practical Guide

Not all paper behaves the same in a sheeter.
Running different grades with one fixed setup is one of the most common reasons for defects, unstable operation, and unnecessary downtime.

In real production, cutting performance is closely tied to the physical properties of the paper—weight, stiffness, surface structure, and moisture behavior all play a role. Ignoring these differences leads to inconsistent results.

Why Paper Grade Matters

Each paper grade responds differently to tension, cutting force, and transport conditions.

A setup that works well for one material may cause problems for another.
This is why parameter adjustment is not optional—it is necessary for stable production.

Typical Behavior by Paper Type

1. Lightweight Paper (28–80 gsm)
Thin paper is flexible and highly sensitive to tension changes.

Common issues include:

  • wrinkling during transport
  • web instability at higher speeds
  • risk of web breaks under excessive tension

To run lightweight grades properly, the system must operate under low, stable tension, with smooth conveying and minimal disturbance.

2. Heavy Board and High GSM Paper
Thicker materials behave very differently.

They require:

  • higher and more stable cutting force
  • rigid mechanical support during cutting
  • precise synchronization to avoid deformation

If the cutting force is insufficient or unstable, problems such as rough edges or incomplete cuts can occur.

3. Coated Paper
Coated surfaces introduce another layer of complexity.

While structurally stable, they are more sensitive to surface damage.

Typical risks include:

  • scratching during transport
  • coating cracks at the cut edge
  • visi