The Complete Guide to Paper: From Raw Materials to Applications

Have you ever wondered how the paper you use every day is made? What’s the difference between various types of paper? This article will take you through the ins and outs of paper.

1. What Paper Is Made Of: Fibers and Additives Working Together

Main raw materials (plant fibers):

  • Wood, reeds, bamboo
  • Sugarcane bagasse, rice straw, wheat straw
  • Tree bark, cotton, hemp, etc.

Additives:

  • Fillers (e.g., clay, talc): fill gaps between fibers
  • Sizing agents: improve strength and smoothness
  • Dyes: for tinting or coloring – even white paper needs treatment

2. Specialty Papers: Types and Structure of Gold/Silver Cardboard
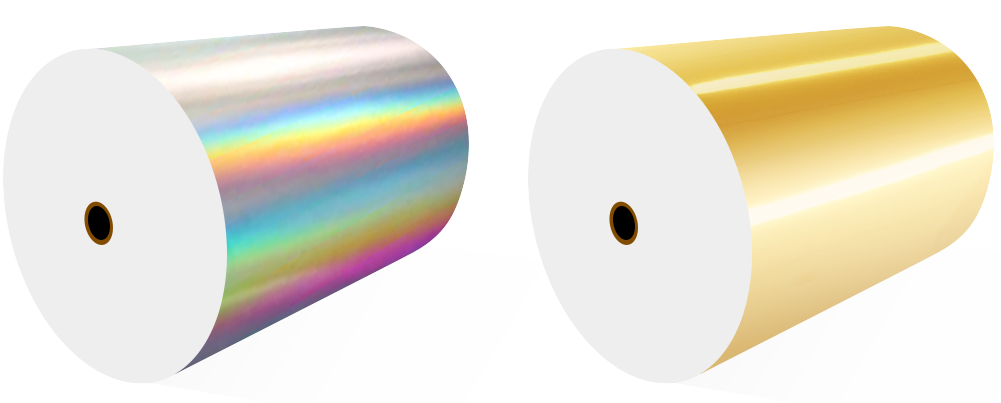
Gold/Silver Cardboard

TypeComposition
Aluminum foil basedAluminum + backing paper + varnish + print
PET basedFilm + backing paper + varnish + print
HolographicFilm + aluminum + embossing + backing paper + varnish + print

Note: Gold card is made by dyeing silver card (coated with red or yellow pigment), so its adhesion is generally weaker than that of silver card.

3. Paper Quality Evaluation Criteria

Visual quality

  • Uniformity: even distribution of fibers and thickness
  • Cleanliness: surface free from dirt and spots
  • Flatness: smooth and even

Physical properties

  • Squareness, caliper, density
  • Opacity, dirt count
  • Tensile strength, folding endurance, tear resistance

4. Paper Sizes Explained

Packaging formats

  • Sheet-fed: pre-cut by the mill, good flatness
  • Roll: wound on a core
Roll/Sheet-fed

Common sizes

TypeDimensions (mm)Inches
Large format889 × 119435″ × 47″
Standard format787 × 109231″ × 43″
Special formatAny size other than abovee.g., 25″ × 38″

5. Thickness vs. Grammage Reference Tables

Note: 1 “si” (Chinese unit) = 0.01 mm. Values vary by manufacturer and process; for reference only.

Coated paper (art paper)

GrammageThickness (si)
80 gsm5–6
105 gsm7–8
128 gsm10–11
157 gsm12–13
200 gsm16–17
230 gsm19
250 gsm22

Coated board

GrammageThickness (si)
230 gsm22–26
250 gsm26–27
300 gsm30–31
350 gsm35–37

Matte coated paper is about 2 si thicker than gloss coated paper of the same weight.

White card (solid bleached board)

GrammageThickness (si)
230 gsm29–30
250 gsm35
300 gsm40
350 gsm47–48
400 gsm52

White-backed white board / gray board

GrammageThickness (si)
250 gsm white back28
450 gsm white back57
250 gsm gray back28
300 gsm gray back36
350 gsm gray back42
400 gsm gray back49
450 gsm gray back57

Woodfree offset paper

GrammageThickness (si)
70 gsm8
80 gsm9
100 gsm11
120 gsm13
140 gsm16

Kraft paper

GrammageThickness (si)Notes
80 gsm11
120 gsm14
150 gsm16–1818 typical, 16 special
200 gsm22
300 gsm44

6. Practical Conversions and Selection Tips

How to choose:

  1. Brochures: 157–250 gsm coated paper
  2. Business cards: 300–350 gsm coated board or white card – specialty paper for a premium feel
  3. Book interiors: 70–120 gsm woodfree offset paper
  4. Packaging boxes: 250–400 gsm gray board or white card
  5. Envelopes/file folders: 80–150 gsm kraft paper

Thickness reference (everyday items):

  • Standard A4 printer paper: about 8–9 si
  • Typical business card: 30–35 si
  • Hardcover book cover: 40–50 si
  • High-end gift box: over 50 si

With this guide, you now have a solid understanding of paper raw materials, types, specifications, and quality standards. Whether for daily use or professional selection, this knowledge will help you make better decisions.
How Tension Directly Shapes Final Paper Quality

Tension is often treated as just another parameter on the control panel.
In reality, it is one of the most influential factors in the entire sheeting process.

From unwinding to cutting and conveying, tension determines how the paper behaves at every stage.
If it is not properly controlled, quality problems will appear—even when the machine itself is running normally.

Why Tension Matters More Than It Seems

Paper is not a rigid material.
It reacts continuously to force, especially at high speed.

When tension changes, even slightly, the paper structure responds immediately.
These changes may not always be visible during operation, but they become clear in the finished sheets.

Three Direct Impacts on Final Quality

1. Flatness
Flat sheets require balanced tension across the entire web.

If one side is tighter than the other, internal stress builds up.
After cutting, this stress is released, leading to:

  • edge curl
  • waviness
  • uneven stacking

In many cases, what looks like a material problem is actually caused by uneven tension distribution.

2. Dimensional Stability
Sheet length and width depend on consistent material behavior during transport.

If tension fluctuates:

  • the paper may stretch or relax inconsistently
  • cut length may drift over time
  • size variation can appear between batches

This is especially noticeable during long production runs, where small deviations accumulate.

3. Cutting Accuracy
Accurate cutting requires the paper to be stable at the moment of shearing.

If tension is unstable:

  • the sheet may shift slightly during cutting
  • edges may become uneven
  • alignment between sheets may vary

Even with a precise cutting system, unstable tension can reduce overall accuracy.

Why Tension Becomes Unstable

In practical production, tension issues often come from:

  • changes in roll diameter during unwinding
  • inconsistent brake or drive response
  • improper parameter settings for different paper grades
  • lack of coordination between line sections

Without proper control, tension tends to drift rather than remain constant.

What Stable Tension Control Looks Like

A stable system does not rely on fixed values alone.
It adjusts continuously based on real conditions.

In a well-controlled line:

  • tension remains consistent from the start of the roll to the end
  • changes in roll diameter are automatically compensated
  • different paper grades can run with appropriate force levels

This reduces the need for manual correction and improves repeatability.

Practical Result in Production

When tension is properly controlled:

  • sheets remain flat after cutting
  • dimensions stay consistent across long runs
  • cutting quality becomes more reliable
  • stacking and downstream handling improve

Just as importantly, operators spend less time making adjustments.

Conclusion

Tension is not just a setup parameter—it is a continuous control factor that directly shapes product quality.

If tension is unstable, defects will appear regardless of machine speed or cutting precision.
If tension is stable, the entire process becomes more predictable, and quality follows naturally.

How Paper Grade Affects Cutting Performance | Practical Guide

Not all paper behaves the same in a sheeter.
Running different grades with one fixed setup is one of the most common reasons for defects, unstable operation, and unnecessary downtime.

In real production, cutting performance is closely tied to the physical properties of the paper—weight, stiffness, surface structure, and moisture behavior all play a role. Ignoring these differences leads to inconsistent results.

Why Paper Grade Matters

Each paper grade responds differently to tension, cutting force, and transport conditions.

A setup that works well for one material may cause problems for another.
This is why parameter adjustment is not optional—it is necessary for stable production.

Typical Behavior by Paper Type

1. Lightweight Paper (28–80 gsm)
Thin paper is flexible and highly sensitive to tension changes.

Common issues include:

  • wrinkling during transport
  • web instability at higher speeds
  • risk of web breaks under excessive tension

To run lightweight grades properly, the system must operate under low, stable tension, with smooth conveying and minimal disturbance.

2. Heavy Board and High GSM Paper
Thicker materials behave very differently.

They require:

  • higher and more stable cutting force
  • rigid mechanical support during cutting
  • precise synchronization to avoid deformation

If the cutting force is insufficient or unstable, problems such as rough edges or incomplete cuts can occur.

3. Coated Paper
Coated surfaces introduce another layer of complexity.

While structurally stable, they are more sensitive to surface damage.

Typical risks include:

  • scratching during transport
  • coating cracks at the cut edge
  • visi

Why Your Sheeter Never Reaches Rated Speed | SMH Solution

workshops, most sheeters are labeled with impressive top speeds, but very few actually run at those levels day in and day out. The problem is almost never the main machine itself—it’s the small, unbalanced details holding the whole line back.

From our years of on-site experience with hundreds of paper mills, we’ve narrowed it down to three most common bottlenecks:

  1. Tension instability: When tension jumps up and down, operators have no choice but to lower speed to stop paper from wrinkling, stretching, or even breaking.
  1. Edge guiding delay: At high running speeds, even tiny deviations in edge position become obvious quickly, forcing the line to slow down for correction.
  2. Transport mismatch: If the conveyor, stacking, or downstream packing can’t keep up with the cutter, the whole line has to throttle back to avoid jams.

Running at full rated speed isn’t about forcing the machine harder. It’s about system balance. SMH designs sheeters with stable tension control, precise edge guiding, and fully synchronized conveying and stacking systems, so your production line can hold rated speed steadily for long runs.